
Double Plus Chain Working Principle Explained
Practical engineering guide: Double Plus Chain Working Principle Explained. Selection, interfaces, application checks, maintenance and RFQ inputs.
This guide focuses on how the small and large roller arrangement creates free-flow carrier motion and a speed relationship between chain and pallet. It is written for machine builders, maintenance teams and buyers who need a chain selection that can be checked against drawings and the real conveyor rather than a generic product label.
Double Plus Chain Working Principle Explained
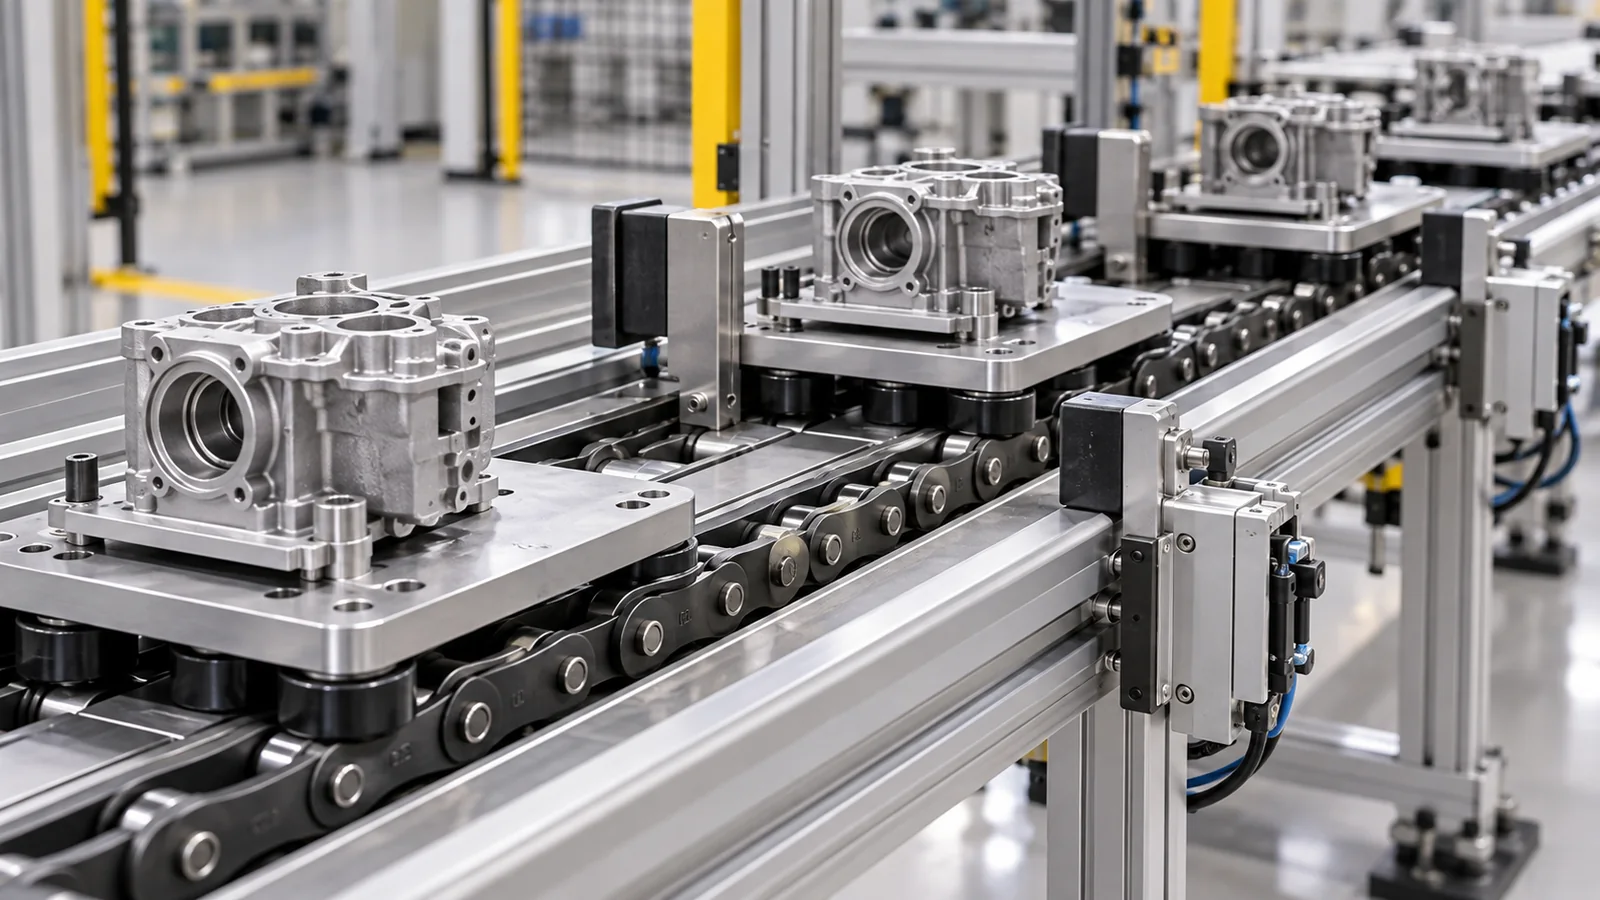
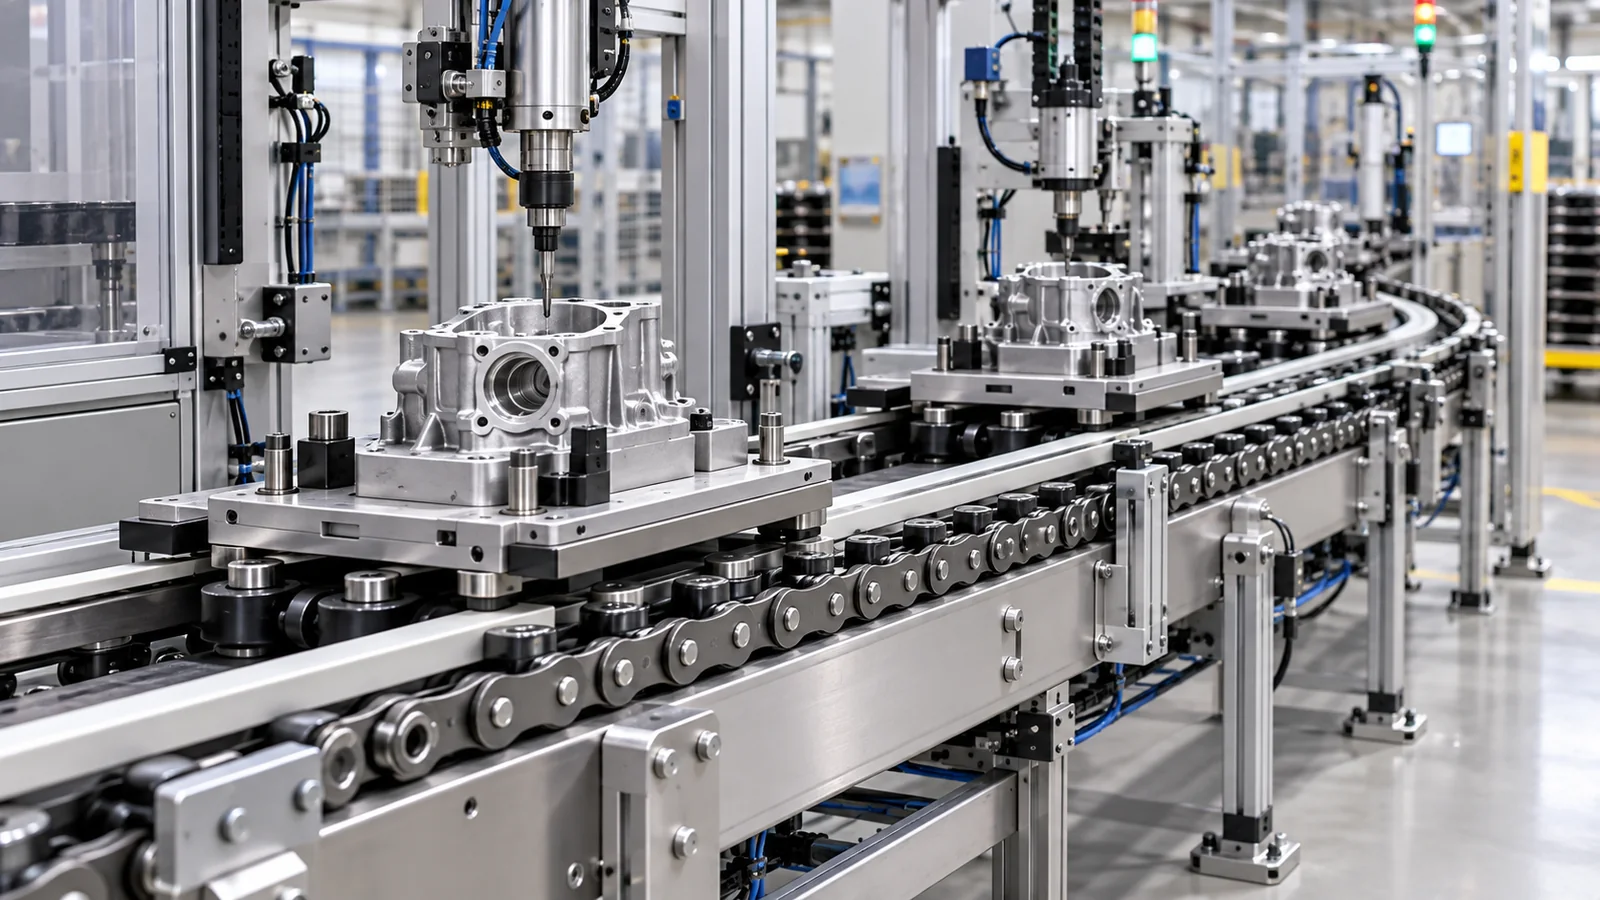
The most useful way to evaluate this subject is to treat the chain as one part of a complete carrier-transport mechanism. In a typical project such as a workpiece pallet moving between assembly stations, chain pitch, roller contact, rail alignment, sprocket engagement, carrier stiffness, stops and maintenance access all influence the result. A useful engineering review therefore combines model-level data with the operating sequence of the machine.
Неліктен бұл мәселе маңызды
How the small and large roller arrangement creates free-flow carrier motion and a speed relationship between chain and pallet affects more than catalogue selection. It changes how the workpiece carrier enters a station, how loads pass into guide rails, how the chain approaches the drive and how the system behaves during stopping or accumulation. If one interface is ignored, the symptom may appear somewhere else: a roller can wear because a rail joint is high, a chain can pull sideways because a pallet stop is offset, or a new chain can run badly because the old sprocket is worn.
The practical objective is not to eliminate every variation in the machine. It is to identify the variables that must be controlled, define which dimensions are fixed by the chain source, and leave unsupported items for explicit RFQ confirmation. This is also why treating the 2.5x or 3.0x ratio as a motor-speed setting is a risky shortcut. It replaces measurable machine data with an assumption and can make a correct-looking part fail at installation.
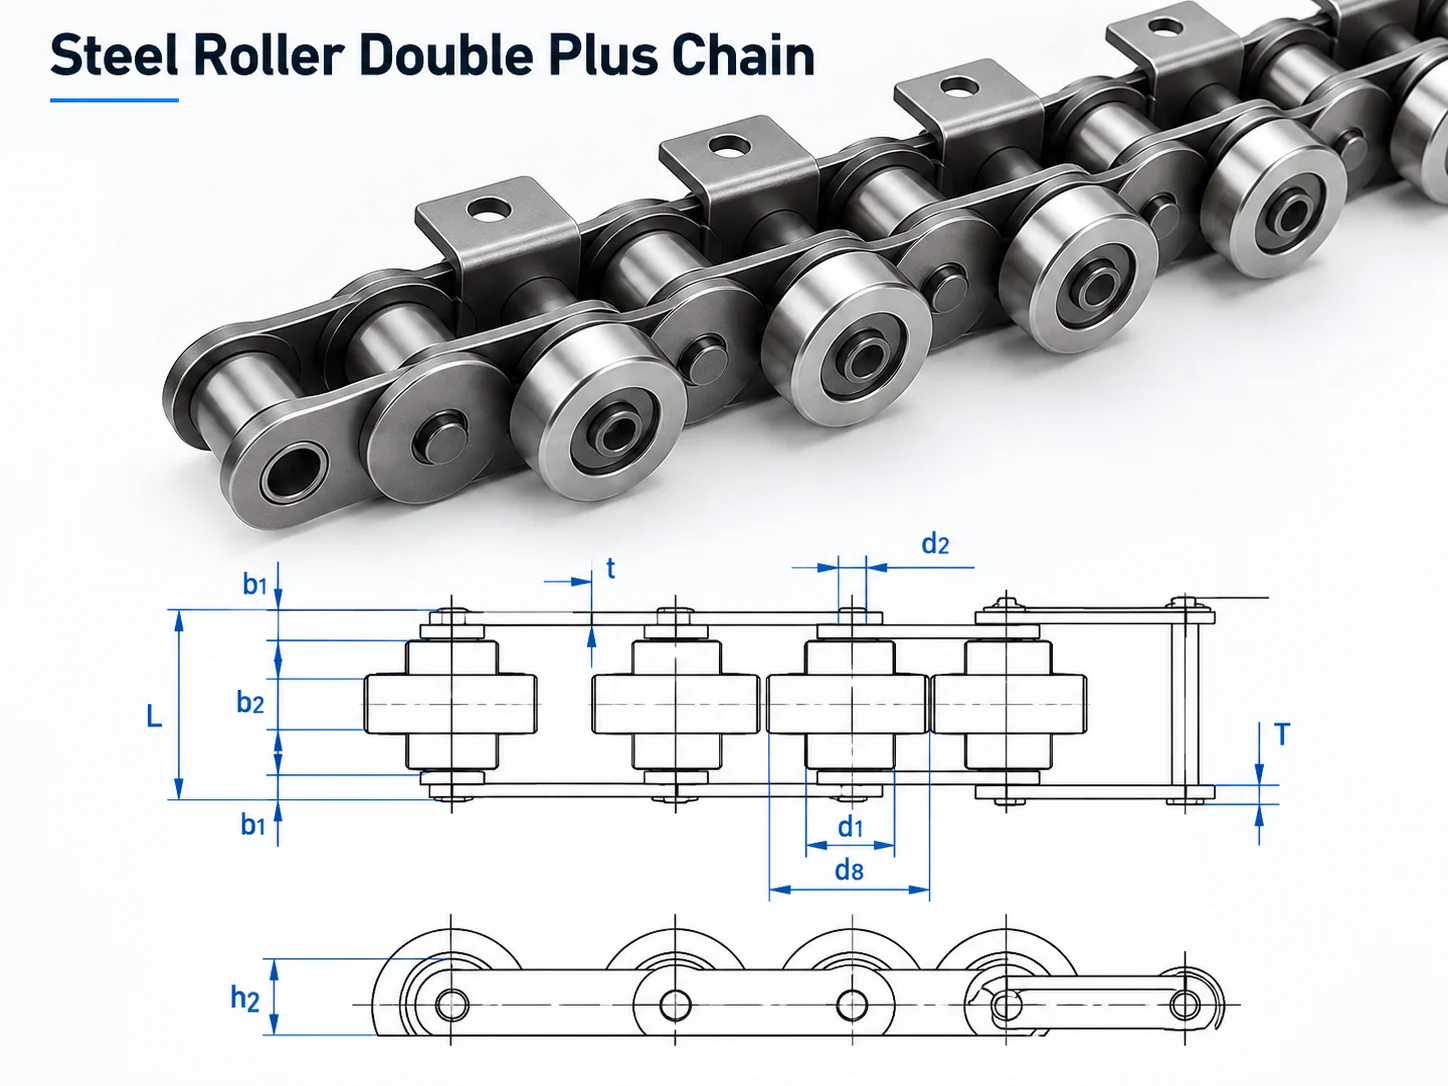
In the approved catalogue used for this project, the Double Plus family is presented in 2.5-times and 3-times speed groups. That description supports the speed-ratio concept, but it does not remove the need to check the model-specific data row. A BS25 and BS30 chain can share a nominal pitch while having different roller geometry, so the complete row and drawing remain the authority for replacement work.
Алдымен анықтау үшін төрт тексеру
Small/Large Roller Contact
Record the relevant diameter, offset, contact surface, clearance and visible wear so the running interface can be checked.
Rail Support
Record the relevant diameter, offset, contact surface, clearance and visible wear so the running interface can be checked.
Pallet Contact Surface
Тасымалдаушы интерфейсін тексеру үшін жүктелген жағдайды, жанасу немесе деректер бетін, орналасуын және күш жолын анықтаңыз.
Sprocket And Return Path
Record tooth count or drive geometry, shaft alignment, take-up position and the way the chain enters and leaves the drive.
Тізбектің дәл геометриясынан бастаңыз
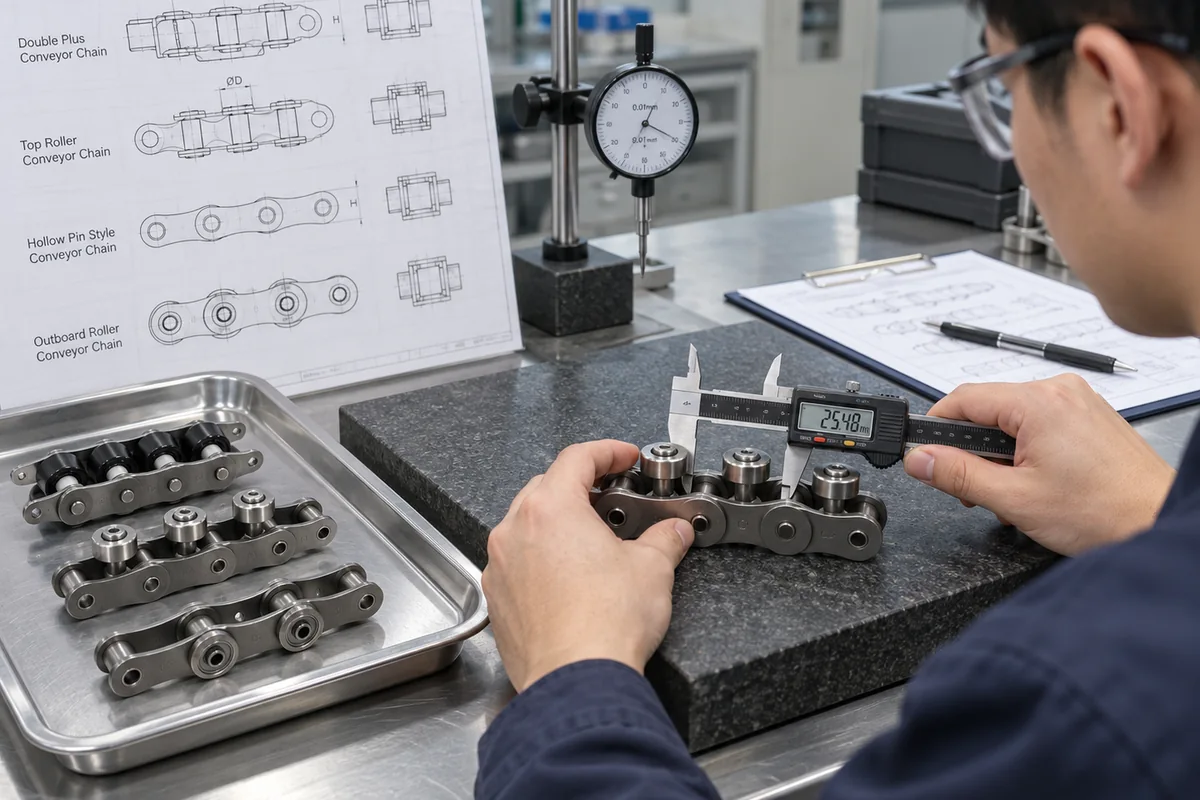
Модель нөмірі қолжетімді болған кезде, дәл модель сипаттамасын және сәйкес сызбаны пайдаланыңыз. Қадамды, ролик диаметрлерін, ішкі енін, түйреуіштің диаметрі мен ұзындығын, пластинаның биіктігі мен қалыңдығын және конвейермен байланысатын кез келген бүйірлік роликтің, үлкен роликтің немесе қуыс түйреуіштің өлшемдерін салыстырыңыз. Код белгісіз болған кезде, орнатылған тізбекті жүйелі түрде өлшеңіз. Бірнеше түйреуіштердегі қадамды өлшеу бір тозған саңылауды оқудан гөрі сенімдірек, ал фотосуреттерде бүйірлік профиль, роликтің орналасуы, жұлдызша және рельстің жанасуы көрсетілуі керек.
Созылу беріктігін паллеттің пайдалы жүктемесі ретінде пайдаланбаңыз. Каталогтың созылу көрсеткіштері материал/компонент сынақ қасиеттері болып табылады. Конвейердің жұмыс жағдайларына сонымен қатар желі ұзындығы, тізбек жіптерінің саны, тасымалдаушылар саны, үдеу, соққы, үйкеліс, майлау, жұлдызша өлшемі, тозу күйі және қажетті қауіпсіздік коэффициенті кіреді. Тізбекті жүйе үшін тек осы шарттар түсінілгеннен кейін ғана тексеруге болады.
Таңдау жұмысының барысы
- Small/Large Roller Contact: Қажетті шартты нақты тізбек сызбасымен немесе жүйенің орналасуымен салыстырыңыз және кез келген ашық сұрақты RFQ растауы үшін жазып алыңыз.
- Rail Support: Қажетті шартты нақты тізбек сызбасымен немесе жүйенің орналасуымен салыстырыңыз және кез келген ашық сұрақты RFQ растауы үшін жазып алыңыз.
- Pallet Contact Surface: Қажетті шартты нақты тізбек сызбасымен немесе жүйенің орналасуымен салыстырыңыз және кез келген ашық сұрақты RFQ растауы үшін жазып алыңыз.
- Sprocket And Return Path: Қажетті шартты нақты тізбек сызбасымен немесе жүйенің орналасуымен салыстырыңыз және кез келген ашық сұрақты RFQ растауы үшін жазып алыңыз.
- Тасымалдаушы және міндет: жүктелген тасымалдаушы массасын, тасымалдаушылар санын, желі жылдамдығын, сағатына іске қосылуын, жинақталу үлгісін және кез келген көлбеу немесе тік ауысуды жазып алыңыз.
- Көлік жүргізу және қайтару: жұлдызша деректерін, біліктің туралануын, көтеру қашықтығын, қайтару тірегін және майлауға қол жеткізуді растаңыз.
- Шығару шарты: Техникалық деректерде көрсетілмеген кез келген өрісті – мысалы, арнайы материалдың сыныбы, жабын, рұқсат етілген жүйе жүктемесі немесе қоршаған орта рейтингісін – бағалаудың орнына, RFQ растау элементі ретінде тізімдеңіз.
Жүйелік интеграция
Тізбек анықталғаннан кейін, конвейердің жүктемені машинаның қалған бөлігіне қалай тасымалдайтынын тексеріңіз. Бағыттаушы немесе тозу рельсі роликтің белгіленген бетін ұстап тұруы және қосылыстар арқылы үздіксіз болуы керек. Параллель жіптердің көрсетілген орталық қашықтығы және синхрондалған жетек уақыты болуы керек. Тоқтатқыштар тізбектің бүйірлік тақтасына емес, жобаланған паллет бетіне тиюі керек. Көлденең берілістер мен көтергіштер тасымалдаушының саңылауға түсіп кетпеуі немесе түйреуіш/пластинаның шетіне түспеуі үшін жеткілікті тірек қажет.
Жиналатын жүйелер үшін тасымалдауды тоқтатудан бөлек ұстаңыз. Тасымалдаушы ұстап тұрғанда тізбек қозғалысын жалғастыруы мүмкін, бірақ тоқтату күшін, кезек ұзындығын, қайта іске қосу реттілігін және жергілікті үйкелісті әлі де тексеру қажет. Өңдеу үшін дайындаманы орналастыратын жүйелер үшін қажетті қайталанушылық қалыпты конвейерлік тасымалдау қамтамасыз ете алатыннан тығыз болған кезде арнайы орналастыру мүмкіндіктерін пайдаланыңыз.
Іске қосу және техникалық қызмет көрсету
Алдымен жаңа немесе жөнделген конвейерді төмен жылдамдықпен тапсырыс беріңіз. Бірнеше толық тізбекті тізбектерді айналдырып, жетек, қайтару, рельс ауысуларын, тоқтауларды және ауыстыруларды бақылаңыз. Тізбектің бір айналымында немесе жұлдызшаның бір айналымында бір рет қайталанатын дыбыстарды тыңдаңыз, себебі бұл үлгілер тығыз қосылысты, роликтің зақымдалуын, жергілікті рельс баспалдағының немесе жұлдызшаның мәселесін анықтауға көмектеседі. Қатты дайындама паллеттерімен параллель жіптердегі қиғаштықтарды бақылаңыз; тіпті шағын уақыт айырмашылықтары да тасымалдаушының бір жағын жүктей алады.
Техникалық қызмет көрсету ақаулықты күтудің орнына үрдістерді бақылауы керек. Бекітілген әдісті қолдана отырып, созылуды немесе ұзындықты тексеруді жазып алыңыз, роликтердің еркін айналуын және қалыптан тыс жазықтықтарын тексеріңіз, тураланбағанын көрсететін жылтыратылған бүйірлік жанасу белгілерін іздеңіз, жұлдызша тістерін тексеріңіз және тарту орнын тексеріңіз. Майлау аралықтары жұмыс ортасын және шынжыр өндірушісінің нұсқауларын көрсетуі керек; егер ол абразивті ластануды тартса немесе технологиялық аймаққа енсе, көбірек майлау автоматты түрде жақсы болмайды.
RFQ тексеру тізімі
Ауыстыру туралы сұраныс үшін, егер оқылатын болса, модель кодын, өлшенген қадамды, роликтің орналасуын, шынжырдың енін, пластинаның биіктігін, түйреуіштердің өлшемдерін, бүйірлік профильдің фотосуретін және жұлдызша/рельс байланысын көрсететін фотосуретті жіберіңіз. Жаңа жүйе үшін конвейер ұзындығын, тасымалдаушы өлшемін және жүктелген массаны, жіптер санын, жіп аралығын, жылдамдығын, іске қосылу/тоқтау, буфер ұзындығын, қоршаған орта жағдайларын және тағайындалған елді қосыңыз. Бұл мәліметтер шынжыр сәйкестігін конвейердің толық жұмыс есебінен бөлуге мүмкіндік береді.
Read the roller motion as a system
The useful feature of Double Plus chain comes from the interaction between the smaller rollers, larger carrier rollers and the guide rail. Carrier movement therefore depends on more than the base chain speed. Rail contact, roller condition, carrier weight, accumulation and the stop mechanism all change the way the conveyor behaves in service.
When checking an existing line, observe a carrier during free travel, accumulation and restart. Confirm that the intended roller surfaces rotate rather than slide, the stop restrains the carrier rather than the chain side plate, and the rail transition does not lift or shock the roller. These simple observations should accompany the dimensional model check.
Интерфейсті өлшеу
Егер ауыстыру құрылғысы бар жабдыққа сәйкес келуі керек болса, бірнеше көлбеу өлшемдерін, шеткі көрініс геометриясын және жұлдызша/рельс бөлшектерін пайдаланыңыз.
Міндетті сипаттаңыз
Жүктелген тасымалдаушының массасын, жылдамдығын, іске қосылуын, жинақталуын немесе индекстелуін және жұмыс ортасын қосыңыз.
Ең нашар жағдайды сынап көріңіз
Тек жүксіз жүрудің орнына, өкіл тасымалдаушылармен және ең талапшыл кезек, тоқтау, ауыстыру немесе қайта іске қосу шарттарымен комиссия.
Ашық элементтерді ашық ұстаңыз
Егер материал, жабын, арнайы төзімділік, құжаттама қажеттілігі немесе рұқсат етілген жүйе жүктемесі көрсетілмесе, оны сұрауда растаңыз.
Жиі қойылатын сұрақтар
Тек алаңнан ғана ауыстырушыны таңдай аламын ба?
For double plus chain working principle explained, pitch is only the first filter. Confirm roller geometry, inner width, pins, plates and any side-roller or hollow-pin features against the installed conveyor before treating two chains as interchangeable.
Созылу күші жоғары болса, бұл жүкті паллетке көтере аламын дегенді білдіре ме?
For double plus chain working principle explained, do not convert tensile strength directly into pallet payload. Service load depends on strand count, friction, acceleration, stop impact, sprockets, rails and the safety margin used for the machine.
Отбасылық фотосурет нақты үлгіні дәлелдей ала ма?
Жоқ. Отбасының бейнесі құрылымды түсіндіруге көмектесе алады, бірақ модельдің сәйкестігі мен өлшемдері модельге тән техникалық сипаттамадан, сызбадан немесе расталған өндірістік деректерден алынуы керек.
Қандай ақпарат баға ұсынысын жылдамдатады?
For an RFQ related to double plus chain working principle explained, send the model code or dimensional sketch, clear photographs, conveyor layout, loaded carrier information, quantity and delivery country so the review starts from reproducible machine data.
Key engineering variables for Double Plus Chain Working Principle Explained
Double Plus selection combines speed ratio, large/small roller interaction, guide rails and carrier underside contact. Record the operating case in one line: what the conveyor carries, how fast it moves, where it stops and what condition triggered the review. Capture dimensions and observations another engineer can reproduce.
| Кіріс | Нені жазу керек | Неліктен маңызды |
|---|---|---|
| Тасымалдаушы/жүк | Жүктелген масса, ауырлық центрі, төменгі жанасу және тасымалдаушылар саны | Қолдау, үйкеліс және тоқтату мінез-құлқы |
| Қозғалыс | Жылдамдық, іске қосу, тоқтату, жинақтау және индекстеу | Динамикалық сұраныс және процесс уақытын есептеу |
| Тізбек жолы | Қадам, роликтер, жіп аралығы және рельстер | Механикалық сәйкестендіру және бақылау |
| Көлік жүргізу | Тісжегі тістері, туралау, тарту және жетек орны | Қатысу және шиеленістің таралуы |
| Қоршаған орта | Температура, шаң, ылғал, тазалау және майлау шектеулері | Материалды таңдау және күтім |
Байланысты өнім және таңдау ресурстары
Қолданыңыз паллет конвейерінің тізбегінің каталогы отбасыларды салыстыру және инженерлік іріктеу жұмысының барысы машиналық деректер толық емес болған кезде.
What to include with an enquiry about Double Plus Chain Working Principle Explained
Орнатылған немесе ұсынылған тізбек тұқымдасын, санын, қолданылуын, тасымалдаушысын/жүктемесін, негізгі өлшемдерін және жаңа бөлшек шешуі керек жұмыс жағдайын анықтаңыз. Қолданыстағы код белгісіз болған кезде фотосуреттерді немесе сызбаларды тіркеңіз және ашық материалдарды, құжаттаманы немесе жеткізу талаптарын көрінетін етіп сақтаңыз.
Make the selection from interfaces, not from one catalogue dimension
A useful selection sequence starts with the carrier and rail, then moves to the chain and sprocket. Measure several pitches, identify the roller arrangement and compare plate height, pin dimensions and roller position against the drawing. Confirm the sprocket tooth count and bore and check whether the chain enters the rail smoothly after leaving the sprocket. For side-roller or hollow-pin designs, include the outboard rail or cross-rod interface in the same review. For Double Plus layouts, state the required conveying and accumulation behavior together with queue length and stop sequence. If any key dimension is unknown, leave it as an RFQ confirmation item instead of filling it from a neighboring model.
Geometry
Pitch over several joints, roller arrangement, pin/plate dimensions and strand spacing.
Көлік жүргізу
Sprocket tooth count, bore, shaft alignment, take-up and chain entry/exit geometry.
Duty
Speed, starts per hour, maximum queue, carrier mass and environmental conditions.
Confirm the model
Compare the complete model drawing and list any unstated material, tolerance or application requirement in the enquiry.
Record both transport and accumulation conditions
When reviewing Double Plus Chain Working Principle Explained, collect data from the conveyor while carriers are moving freely and again while the longest realistic queue is stopped. Record loaded carrier mass, carrier spacing, conveyor and carrier speed where available, stop position, release interval and restart sequence. Mark a carrier so its movement can be followed through the queue, and compare both strands on a dual-chain system. Photographs should show the roller/rail interface from the end as well as the chain from the side.
Use the same survey to check the drive and supporting geometry. Count sprocket teeth, record bore or shaft arrangement, note take-up position, and look for polished edges or impact marks at rail joints and transfers. If the conveyor is being modified rather than simply repaired, include the new takt time, maximum queue and any change in pallet mass. These observations make it possible to distinguish a chain-family question from a rail, stop or timing problem before parts are specified.
Free travel
Carrier speed, roller rotation, tracking and transfer support.
Queued travel
Maximum accumulation, stop contact, drag and restart behavior.
Көлік жүргізу
Sprocket tooth count, shaft arrangement, take-up and chain entry.
Machine interface
Rail section, carrier underside, strand centers and station clearances.
Observe the two operating states of a Double Plus conveyor
A useful field check includes both free-running travel and accumulation. Mark one carrier and note its travel speed while the chain is moving normally, then stop that carrier in a controlled accumulation zone while the chain continues. Watch the large and small rollers, rail contact and the carrier underside. The purpose is not to estimate a ratio by eye, but to confirm that the installed roller arrangement and guide geometry behave as intended in both states.
Next release a short queue of representative loaded carriers. A clean restart should not produce sudden side movement, roller skidding or an impact at the first rail joint. Compare both strands on dual-chain conveyors. If one side leads, check rail height, sprocket timing, take-up position and carrier stiffness before increasing chain tension.
When requesting a chain, state the model if known, pitch, roller dimensions, required carrier speed, base chain speed when available, loaded carrier mass and maximum queue. Include an end-view photograph that shows which roller runs on the rail. This is more reliable than treating “Double Plus” as a complete specification.

























