Productbeschrijving
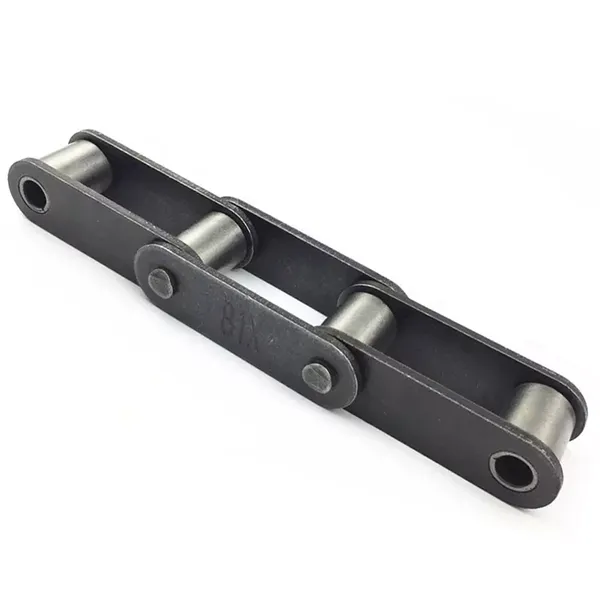
High Quality & Made to Order Stainless Steel Table Top Conveyor Chain (TS635)
Productbeschrijving
1. Material: Stainless steel chain / Alloy Carbon Steel
2. Surface Treatment: Zinc-Plated / Nickel-Plated / Dacromet-Plated
3. Short pitch stainless steel conveyor chain with attachments.
4. Double pitch stainless steel conveyor chain.
5. Double pitch hollow pin chain.
Note: If you have drawing or samples, we can do the special conveyor chains.
| Product name | Table Top Conveyor Chain (TS635) |
| Materials Available | 1. Stainless Steel: SS304, SS316, etc |
| 2. Alloy Steel: 45Mn, 42CrMo, etc | |
| 3. OEM according to your request | |
| Surface Treatment | Shot peening, Polishing, Oxygenation, Blackening, Zinc-plated, Nickel-plated, Anodized, etc. |
| Characteristic | Fire Resistant, Oil Resistant, Heat Resistant |
| Sollicitatie | Mainly used in products transmission |
| Design criterion | ISO DIN ANSI & Customer’s Drawing |
| Size | Customer’s Drawing & ISO standard |
| Package | Wooden Case / Container and pallet, or made-to-order |
| Certificaat | ISO9001: 2008 |
| Advantage | First quality, Best service, Competitive price, Fast delivery |
| Delivery Time | 20 days for samples. 45 days for official order. |
View more products,please click here…
Company Profile
| Materiaal: | Stainless Steel |
|---|---|
| Structuur: | Conveyor Chain |
| Oppervlaktebehandeling: | Oil Blooming |
| Kettingmaat: | Ts635 |
| Functie: | Hittebestendig |
| Sample: | for Free |
| Voorbeelden: |
US$ 0/Meter
1 meter (minimale bestelling) | |
|---|
| Aanpassing: |
Beschikbaar
| Aanvraag op maat |
|---|

Waar moet je op letten bij de keuze van een corrosiebestendige transportketting?
Bij de keuze voor een corrosiebestendige transportketting moet rekening worden gehouden met verschillende factoren om de levensduur en prestaties van de ketting in corrosieve omgevingen te garanderen. Hieronder volgen enkele belangrijke aandachtspunten:
1. Materiaalkeuze: Kies een kettingmateriaal dat van nature corrosiebestendig is. Roestvrij staal, zoals AISI 304 of AISI 316, is een veelgebruikte keuze vanwege de uitstekende corrosiebestendigheid. Andere materialen, zoals kunststof kettingen of speciale legeringen, kunnen ook worden overwogen, afhankelijk van de specifieke toepassingseisen.
2. Coatings en oppervlaktebehandelingen: In sommige gevallen kunnen extra beschermende coatings of oppervlaktebehandelingen worden aangebracht om de corrosiebestendigheid van de ketting te verbeteren. Deze coatings, zoals verzinken, galvaniseren of epoxycoatings, vormen een barrière tussen het kettingmateriaal en corrosieve stoffen, waardoor direct contact wordt voorkomen en het risico op corrosie wordt verminderd.
3. Milieucompatibiliteit: Houd rekening met de specifieke corrosieve stoffen die aanwezig zijn in de omgeving waar de transportketting zal worden gebruikt. Verschillende corrosieve stoffen, zoals zuren, basen of zout water, vereisen specifieke weerstandseigenschappen. Zorg ervoor dat het gekozen kettingmateriaal en de coatings compatibel zijn met de corrosieve stoffen in de gebruiksomgeving.
4. Onderhoud en smering: Goed onderhoud en smering spelen een cruciale rol bij het voorkomen van corrosie en het verlengen van de levensduur van een transportketting. Regelmatige reiniging, inspectie en het aanbrengen van geschikte smeermiddelen kunnen helpen bij het verwijderen van corrosieve verontreinigingen en het beschermen van het kettingoppervlak tegen aantasting.
5. Testen en certificering: Overweeg kettingen die zijn getest en gecertificeerd op corrosiebestendigheid volgens relevante industrienormen. Zoek naar certificeringen zoals ISO 9227 (zoutsproeitest) of ASTM B117 (corrosiebestendigheidstest) om de prestaties van de ketting in corrosieve omgevingen te garanderen.
Door zorgvuldig rekening te houden met deze factoren en te overleggen met fabrikanten van transportkettingen of experts op het gebied van corrosiebestendigheid, kunt u een ketting selecteren die goed geschikt is voor uw specifieke corrosieve omgeving. Zo minimaliseert u het risico op corrosieproblemen en bent u verzekerd van optimale prestaties en een lange levensduur.
What are the future trends and advancements in conveyor chain technology?
The field of conveyor chain technology is constantly evolving, driven by the need for improved efficiency, productivity, and sustainability. Here are some of the future trends and advancements in conveyor chain technology:
1. Automation and robotics: The integration of conveyor chains with automation and robotics systems is a growing trend. This includes the use of advanced sensors, machine vision, and artificial intelligence to enable autonomous operation, precise positioning, and efficient material handling.
2. Smart and connected systems: Conveyor chains are becoming increasingly connected through the Internet of Things (IoT) technology. This allows for real-time monitoring, data collection, and analysis of various performance parameters such as chain wear, tension, temperature, and energy consumption. Smart systems can optimize maintenance schedules, detect potential failures, and improve overall system efficiency.
3. Lightweight and high-strength materials: The development of lightweight yet high-strength materials is an ongoing focus in conveyor chain technology. Advanced alloys, composites, and engineered plastics offer improved strength-to-weight ratios, reducing energy consumption and increasing the load capacity of conveyor systems.
4. Energy efficiency: Energy efficiency is a key consideration in conveyor chain design. Future advancements aim to minimize power consumption through the use of efficient drive systems, regenerative braking, and smart control algorithms that optimize speed and acceleration profiles. Energy recovery technologies, such as regenerative drives, can also capture and reuse energy during deceleration or braking.
5. Sustainability and environmental friendliness: Conveyor chain technology is moving towards more sustainable and environmentally friendly solutions. This includes the use of eco-friendly materials, improved lubrication techniques to minimize environmental impact, and the adoption of energy-efficient components and systems. Recycling and circular economy concepts are also gaining prominence in the design and manufacturing of conveyor chains.
6. Advanced wear monitoring and predictive maintenance: The future of conveyor chain technology involves advanced wear monitoring systems that can accurately predict the remaining useful life of chains and components. This enables proactive maintenance planning and reduces unplanned downtime. Predictive maintenance algorithms analyze data collected from sensors and provide timely alerts for chain replacement or repair.
These are just a few examples of the future trends and advancements in conveyor chain technology. As technology continues to advance, we can expect further innovations that enhance performance, efficiency, reliability, and sustainability in conveyor systems.

What are the cost considerations when purchasing a conveyor chain?
When purchasing a conveyor chain, there are several cost considerations that need to be taken into account to ensure an optimal investment and operational efficiency.
1. Initial Cost: The initial cost of the conveyor chain includes the cost of the chain itself, as well as any additional components such as sprockets, attachments, and connecting links. It is important to compare prices from different suppliers and evaluate the overall value for the money.
2. Maintenance and Repair Costs: Consider the long-term maintenance and repair costs associated with the conveyor chain. Some chains may require more frequent lubrication or replacement of components, which can add to the overall operating expenses.
3. Service Life: The service life of the conveyor chain is an essential factor in determining its cost-effectiveness. Chains with longer service life may have a higher initial cost but can result in lower replacement and downtime costs in the long run.
4. Energy Efficiency: Energy consumption is an ongoing cost to consider. Conveyor chains that offer lower friction and efficient power transmission can contribute to energy savings and reduce operating expenses.
5. Maintenance Ease: Consider the ease of maintenance when selecting a conveyor chain. Chains that are easier to clean, inspect, and maintain can reduce labor costs and increase operational efficiency.
6. Compatibility and Integration: Ensure that the selected conveyor chain is compatible with the existing conveyor system or equipment. Retrofitting or modifying the system to accommodate a specific chain may incur additional costs.
7. Supplier Support and Warranty: Evaluate the level of technical support provided by the supplier and the warranty coverage offered for the conveyor chain. This can impact the overall cost of ownership and provide peace of mind in case of any unforeseen issues.
It is important to consider these factors holistically and make a cost-benefit analysis based on the specific requirements of the application. Choosing a conveyor chain that aligns with the budget, performance needs, and long-term cost considerations will help optimize the investment and ensure efficient material handling operations.
editor by CX 2023-10-17