
Product Description
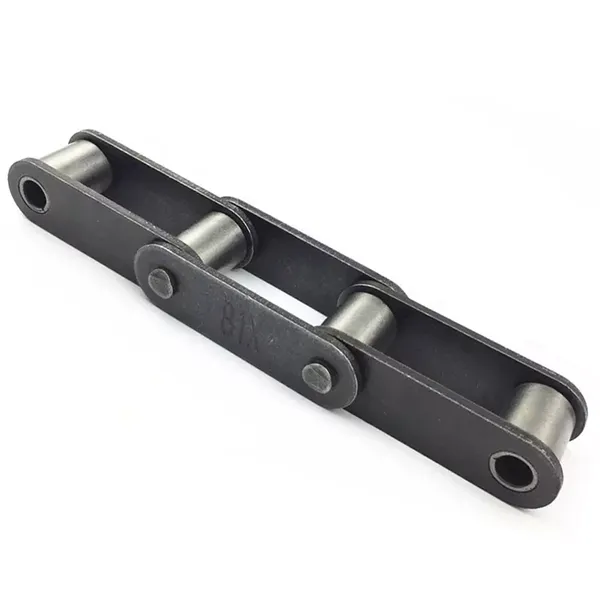
High Quality & Made to Order Stainless Steel Table Top Conveyor Chain (TS635)
Product Description
1. Material: Stainless steel chain / Alloy Carbon Steel
2. Surface Treatment: Zinc-Plated / Nickel-Plated / Dacromet-Plated
3. Short pitch stainless steel conveyor chain with attachments.
4. Double pitch stainless steel conveyor chain.
5. Double pitch hollow pin chain.
Note: If you have drawing or samples, we can do the special conveyor chains.
| Product name | Table Top Conveyor Chain (TS635) |
| Materials Available | 1. Stainless Steel: SS304, SS316, etc |
| 2. Alloy Steel: 45Mn, 42CrMo, etc | |
| 3. OEM according to your request | |
| Surface Treatment | Shot peening, Polishing, Oxygenation, Blackening, Zinc-plated, Nickel-plated, Anodized, etc. |
| Characteristic | Fire Resistant, Oil Resistant, Heat Resistant |
| Application | Mainly used in products transmission |
| Design criterion | ISO DIN ANSI & Customer’s Drawing |
| Size | Customer’s Drawing & ISO standard |
| Package | Wooden Case / Container and pallet, or made-to-order |
| Certificate | ISO9001: 2008 |
| Advantage | First quality, Best service, Competitive price, Fast delivery |
| Delivery Time | 20 days for samples. 45 days for official order. |
View more products,please click here…
Company Profile
| Material: | Stainless Steel |
|---|---|
| Structure: | Conveyor Chain |
| Surface Treatment: | Oil Blooming |
| Chain Size: | Ts635 |
| Feature: | Heat Resistant |
| Sample: | for Free |
| Samples: |
US$ 0/Meter
1 Meter(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|

What are the considerations for selecting a corrosion-resistant conveyor chain?
When selecting a corrosion-resistant conveyor chain, several factors need to be considered to ensure the chain’s longevity and performance in corrosive environments. Here are some key considerations:
1. Material Selection: Choose a chain material that is inherently resistant to corrosion. Stainless steel, such as AISI 304 or AISI 316, is a common choice due to its excellent corrosion resistance properties. Other materials like plastic chains or special alloys can also be considered based on the specific application requirements.
2. Coatings and Surface Treatments: In some cases, additional protective coatings or surface treatments can be applied to enhance the chain’s corrosion resistance. These coatings, such as zinc plating, galvanizing, or epoxy coatings, create a barrier between the chain material and corrosive substances, preventing direct contact and reducing the risk of corrosion.
3. Environmental Compatibility: Consider the specific corrosive agents present in the environment where the conveyor chain will be used. Different corrosive substances, such as acids, alkalis, or saltwater, require specific resistance properties. Ensure that the selected chain material and coatings are compatible with the corrosive agents present in the operating environment.
4. Maintenance and Lubrication: Proper maintenance and lubrication play a crucial role in preventing corrosion and extending the life of a conveyor chain. Regular cleaning, inspection, and application of appropriate lubricants can help remove corrosive contaminants and protect the chain surface from degradation.
5. Testing and Certification: Consider chains that have undergone testing and certification for corrosion resistance in relevant industry standards. Look for certifications such as ISO 9227 (salt spray test) or ASTM B117 (corrosion resistance test) to ensure the chain’s performance in corrosive environments.
By carefully considering these factors and consulting with conveyor chain manufacturers or corrosion-resistant experts, you can select a chain that is well-suited for your specific corrosive environment, minimizing the risk of corrosion-related issues and ensuring optimal performance and longevity.
What are the future trends and advancements in conveyor chain technology?
The field of conveyor chain technology is constantly evolving, driven by the need for improved efficiency, productivity, and sustainability. Here are some of the future trends and advancements in conveyor chain technology:
1. Automation and robotics: The integration of conveyor chains with automation and robotics systems is a growing trend. This includes the use of advanced sensors, machine vision, and artificial intelligence to enable autonomous operation, precise positioning, and efficient material handling.
2. Smart and connected systems: Conveyor chains are becoming increasingly connected through the Internet of Things (IoT) technology. This allows for real-time monitoring, data collection, and analysis of various performance parameters such as chain wear, tension, temperature, and energy consumption. Smart systems can optimize maintenance schedules, detect potential failures, and improve overall system efficiency.
3. Lightweight and high-strength materials: The development of lightweight yet high-strength materials is an ongoing focus in conveyor chain technology. Advanced alloys, composites, and engineered plastics offer improved strength-to-weight ratios, reducing energy consumption and increasing the load capacity of conveyor systems.
4. Energy efficiency: Energy efficiency is a key consideration in conveyor chain design. Future advancements aim to minimize power consumption through the use of efficient drive systems, regenerative braking, and smart control algorithms that optimize speed and acceleration profiles. Energy recovery technologies, such as regenerative drives, can also capture and reuse energy during deceleration or braking.
5. Sustainability and environmental friendliness: Conveyor chain technology is moving towards more sustainable and environmentally friendly solutions. This includes the use of eco-friendly materials, improved lubrication techniques to minimize environmental impact, and the adoption of energy-efficient components and systems. Recycling and circular economy concepts are also gaining prominence in the design and manufacturing of conveyor chains.
6. Advanced wear monitoring and predictive maintenance: The future of conveyor chain technology involves advanced wear monitoring systems that can accurately predict the remaining useful life of chains and components. This enables proactive maintenance planning and reduces unplanned downtime. Predictive maintenance algorithms analyze data collected from sensors and provide timely alerts for chain replacement or repair.
These are just a few examples of the future trends and advancements in conveyor chain technology. As technology continues to advance, we can expect further innovations that enhance performance, efficiency, reliability, and sustainability in conveyor systems.

What are the cost considerations when purchasing a conveyor chain?
When purchasing a conveyor chain, there are several cost considerations that need to be taken into account to ensure an optimal investment and operational efficiency.
1. Initial Cost: The initial cost of the conveyor chain includes the cost of the chain itself, as well as any additional components such as sprockets, attachments, and connecting links. It is important to compare prices from different suppliers and evaluate the overall value for the money.
2. Maintenance and Repair Costs: Consider the long-term maintenance and repair costs associated with the conveyor chain. Some chains may require more frequent lubrication or replacement of components, which can add to the overall operating expenses.
3. Service Life: The service life of the conveyor chain is an essential factor in determining its cost-effectiveness. Chains with longer service life may have a higher initial cost but can result in lower replacement and downtime costs in the long run.
4. Energy Efficiency: Energy consumption is an ongoing cost to consider. Conveyor chains that offer lower friction and efficient power transmission can contribute to energy savings and reduce operating expenses.
5. Maintenance Ease: Consider the ease of maintenance when selecting a conveyor chain. Chains that are easier to clean, inspect, and maintain can reduce labor costs and increase operational efficiency.
6. Compatibility and Integration: Ensure that the selected conveyor chain is compatible with the existing conveyor system or equipment. Retrofitting or modifying the system to accommodate a specific chain may incur additional costs.
7. Supplier Support and Warranty: Evaluate the level of technical support provided by the supplier and the warranty coverage offered for the conveyor chain. This can impact the overall cost of ownership and provide peace of mind in case of any unforeseen issues.
It is important to consider these factors holistically and make a cost-benefit analysis based on the specific requirements of the application. Choosing a conveyor chain that aligns with the budget, performance needs, and long-term cost considerations will help optimize the investment and ensure efficient material handling operations.


editor by CX 2023-10-17

























