
Stops, Locators and Indexing on Pallet Conveyors
Practical engineering guide: Stops, Locators and Indexing on Pallet Conveyors. Selection, interfaces, application checks, maintenance and RFQ inputs.
This guide focuses on how transport stopping differs from precision locating and why process datums should be designed separately. It is written for machine builders, maintenance teams and buyers who need a chain selection that can be checked against drawings and the real conveyor rather than a generic product label.
Stops, Locators and Indexing on Pallet Conveyors
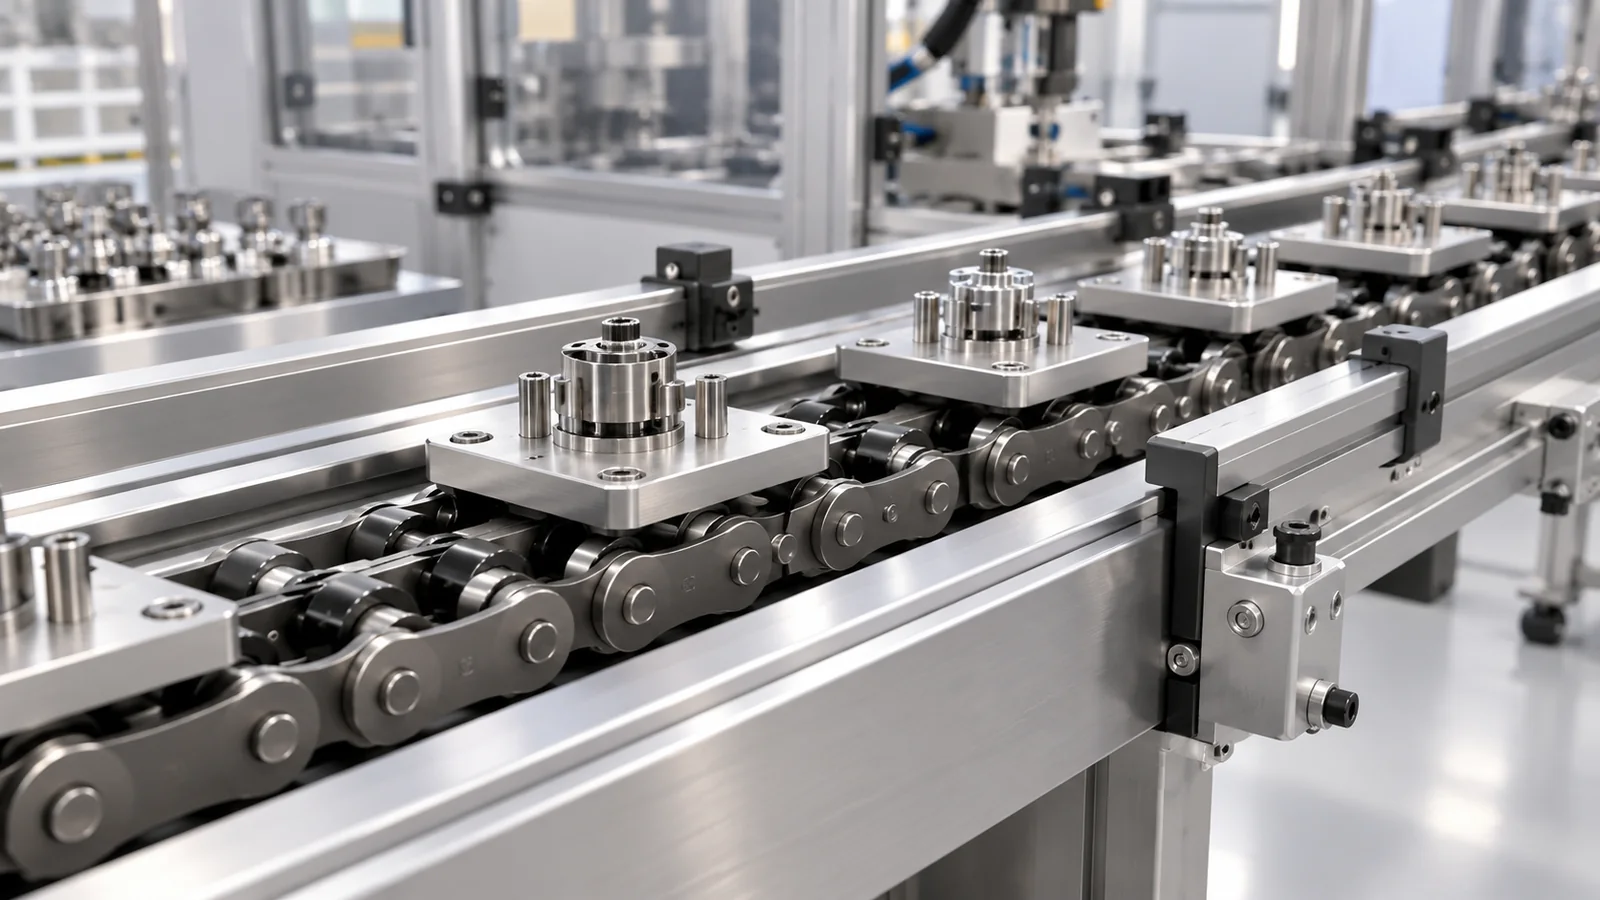
A pallet conveyor looks simple from a distance, but its reliability depends on several interfaces working at the same time. In a typical project such as an assembly station with a pneumatic stopper and locating pins, chain pitch, roller contact, rail alignment, sprocket engagement, carrier stiffness, stops and maintenance access all influence the result. A useful engineering review therefore combines model-level data with the operating sequence of the machine.
இந்தப் பிரச்சினை ஏன் முக்கியமானது
How transport stopping differs from precision locating and why process datums should be designed separately affects more than catalogue selection. It changes how the workpiece carrier enters a station, how loads pass into guide rails, how the chain approaches the drive and how the system behaves during stopping or accumulation. If one interface is ignored, the symptom may appear somewhere else: a roller can wear because a rail joint is high, a chain can pull sideways because a pallet stop is offset, or a new chain can run badly because the old sprocket is worn.
The practical objective is not to eliminate every variation in the machine. It is to identify the variables that must be controlled, define which dimensions are fixed by the chain source, and leave unsupported items for explicit RFQ confirmation. This is also why using chain tension as the locating force is a risky shortcut. It replaces measurable machine data with an assumption and can make a correct-looking part fail at installation.
முதலில் வரையறுக்க வேண்டிய நான்கு சோதனைகள்
Stop Face
Define the loaded condition, contact or datum surface, position and force path so the carrier interface can be checked.
Locator Datum
Define the loaded condition, contact or datum surface, position and force path so the carrier interface can be checked.
Lift-And-Locate Motion
கன்வேயரின் இந்தப் பகுதிக்குப் பொருந்தக்கூடிய அளவிடக்கூடிய நிலை, நிறுவப்பட்ட இடைமுகம் மற்றும் ஏற்புச் சரிபார்ப்பு ஆகியவற்றைக் குறிப்பிடவும்.
Sensor Timing
கன்வேயரின் இந்தப் பகுதிக்குப் பொருந்தக்கூடிய அளவிடக்கூடிய நிலை, நிறுவப்பட்ட இடைமுகம் மற்றும் ஏற்புச் சரிபார்ப்பு ஆகியவற்றைக் குறிப்பிடவும்.
துல்லியமான சங்கிலி வடிவவியலுடன் தொடங்குங்கள்
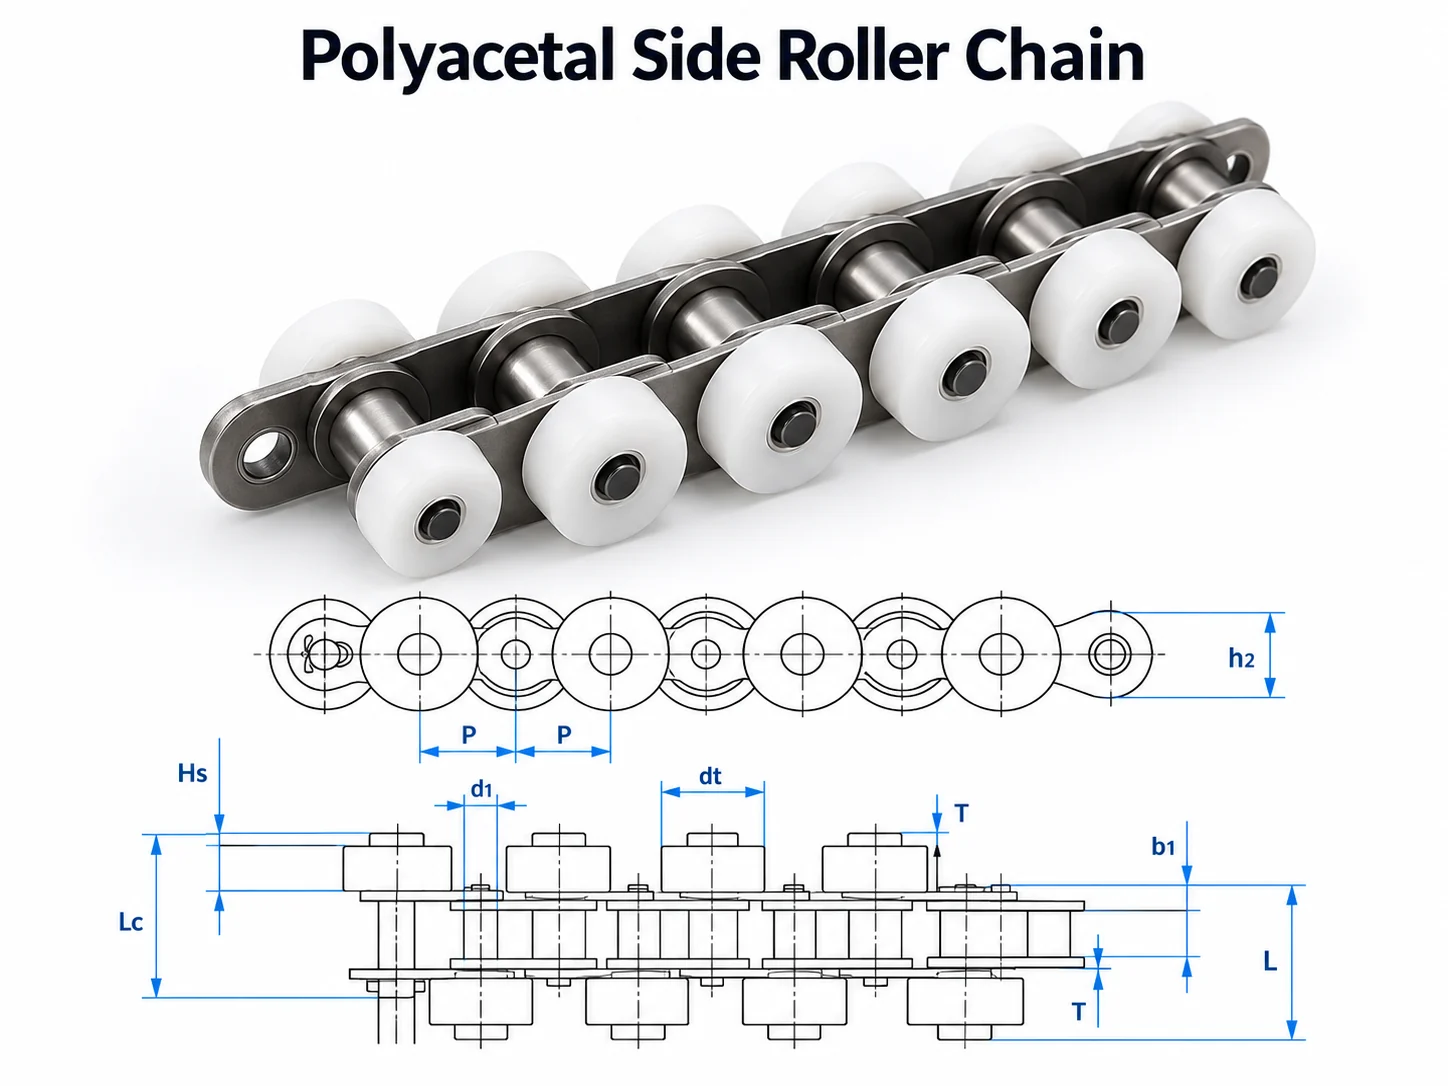
மாடல் எண் கிடைக்கும்போது, சரியான மாடல் விவரக்குறிப்பு மற்றும் அதனுடன் பொருந்தும் வரைபடத்தைப் பயன்படுத்தவும். பிட்ச், ரோலர் விட்டங்கள், உள் அகலம், பின் விட்டம் மற்றும் நீளம், பிளேட் உயரம் மற்றும் தடிமன், மற்றும் கன்வேயருடன் இணையும் ஏதேனும் பக்கவாட்டு ரோலர், பெரிய ரோலர் அல்லது உள்ளீடற்ற பின் ஆகியவற்றின் பரிமாணங்களை ஒப்பிட்டுப் பார்க்கவும். குறியீடு தெரியாதபோது, நிறுவப்பட்ட சங்கிலியை முறையாக அளவிடவும். தேய்ந்துபோன ஒற்றை இடைவெளியை அளவிடுவதை விட, பல பின்களுக்கு இடையே பிட்சை அளவிடுவது மிகவும் நம்பகமானது. மேலும், புகைப்படங்கள் பக்கவாட்டுத் தோற்றம், ரோலர் அமைப்பு, ஸ்ப்ராக்கெட் மற்றும் ரெயில் தொடர்பு ஆகியவற்றைக் காட்ட வேண்டும்.
இழுவிசை வலிமையை பேலட் பேலோடாகப் பயன்படுத்த வேண்டாம். பட்டியல் இழுவிசை எண்கள் என்பவை பொருள்/கூறு சோதனைப் பண்புகளாகும். கன்வேயரின் இயக்க நிலைமைகளில், லைன் நீளம், சங்கிலி இழைகளின் எண்ணிக்கை, கேரியர் எண்ணிக்கை, முடுக்கம், அதிர்ச்சி, உராய்வு, உயவு, ஸ்ப்ராக்கெட் அளவு, தேய்மான நிலை மற்றும் தேவையான பாதுகாப்பு காரணி ஆகியவையும் அடங்கும். அந்த நிலைமைகள் புரிந்து கொள்ளப்பட்ட பின்னரே ஒரு அமைப்புக்கான சங்கிலியைச் சரிபார்க்க முடியும்.
தேர்வு பணிப்பாய்வு
- Stop Face: தேவையான நிபந்தனையைத் துல்லியமான சங்கிலி வரைபடம் அல்லது அமைப்பு தளவமைப்புடன் ஒப்பிட்டு, விலைக்கோப்பு உறுதிப்படுத்தலுக்கான (RFQ) விடுபட்ட சந்தேகங்களைப் பதிவு செய்யவும்.
- Locator Datum: தேவையான நிபந்தனையைத் துல்லியமான சங்கிலி வரைபடம் அல்லது அமைப்பு தளவமைப்புடன் ஒப்பிட்டு, விலைக்கோப்பு உறுதிப்படுத்தலுக்கான (RFQ) விடுபட்ட சந்தேகங்களைப் பதிவு செய்யவும்.
- Lift-And-Locate Motion: தேவையான நிபந்தனையைத் துல்லியமான சங்கிலி வரைபடம் அல்லது அமைப்பு தளவமைப்புடன் ஒப்பிட்டு, விலைக்கோப்பு உறுதிப்படுத்தலுக்கான (RFQ) விடுபட்ட சந்தேகங்களைப் பதிவு செய்யவும்.
- Sensor Timing: தேவையான நிபந்தனையைத் துல்லியமான சங்கிலி வரைபடம் அல்லது அமைப்பு தளவமைப்புடன் ஒப்பிட்டு, விலைக்கோப்பு உறுதிப்படுத்தலுக்கான (RFQ) விடுபட்ட சந்தேகங்களைப் பதிவு செய்யவும்.
- போக்குவரத்து மற்றும் கடமை: ஏற்றப்பட்ட கேரியர் நிறை, கேரியர்களின் எண்ணிக்கை, லைன் வேகம், ஒரு மணி நேரத்திற்கான தொடக்கங்கள், குவிப்பு முறை மற்றும் ஏதேனும் சாய்வு அல்லது செங்குத்து மாற்றம் ஆகியவற்றை பதிவு செய்யவும்.
- ஓட்டிச் சென்று திரும்புதல்: ஸ்ப்ராக்கெட் தரவு, ஷாஃப்ட் சீரமைப்பு, டேக்-அப் வரம்பு, ரிட்டர்ன் சப்போர்ட் மற்றும் லூப்ரிகேஷன் அணுகல் ஆகியவற்றை உறுதிப்படுத்தவும்.
- வெளியீட்டு நிபந்தனை: சிறப்புப் பொருள் தரம், பூச்சு, அனுமதிக்கப்பட்ட அமைப்புச் சுமை அல்லது சுற்றுச்சூழல் மதிப்பீடு போன்ற, தொழில்நுட்பத் தரவுகளில் குறிப்பிடப்படாத எந்தவொரு புலத்தையும் மதிப்பிடுவதற்குப் பதிலாக, RFQ உறுதிப்படுத்தல் இனமாகப் பட்டியலிடவும்.
அமைப்பு ஒருங்கிணைப்பு
சங்கிலி அடையாளம் காணப்பட்டவுடன், கன்வேயர் இயந்திரத்தின் மற்ற பகுதிகளுக்குச் சுமையை எவ்வாறு மாற்றுகிறது என்பதைச் சரிபார்க்கவும். வழிகாட்டி அல்லது தேய்மானப் பட்டை, உத்தேசிக்கப்பட்ட உருளை மேற்பரப்பைத் தாங்க வேண்டும் மற்றும் இணைப்புகள் வழியாகத் தொடர்ச்சியாக இருக்க வேண்டும். இணை இழைகள் குறிப்பிட்ட மையத் தூரத்தையும் ஒத்திசைக்கப்பட்ட இயக்க நேரத்தையும் கொண்டிருக்க வேண்டும். நிறுத்தங்கள், சங்கிலியின் பக்கத் தகட்டை அல்லாமல், வடிவமைக்கப்பட்ட தட்டு முகத்தைத் தொட வேண்டும். குறுக்கு இடமாற்றங்கள் மற்றும் தூக்குதல்களுக்குப் போதுமான ஆதரவு தேவை, அப்போதுதான் கேரியர் ஒரு இடைவெளியில் விழவோ அல்லது ஒரு முள்/தட்டின் விளிம்பில் இறங்கவோ செய்யாது.
பொருட்களைக் குவிக்கும் அமைப்புகளுக்கு, போக்குவரத்தை நிறுத்துவதிலிருந்து பிரிக்கவும். கேரியர் நிறுத்தப்பட்டிருக்கும்போது சங்கிலி தொடர்ந்து நகரலாம், ஆனால் நிறுத்தும் விசை, வரிசை நீளம், மறுதொடக்கம் செய்யும் முறை மற்றும் உள்ளூர் உராய்வு ஆகியவற்றை இன்னும் சரிபார்க்க வேண்டும். செயலாக்கத்திற்காக ஒரு பணிப்பொருளை நிலைநிறுத்தும் அமைப்புகளுக்கு, சாதாரண கன்வேயர் போக்குவரத்து வழங்கக்கூடியதை விடத் தேவையான மீண்டும் மீண்டும் செய்யும் துல்லியம் இறுக்கமாக இருக்கும்போது, பிரத்யேக இருப்பிட அம்சங்களைப் பயன்படுத்தவும்.
செயல்பாட்டுக்குக் கொண்டுவருதல் மற்றும் பராமரிப்பு
புதிய அல்லது பழுதுபார்க்கப்பட்ட கன்வேயரை முதலில் குறைந்த வேகத்தில் இயக்கவும். பல முழுமையான சங்கிலிச் சுற்றுகளை மெதுவாக இயக்கி, அதன் இயக்கம், திரும்புதல், தண்டவாள மாற்றங்கள், நிறுத்தங்கள் மற்றும் இடமாற்றங்களைக் கவனிக்கவும். சங்கிலியின் ஒவ்வொரு சுற்றுக்கும் அல்லது ஸ்ப்ராக்கெட்டின் ஒவ்வொரு சுழற்சிக்கும் ஒருமுறை மீண்டும் மீண்டும் வரும் ஒலிகளைக் கவனியுங்கள், ஏனெனில் அந்த வடிவங்கள் இறுக்கமான இணைப்பு, ரோலர் சேதம், தண்டவாளத்தின் குறிப்பிட்ட பகுதியில் ஏற்படும் ஏற்ற இறக்கம் அல்லது ஸ்ப்ராக்கெட் சிக்கலைக் கண்டறிய உதவுகின்றன. கடினமான வேலைப்பொருள் தட்டுகளில், இணையாக உள்ள இழைகளில் ஏற்படும் சாய்வைக் கவனியுங்கள்; சிறிய நேர வேறுபாடுகள் கூட கேரியரின் ஒரு பக்கத்தில் சுமையை ஏற்படுத்தக்கூடும்.
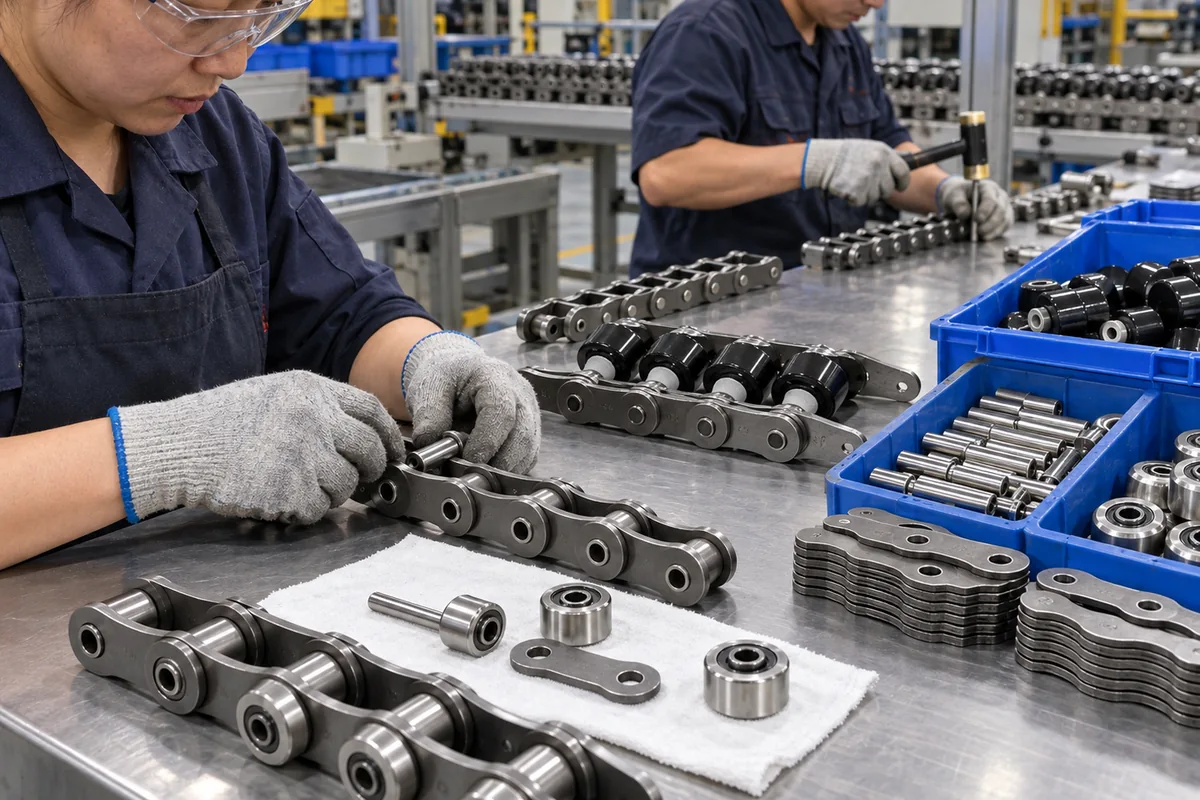
பராமரிப்பு என்பது ஒரு கோளாறுக்காகக் காத்திருப்பதை விடுத்து, அதன் போக்குகளைக் கண்காணிப்பதாக இருக்க வேண்டும். அங்கீகரிக்கப்பட்ட முறையைப் பயன்படுத்தி நீட்சி அல்லது நீளச் சோதனைகளைப் பதிவு செய்யவும்; உருளைகளின் தடையற்ற சுழற்சி மற்றும் அசாதாரணமான தட்டையான பகுதிகளை ஆய்வு செய்யவும்; சீரற்ற நிலையைக் குறிக்கும் மெருகூட்டப்பட்ட பக்கவாட்டுத் தொடர்பு அடையாளங்களைத் தேடவும்; பற்சக்கரப் பற்களை ஆய்வு செய்து, அதன் பிடிப்பு நிலையைச் சரிபார்க்கவும். மசகு எண்ணெய் இடும் இடைவெளிகள், இயக்கச் சூழலையும் சங்கிலி உற்பத்தியாளரின் வழிகாட்டுதலையும் பிரதிபலிக்க வேண்டும்; மசகு எண்ணெய் சிராய்ப்பு அசுத்தங்களை ஈர்த்தாலோ அல்லது ஒரு செயல்முறைப் பகுதிக்குள் நுழைந்தாலோ, அதிக மசகு எண்ணெய் இடுவது தானாகவே சிறந்ததாகிவிடாது.
RFQ சரிபார்ப்புப் பட்டியல்
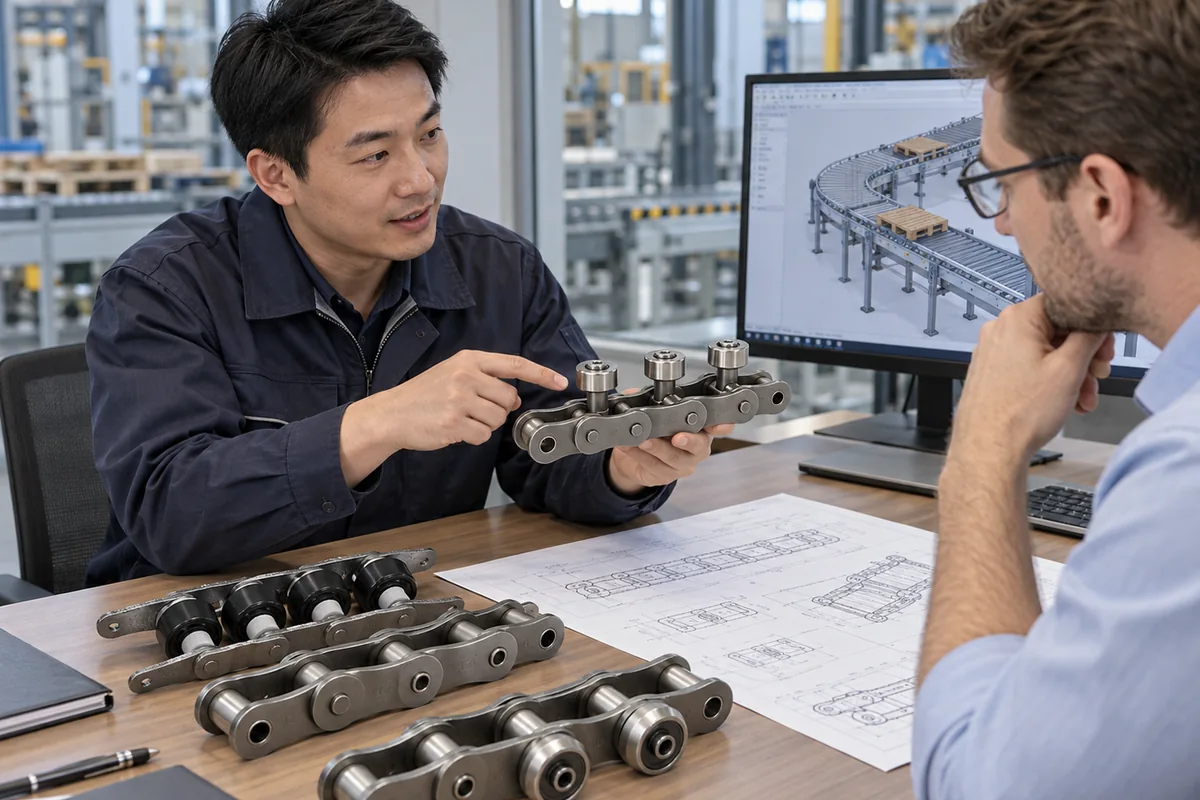
மாற்று கோரிக்கைக்கு, மாடல் குறியீடு (தெளிவாகத் தெரிந்தால்), அளவிடப்பட்ட பிட்ச், ரோலர் அமைப்பு, சங்கிலி அகலம், தட்டு உயரம், பின் பரிமாணங்கள், பக்கவாட்டுத் தோற்றத்தின் புகைப்படம் மற்றும் ஸ்ப்ராக்கெட்/ரெயில் தொடர்பைக் காட்டும் புகைப்படம் ஆகியவற்றை அனுப்பவும். ஒரு புதிய அமைப்புக்கு, கன்வேயர் நீளம், கேரியர் அளவு மற்றும் ஏற்றப்பட்ட நிறை, இழைகளின் எண்ணிக்கை, இழை இடைவெளி, வேகம், தொடக்கங்கள்/நிறுத்தங்கள், பஃபர் நீளம், சுற்றுச்சூழல் நிலைமைகள் மற்றும் சேரும் நாடு ஆகியவற்றைச் சேர்க்கவும். இந்த விவரங்கள், ஒரு முழுமையான கன்வேயர்-பணி கணக்கீட்டிலிருந்து சங்கிலிப் பொருத்தத்தைப் பிரித்தெடுக்க உதவுகின்றன.
Separate transport, stopping and precision locating
A conveyor stop should arrest a designed face on the pallet; precision locating should use dedicated datum features or a lift-and-locate mechanism when the process requires tighter repeatability than conveyor transport provides.
Record stop position, approach speed, carrier mass and whether a queue can build behind the station. Check that machining, pressing or test forces are reacted by the station structure instead of being transmitted through the chain or a free-running roller.
இடைமுகத்தை அளவிடவும்
ஏற்கனவே உள்ள இயந்திரத்தில் ஒரு மாற்றுப் பாகம் பொருந்த வேண்டியிருக்கும் போது, பல்வேறு சுழற்சி அளவுகள், இறுதித் தோற்ற வடிவியல் மற்றும் பற்சக்கரம்/தண்டவாள விவரங்களைப் பயன்படுத்தவும்.
கடமையை விவரிக்கவும்
ஏற்றப்பட்ட கேரியரின் நிறை, வேகம், தொடக்கங்கள், திரள் அல்லது குறியீட்டு நடத்தை மற்றும் இயக்கச் சூழல் ஆகியவற்றை உள்ளடக்கவும்.
மிக மோசமான சூழ்நிலையைச் சோதித்துப் பாருங்கள்
வெறும் சுமையற்ற பயணத்தை மட்டும் கொண்டிராமல், புகழ்பெற்ற போக்குவரத்து நிறுவனங்களுடனான ஒப்பந்தம் மற்றும் மிகவும் சவாலான வரிசை, நிறுத்தம், இடமாற்றம் அல்லது மீண்டும் தொடங்குதல் போன்ற நிலைமைகளையும் கருத்தில் கொள்ள வேண்டும்.
திறந்த பொருட்களை வெளிப்படையாக வைத்திருங்கள்
பொருள், பூச்சு, சிறப்பு சகிப்புத்தன்மை, ஆவணத் தேவை அல்லது அனுமதிக்கப்பட்ட அமைப்புச் சுமை ஆகியவை குறிப்பிடப்படவில்லை எனில், அதை விசாரணையில் உறுதிப்படுத்தவும்.
அடிக்கடி கேட்கப்படும் கேள்விகள்
பேச்சு வழியை மட்டும் வைத்து ஒரு மாற்று நபரைத் தேர்ந்தெடுக்க முடியுமா?
For stops, locators and indexing on pallet conveyors, pitch is only the first filter. Confirm roller geometry, inner width, pins, plates and any side-roller or hollow-pin features against the installed conveyor before treating two chains as interchangeable.
அதிக இழுவிசை மதிப்பு இருந்தால், அந்தச் சுமையை நான் பலகையில் வைத்துத் தூக்கிச் செல்ல முடியுமா?
For stops, locators and indexing on pallet conveyors, do not convert tensile strength directly into pallet payload. Service load depends on strand count, friction, acceleration, stop impact, sprockets, rails and the safety margin used for the machine.
ஒரு மாதிரி குடும்பப் புகைப்படம் சரியான மாடலை நிரூபிக்க முடியுமா?
இல்லை. ஒரு மாதிரி குடும்பப் படம் கட்டமைப்பை விளக்க உதவக்கூடும், ஆனால் மாடலின் அடையாளம் மற்றும் பரிமாணங்கள், அந்த மாடலுக்கென உள்ள தொழில்நுட்ப விவரக்குறிப்பு, வரைபடம் அல்லது உறுதிசெய்யப்பட்ட உற்பத்தித் தரவுகளிலிருந்துதான் பெறப்பட வேண்டும்.
எந்தத் தகவல் ஒரு விலைப்புள்ளியை விரைவுபடுத்துகிறது?
For an RFQ related to stops, locators and indexing on pallet conveyors, send the model code or dimensional sketch, clear photographs, conveyor layout, loaded carrier information, quantity and delivery country so the review starts from reproducible machine data.
Key engineering variables for Stops, Locators and Indexing on Pallet Conveyors
இந்த முடிவு, ஒரு பொதுவான குடும்பப் பெயரைச் சார்ந்திருக்காமல், அளவிடக்கூடிய இயந்திர உள்ளீடுகள் மற்றும் துல்லியமான சங்கிலி வரைபடத்தைச் சார்ந்திருக்க வேண்டும். இயக்க நிகழ்வை ஒரே வரியில் பதிவு செய்யவும்: கன்வேயர் எதைக் கொண்டு செல்கிறது, அது எவ்வளவு வேகமாக நகர்கிறது, அது எங்கே நிற்கிறது மற்றும் எந்த நிலை இந்த ஆய்வைத் தூண்டியது என்பனவற்றைப் பதிவு செய்யவும். மற்றொரு பொறியாளர் மீண்டும் செய்து பார்க்கக்கூடிய பரிமாணங்களையும் அவதானிப்புகளையும் பதிவு செய்யவும்.
| உள்ளீடு | என்ன பதிவு செய்ய வேண்டும் | அது ஏன் முக்கியம் |
|---|---|---|
| கேரியர்/சுமை | ஏற்றப்பட்ட நிறை, ஈர்ப்பு மையம், கீழ்ப்புறத் தொடர்பு மற்றும் கேரியர் எண்ணிக்கை | ஆதரவு, உராய்வு மற்றும் நிறுத்த நடத்தை |
| இயக்கம் | வேகம், தொடக்கங்கள், நிறுத்தங்கள், திரட்டல் மற்றும் குறியிடல் | மாறும் தேவை மற்றும் செயல்முறை நேரம் |
| சங்கிலி பாதை | பிட்ச், ரோலர்கள், இழை இடைவெளி மற்றும் தண்டவாளங்கள் | இயந்திரப் பொருத்தம் மற்றும் கண்காணிப்பு |
| ஓட்டுநர் | ஸ்ப்ராக்கெட் பற்கள், சீரமைப்பு, இழுவை மற்றும் இயக்க நிலை | ஈடுபாடு மற்றும் பதற்றப் பரவல் |
| சுற்றுச்சூழல் | வெப்பநிலை, தூசி, ஈரப்பதம், சுத்தம் செய்தல் மற்றும் உயவு வரம்புகள் | பொருள் மற்றும் பராமரிப்புத் தேர்வுகள் |
தொடர்புடைய தயாரிப்பு மற்றும் தேர்வு ஆதாரங்கள்
பயன்படுத்தவும் தட்டு கன்வேயர் சங்கிலி பட்டியல் குடும்பங்களையும் ஒப்பிட்டுப் பார்க்க பொறியியல் தேர்வு பணிப்பாய்வு இயந்திரத் தரவு முழுமையடையாதபோது.
What to include with an enquiry about Stops, Locators and Indexing on Pallet Conveyors
நிறுவப்பட்ட அல்லது முன்மொழியப்பட்ட சங்கிலி வகை, அதன் எண்ணிக்கை, பயன்பாடு, தாங்கி/சுமை, முக்கிய பரிமாணங்கள் மற்றும் புதிய பாகம் தீர்க்க வேண்டிய இயக்க நிலை ஆகியவற்றை அடையாளம் காணவும். தற்போதுள்ள விதிமுறை நிச்சயமற்றதாக இருக்கும்போது புகைப்படங்கள் அல்லது வரைபடங்களை இணைக்கவும், மேலும் முடிக்கப்படாத பொருட்கள், ஆவணங்கள் அல்லது விநியோகத் தேவைகளைத் தெளிவாகத் தெரியும்படி வைக்கவும்.
Close the design loop with a measurable conveyor record
A pallet conveyor review should leave behind a compact machine record that another engineer or buyer can use later. Capture the chain model, measured pitch, carrier mass, strand spacing, rail section, sprocket data, conveyor speed, start/stop pattern, environment and quantity in one place. Add photographs of the chain, sprocket, carrier underside and the most critical transfer. For a new line, include the process sequence and station layout; for a replacement, include the old part number and the dimensions that were verified on the machine. This record makes later maintenance and procurement faster because the next decision is based on the installed interfaces rather than a product photograph or family name.
Machine
Carrier/load, layout, transfers, stops, speed and queue behavior.
Chain
Model, measured pitch, roller/pin geometry and condition.
ஓட்டுநர்
Sprocket, shaft, take-up and rail transition.
Project
Quantity, environment, documentation and delivery requirement.
Measure the interfaces that control fit and tracking
For Stops, Locators and Indexing on Pallet Conveyors, start with a dimensioned record of the installed conveyor. Measure several pitches rather than one joint, then add roller or pin geometry, plate dimensions, strand centers and the rail/contact section. At the drive, record sprocket tooth count, bore or shaft arrangement and visible tooth wear. At stations, identify stop faces, locators, transfer gaps and the carrier surfaces that actually touch the conveyor.
Repeat the review with a representative loaded pallet at safe low speed. Watch whether the carrier stays square, whether both strands share the load and whether any symptom begins at the same fixed location. A change tied to one rail joint, stop or sprocket should be corrected at that interface before chain tension or a new chain is used as the remedy. Keep photographs of the measurement reference points with the RFQ so an engineer can reproduce the comparison against the proposed drawing.
Chain geometry
Several-pitch length plus roller, pin, plate and attachment dimensions.
Carrier geometry
Loaded mass, underside supports, datums, center of gravity and stop faces.
Drive geometry
Sprocket, shaft, center distance and available take-up travel.
Fixed locations
Rail joints, transfers, stops and points with recurring wear or impact.
Keep transport stopping separate from precision locating
Identify the face that the conveyor stop contacts and measure its height relative to the rail and carrier center of mass. A stop that catches the pallet too high can pitch the carrier; one that contacts only one side can create yaw and side-load a chain. Record approach speed and the number of carriers that can queue behind the stop.
Where the process needs precise positioning, check the locator or lift-and-locate mechanism independently from the transport stop. Confirm that machining, pressing or test forces are reacted by station structure rather than by free-running rollers or chain attachments. Cycle the locator with representative fixtures and verify that the carrier can re-enter the conveyor without binding.
During commissioning, test single-carrier stops and a full upstream queue. Watch the first restart after release. If the pallet shifts laterally or rebounds, inspect the stop face, guide clearance and station timing before changing the chain selection.
If multiple stops share one conveyor, compare their contact height and release timing with the same carrier. Differences between stations can create inconsistent yaw or rebound even when the chain is unchanged, and those differences should be corrected at the station hardware.

























