Mô tả sản phẩm
Company Profile
-HangZhou CHOHO Industrial Co., Ltd. was founded in 1999. Has become the leader of chain system technology, the first batch of natioal recognized enterprise technology center,national technology innovation demonstration enterprise,and the first A-share listed company in China’s chain drive industry.The securities code is 003033.
-CHOHO has 4 subsidiaries, including testing technology and international trading companies. has 4 factories in HangZhou, Thailand factory, ZheJiang R&D Center and Tokyo R&D Center. In addition, CHOHO ZHangZhoug Industrial zone is expected to be completed & put into operation next year.
-We specialized in producing all kinds of standard chains and special chains, such as Agricultural Chain, Sprocket, Chain Harrow, Tillage Parts,Rice Harvester Chain, GS38 Chain, Roller Chain, Automobile Chain, Motorcycle Chain Industrial Chain and so on.Our partners among world top enterprises, such as LOVOL,JOHN DEERE,NEW HOLLAND, CLASS,AGCO,DEUTZFAHR,HONDA, KUBOTA etc.
Production Capacity Equipment
By 2571,CHOHO has more than 2,700 sets of main production equipment and more than 600 sets of high-precision equipment,With the domestic advanced product laboratory and chain production assembly line, CHOHO has strong research and development and testing capabilities for high-end chain products.
Our Advantages
1. Any inquiry you make will be answered professionally within 6~8 hours.
2. Attaches great importance to product quality and approved by many global quality system certification,such as France, Norway, Germany.
3. Focused on Chain since 1999, have rich experience in Production.
4. High-quality workers,First-class advanced equipment,good quality control,advanced technology.
5. Be Good at Custom-Made Products, provide customized services for customers.
6. Participated in the drafting of 24 national and industrial standards such as chains.As of 2571-Mar, CHOHO has 180 authorized patents.
7. With the responsibility of “Providing high quality chain system with the same service life for the global locomotive industry”, have established a strong R&D team.
CHOHO has a natural brand awareness. As of January 2571, CHOHO has registered the “CHOHO” trademark in more than 60 countries, including the United States, Japan, the United Kingdom, France, Germany, Russia, Spain, Austria, Belgium, Bulgaria, Croatia, Czech Republic, Denmark, Finland, Greece , Hungary, Ireland, Italy, Netherlands, Poland, Portugal, Romania, Ukraine, Sweden, Australia, Algeria, Egypt, Kenya, Morocco, South Korea, Kazakhstan, Mongolia, Syria, Thailand, Pakistan, India, Brazil, Mexico, Colombia, etc.
Product Advantages
Chứng chỉ
CHOHO attaches great importance to product quality and approved by many global quality system certification, such as France, Norway, and Germany. Through the establishment of a sophisticated production management process and quality control system, the entire product process control is achieved. With the introduction of advanced production, processing, and testing equipment, CHOHO has internationally leading full-process quality control capabilities to provide customers with high-quality products.
Choho Provide Chain System Solutions for The Global Top 500 and The Enterprises in Various Fields Top 10!
Broad Customer Channels Market Continues to Develop!
CHOHO has been invited to participate in domestic & international agricultural machinery exhibitions, such as Hannover Messe, Bologna Fair, Canton Fair ,VIV ASIA and so on!
Packaging & Shipping
| Packaging Details: |
Chain+Plastic Bag+Neutral Box+Wooden case+Big Carton+Steel Pallets or Customization |
Câu hỏi thường gặp
1. Bạn là nhà sản xuất hay công ty thương mại?
We are a factory focused on producing and exporting Chain over 23 years,have a professional international trade team.
2. Bạn thường sử dụng hình thức thanh toán nào?
T/T 30% deposit and 70% against document, L/C at sight
3. Thời gian giao hàng của bạn là bao lâu?
Normally 30~45 days.Stock can be shipped immediately.
4. Do you attend any Show?
We attend Hannover show in Germany, EIMA in Italy, CZPT in France, CIAME in China and many other Agricultural machinery shows.
5.Do you offer free samples?
Yes,we can.or you just bear the shipping cost.
6.Is OEM available?
Yes, OEM is available. We have professional designers to help you design.
Shipping Cost:
Estimated freight per unit.
|
To be negotiated
|
| Cách sử dụng: |
Transmission Chain, Conveyor Chain, Dedicated Special Chain, Roller Chain |
| Vật liệu: |
Thép không gỉ |
| Xử lý bề mặt: |
Đánh bóng |
| Mẫu: |
US$ 0/Meter
1 mét (Số lượng đặt hàng tối thiểu)
|
Order Sample
|
| Tùy chỉnh: |
Có sẵn
|
Yêu cầu tùy chỉnh
|
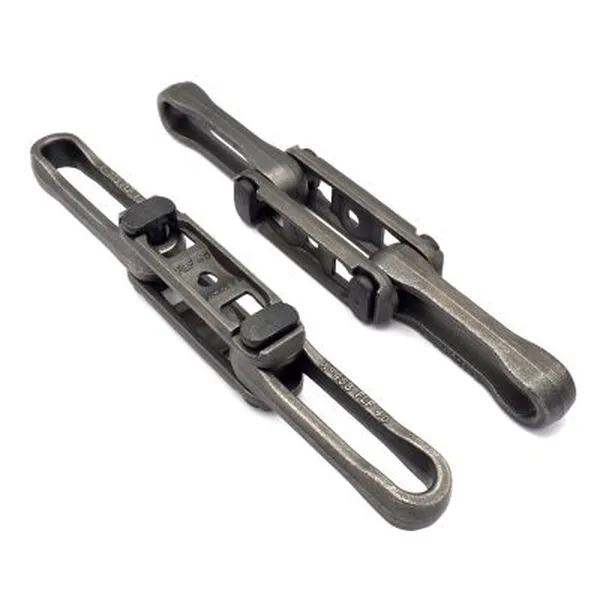
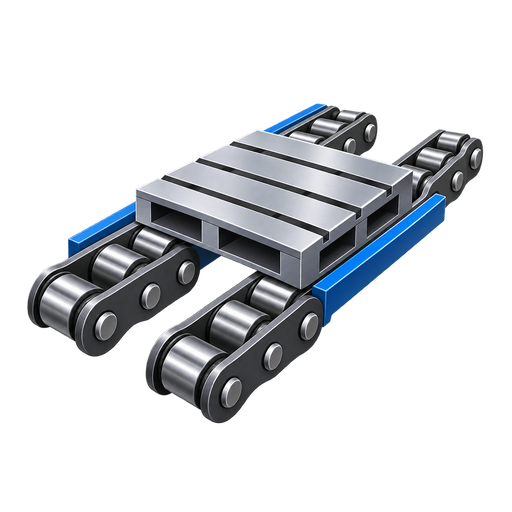
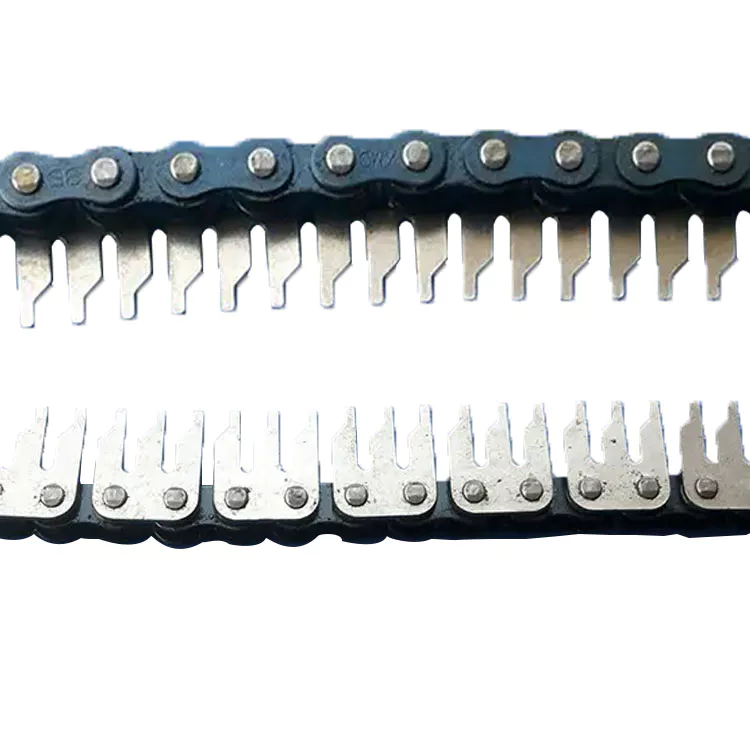
What are the advantages of using a slat conveyor chain?
A slat conveyor chain offers several advantages in material handling and conveying applications. Here are some key benefits:
1. Heavy-Duty Capacity:
– Slat conveyor chains are designed to handle heavy loads and can withstand rigorous industrial environments.
– They are commonly used in applications that require transporting large, bulky, or irregularly shaped items, such as automotive parts, pallets, or containers.
2. Flexibility:
– Slat chains can be customized and configured to suit specific conveying requirements. They are available in various widths, lengths, and chain configurations to accommodate different product sizes and shapes.
– The modular design of slat chains allows for easy modification or expansion of the conveyor system as production needs change.
3. Versatility:
– Slat chains can be used in both horizontal and inclined conveying applications. They are capable of moving products up or down slopes, making them suitable for production lines with varying elevations.
– These chains can be integrated with curves, turns, merges, and diverters to create complex conveying systems that optimize space utilization and product flow.
4. Durability and Longevity:
– Slat chains are typically made from robust materials such as steel or plastic, providing excellent durability and resistance to wear and tear.
– They can withstand demanding operating conditions, including high temperatures, corrosive environments, or exposure to chemicals.
5. Low Maintenance:
– Slat conveyor chains require minimal maintenance compared to other types of conveyor systems. They have fewer moving parts and typically operate with reduced friction.
– With proper lubrication and periodic inspection, slat chains can maintain their performance and reliability over an extended service life.
6. Easy Cleaning:
– The open design of slat chains allows for easy cleaning and debris removal. They are suitable for applications that require frequent sanitation or hygiene maintenance, such as in food processing or pharmaceutical industries.
Overall, using a slat conveyor chain offers the advantages of high load capacity, flexibility in design, versatility in conveying applications, durability, low maintenance requirements, and ease of cleaning. These features make slat chains an effective solution for various industries requiring efficient and reliable material handling.
Can a conveyor chain be used in food processing applications?
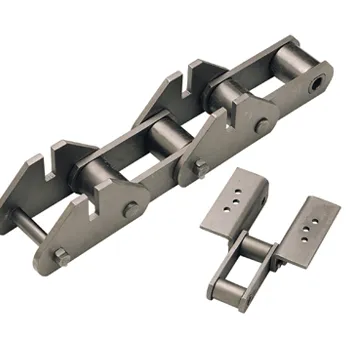
Yes, a conveyor chain can be used in food processing applications. Conveyor chains play a crucial role in the efficient and hygienic handling of food products throughout the production process. Here are some key points to consider:
1. Food-Grade Materials: Conveyor chains used in food processing applications are typically made from food-grade materials such as stainless steel or plastic. These materials are corrosion-resistant, easy to clean, and comply with food safety regulations.
2. Hygiene Considerations: Food processing environments require high standards of hygiene. Conveyor chains designed for food applications incorporate features such as smooth surfaces, open link designs, and easy disassembly for thorough cleaning. They may also have specialized coatings or treatments to prevent bacterial growth.
3. Sanitary Design: Conveyor chains for food processing applications are designed with minimal crevices or joints to prevent food particles from getting trapped. They may have self-draining capabilities to remove excess fluids or debris.
4. Product Integrity: Conveyor chains in food processing applications ensure gentle handling of delicate food products to avoid damage or contamination. They can be equipped with accessories like cleats, side guards, or modular belt systems to securely hold and transport items of various shapes and sizes.
5. High Temperature and Washdown Capabilities: Some food processing applications require conveyor chains to withstand high temperatures during cooking, baking, or sterilization processes. Specialized chains with heat-resistant materials or coatings are available. Additionally, conveyor chains used in food processing should be capable of withstanding frequent washdowns and cleaning with water or cleaning agents.
6. Compliance with Standards: Conveyor chains used in food processing applications must comply with industry-specific standards such as FDA (Food and Drug Administration) regulations, HACCP (Hazard Analysis Critical Control Point) guidelines, and other food safety certifications.
When selecting a conveyor chain for food processing applications, it is important to consider the specific requirements of the production line, including the type of food being handled, the operating conditions, and the necessary sanitary standards. Proper maintenance and regular cleaning protocols should also be implemented to ensure food safety and product integrity.
What are the industry standards and regulations for conveyor chains?
In the field of conveyor chains, there are several industry standards and regulations that help ensure safety, performance, and quality. Some of the commonly recognized standards include:
1. ISO 1977:2013 – Conveyor chains, attachments, and sprockets: This International Organization for Standardization (ISO) standard specifies the requirements and dimensions for various types of conveyor chains, attachments, and sprockets used in general industrial applications.
2. ANSI/ASME B29.1 – Precision Power Transmission Roller Chains, Attachments, and Sprockets: This American National Standard Institute (ANSI) standard provides guidelines for the design, dimensions, and performance of roller chains, attachments, and sprockets used in power transmission systems, including conveyor chains.
3. CEMA – Conveyor Equipment Manufacturers Association: CEMA publishes various standards and technical documents related to conveyor systems, including conveyor chains. These standards cover topics such as safety, design, installation, maintenance, and operation of conveyor equipment.
4. OSHA – Occupational Safety and Health Administration: OSHA is a regulatory agency in the United States that sets and enforces safety standards for workplaces. They have specific regulations related to conveyor systems, including requirements for guarding, maintenance, and employee safety.
5. Local and National Building Codes: Depending on the location and application, there may be specific building codes or regulations that dictate the design, installation, and operation of conveyor chains. These codes ensure compliance with safety and structural requirements.
It’s important for conveyor chain manufacturers, system integrators, and end-users to adhere to these industry standards and regulations to ensure the safe and reliable operation of conveyor systems. Compliance with these standards helps to maintain worker safety, promote system performance, and ensure compatibility and interchangeability of conveyor chain components.
editor by CX 2023-08-18