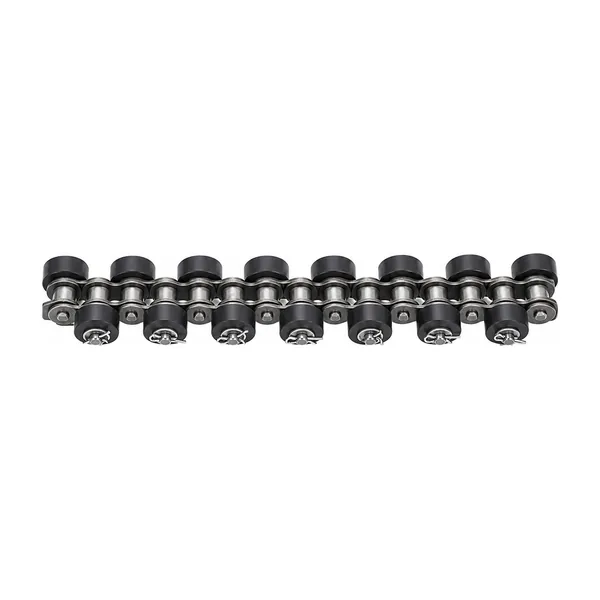
C210A-PSR Double Pitch Polyacetal Side Roller Chain
C210A-PSR Double Pitch Polyacetal Side Roller Chain with 31.75 mm pitch for pallet and workpiece-carrier conveyor layouts. Confirm roller or…

C216AL-PSR Double Pitch Polyacetal Side Roller Chain with 50.8 mm pitch for pallet and workpiece-carrier conveyor layouts. Confirm roller or pin geometry, rail/sprocket interface, environment and quantity before replacement or new-system release.
C216AL-PSR Double Pitch Polyacetal Side Roller Chain should be checked with sprocket pitch, rail contact, carrier underside, strand spacing, drive layout and operating environment. For replacement work, send the installed model, measured pitch, sprocket details and clear side/end photographs. For new equipment, send carrier mass, line speed, carrier count, start/stop sequence and station interfaces.
C216AL-PSR is a large roller double-pitch polyacetal side-roller chain with a specified pitch of 50.8 mm. Double-pitch side-roller layouts are useful when the conveyor architecture calls for a wider pitch spacing while retaining an outboard rolling interface for pallet or carrier support. The model-specific specification table distinguishes the small-roller and large-roller forms, so the product page preserves that variant boundary instead of collapsing the two into one generic product. This entry is currently kept as a draft because the technical data provides dimensions but no clean dedicated product photograph. The dimensional drawing is included for engineering review, and a real matching photograph should be added before public release.
This model is most useful when it is treated as one element of the entire conveyor mechanism, not as an isolated replacement part. For C216AL-PSR, the 50.8 mm pitch is only the first check. The side-roller diameter dt is listed as 28.58 mm and the pin diameter d2 as 7.92 mm. The table also lists a minimum tensile strength of 56.7 kN. Tensile strength is a chain test/property value and should not be used directly as the allowable pallet load, because service load depends on span, number of strands, acceleration, shock, lubrication, rail friction, sprocket geometry and the machine duty cycle. Within the prepared range, C216AL-PSR is at the larger-pitch end of the selected family. The next smaller selected reference is C210A-PSR; moving between them changes several dimensions at the same time, so a replacement decision should not be based on pitch alone. When matching an existing line, the safest route is to compare the complete dimension set and verify the side-roller contact position against the conveyor rail.
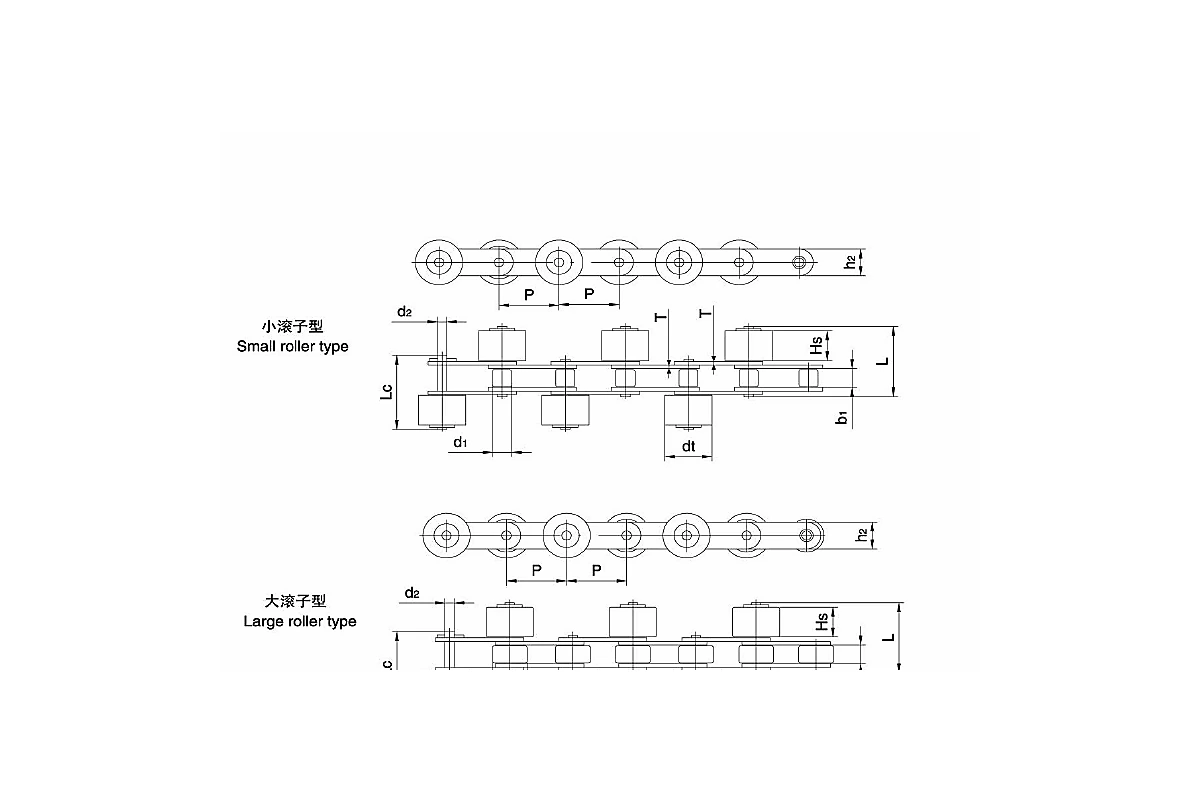
Use this drawing together with the model table. Pitch, roller, pin and plate symbols are meaningful only when matched to the corresponding view.
All numerical values on this page are copied from the model-specific data row in the technical data available for this model. Fields that the technical data does not state are intentionally not filled with estimated values. This entry remains in draft status because a clean real product photograph for the exact/same approved family has not yet been added; the dimensional drawing is included for technical review.
| Parameter | Catalogue value |
|---|---|
| Roller variant | Large roller |
| Pitch P | 50.8 mm |
| Inner width b1 min | 15.75 mm |
| Roller d1 max | — |
| Large roller d3 max | 28.58 mm |
| Side roller dt max | 28.58 mm |
| Side roller offset Hs min | 15.8 mm |
| Pin diameter d2 max | 7.92 mm |
| Pin length L max | 51.1 mm |
| Pin length Lc max | 53.7 mm |
| Plate depth h2 max | 24 mm |
| Plate thickness T max | 3.25 mm |
| Minimum tensile strength Q | 56.7 kN |
Dimensions should be checked against the drawing before a replacement order is released. Symbols such as P, d1, d2, d4, d8, b1, b2, L, Lc, h2, T and t refer to the corresponding catalogue drawing for this chain family.
A pallet conveyor chain has to work with the complete transport path. The chain engages the sprockets, follows the guide or wear rail, supports or drives the carrier through a defined roller interface, and then returns through the lower strand. The pallet or workpiece carrier may also meet stops, locators, lifts, transfers, sensors and process stations. For that reason, a correct chain model can still perform poorly if the rails are misaligned, if the sprocket tooth form does not match the chain, or if the carrier contacts the wrong roller surface.
Current conveyor-system terminology commonly describes pallet transport in terms of workpiece carriers, buffering, positioning, separation, locating stations, stops, merges and transfers. Those functions are system-level features. C216AL-PSR should therefore be selected from its specified geometry first, then checked against the required conveyor function. EVER POWER does not treat a catalogue tensile value or a family description as a substitute for a system calculation.
For a new conveyor, begin with the workpiece carrier and the required production sequence, then work outward to the chain path. For a replacement, begin with the installed chain and measure what is actually on the machine. In both cases, the objective is to remove ambiguity before production or shipment.
When two models look similar in a photograph, use the dimensional table and drawing to separate them. A different pin length, roller diameter or plate depth can be enough to cause interference with a guide, misalignment with a sprocket or incorrect pallet contact. If measurements from the installed chain do not match the table, send those differences with the inquiry rather than forcing the nearest model number.
Chain and sprocket selection should be reviewed together. The sprocket pitch must correspond to the chain pitch, while tooth form, tooth count, bore, hub arrangement and shaft connection belong to the machine design. Reusing an old sprocket without checking its wear condition can shorten the service life of a new chain. Conversely, ordering a new sprocket from only a photograph can create a mismatch at the bore or hub even if the tooth pitch is correct.
The rail side of the system deserves the same attention. Check material, straightness, transitions, joints, return guides and the vertical position of every surface that contacts a roller. Pallet stops and locating devices should stop or locate the carrier without forcing the chain sideways. In multi-strand conveyors, keep the strands aligned and tensioned so one side does not pull the pallet ahead of the other. For longer systems, document the take-up travel and the method used to maintain chain length and tracking.
EVER POWER can quote matching sprockets and chain as a package when the sprocket requirements are provided. The companion sprocket is mentioned here because it is a functional partner to the chain; no bore, tooth count or hub dimensions are assumed from the chain model alone.
During commissioning, check that the chain enters and leaves each sprocket without side loading and that the supporting rails are aligned with the intended roller contact surfaces. Verify that connecting links, retaining parts and any chain-specific attachments are fully seated before the machine is placed into automatic operation. Keep the two sides of a twin-strand conveyor synchronized during installation so the pallet does not enter stations at an angle.
Inspect the side rollers and their rail contact for free rotation, uneven wear and misalignment. If one chain strand carries more of the pallet weight than the other, the root cause may be conveyor frame or rail alignment rather than the chain model itself. Establish an inspection interval from the real duty cycle rather than using one universal schedule. A line that indexes continuously, operates in abrasive contamination or experiences frequent pallet stops may need more frequent checks than a lightly used transfer conveyor. Record elongation, roller condition, unusual noise, hot spots, sprocket wear and any recurring tracking correction so maintenance decisions are based on trend rather than guesswork.
Lubrication practice should follow the chain construction, environment and process restrictions. Avoid applying a lubricant simply because another chain on the same machine uses it. If the conveyor operates near sensitive products, cleaning agents, elevated temperature or a process that restricts oil, state that condition during the RFQ so an appropriate chain and maintenance approach can be discussed.
For an RFQ on C216AL-PSR, send the chain model if known, required quantity or length, destination country, machine application, conveyor speed, pallet or carrier details and any available drawing. Include a rail cross-section or side view showing where the side roller contacts the conveyor structure. If the request is a replacement for an installed chain, photographs of the complete chain, a close-up of one pitch, the sprocket and the rail interface are especially useful. EVER POWER can review the dimensional match and quote chain together with matching sprocket requirements when the sprocket data are available. Where the technical data do not define a property – for example a special material grade, attachment load, permissible working load or a particular coating – that property will be treated as an RFQ confirmation item rather than being assumed from the model family.
For production planning, also state whether you need endless matched lengths, loose chain lengths, connecting links, spare sections or sprockets. If the conveyor uses paired chains, tell us whether matched strand length is required. If a drawing contains tolerances or special interfaces not shown in the technical specification table, attach it to the inquiry. That information is more useful than a broad request for a “pallet conveyor chain” because it lets the quotation stay tied to the machine that will actually use the component.
The specification table lists a pitch P of 50.8 mm for C216AL-PSR. The side-roller location and the other chain dimensions should also be checked against the conveyor rail.
Yes. Sprockets should be matched to the chain pitch and roller/pin geometry, and the bore, hub and tooth-count requirements should be included in the RFQ.
Conveyor speed, carrier load, number of chain strands, start/stop frequency, rail material, lubrication, contamination, temperature and any accumulation or impact at stations should all be described.
The side roller gives the conveyor designer an outboard rolling interface that can support or guide the chain/pallet arrangement on a rail. Its exact role depends on the machine layout.
No. The catalogue lists a minimum tensile strength of 56.7 kN for this model. It is not a safe working-load value and should not be used directly to size the pallet load.
Yes, when the key dimensions and interfaces are verified. Send the chain code, pitch, side-roller diameter and position, rail cross-section, sprocket details and photographs of the installed chain.
Use the model and table on this page as the starting point, then send your conveyor drawing, required quantity or length, destination country and any replacement-chain measurements to [email protected]. For retrofit work, include the sprocket and rail interface so the review covers the complete chain path rather than the chain alone.
Vraag een offerte aan
The working interfaces are the pins, bushings, rollers, side plates and family-specific support features. The rail should support the intended roller surface without forcing side plates to carry track load. Sprockets must belong to the same pitch system and the carrier should contact only the surfaces intended to support it. Misalignment can appear as noise, edge wear, stiff articulation or uneven load sharing between strands.
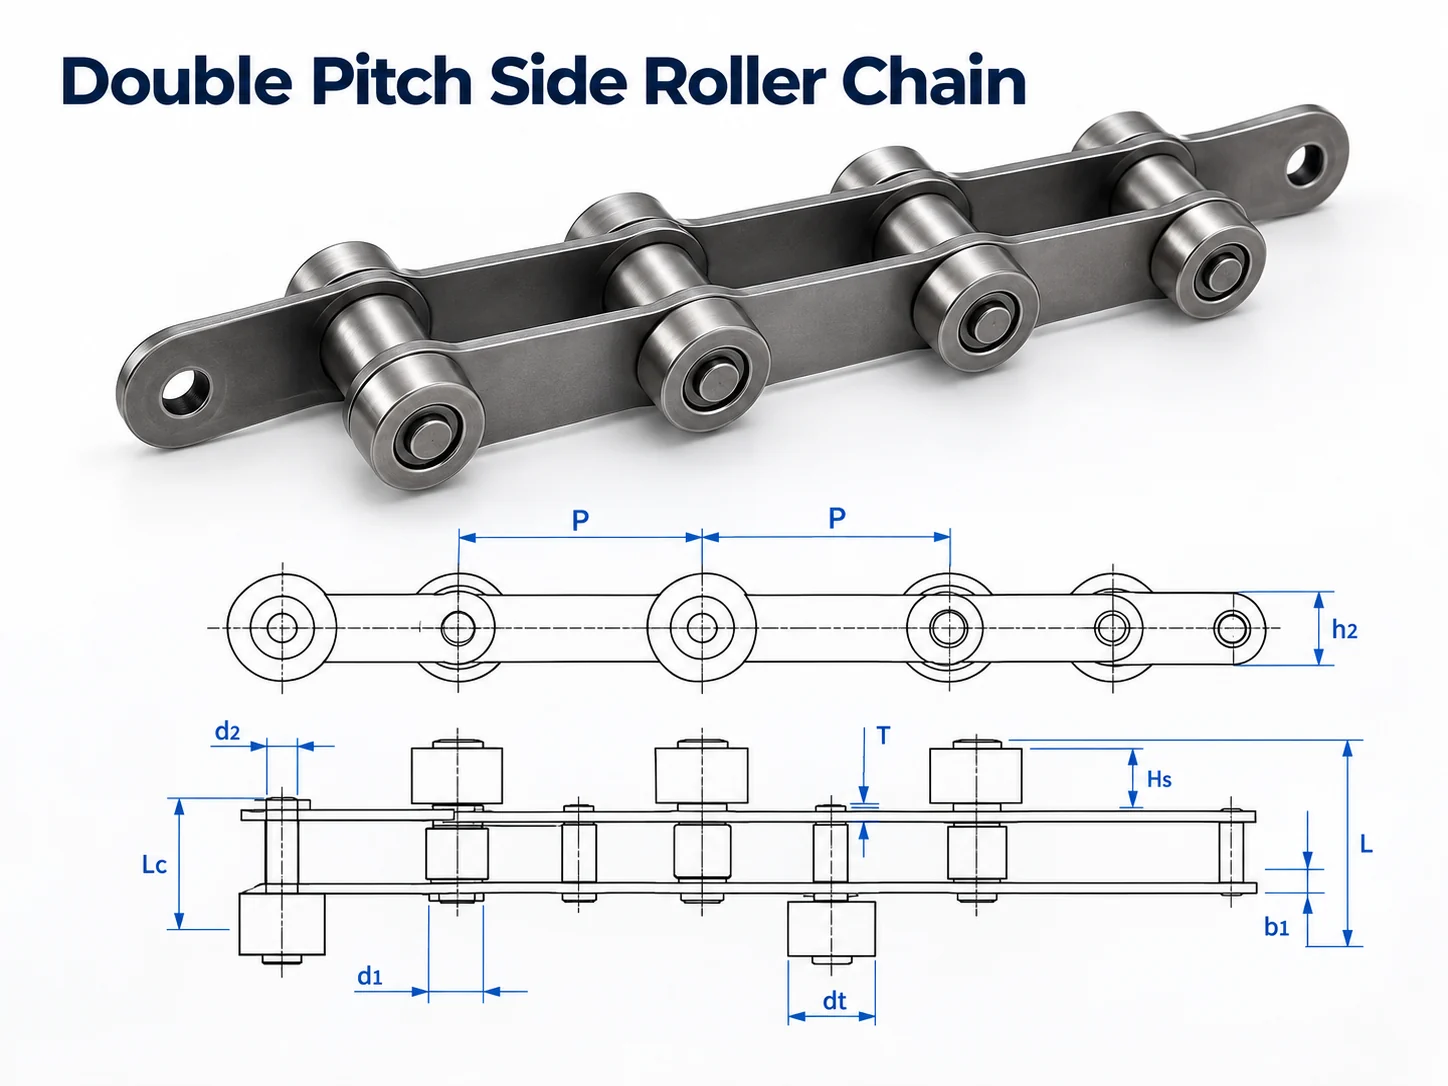
This family is evaluated for palletized assembly, inspection, transfer and buffering where repeatable carrier motion matters. Coordinate stops, lifts, locators, sensors and transfers so process loads are reacted through fixtures rather than becoming unintended chain side loads. Accumulation or free-flow behavior is a system-level result.
Order release should check pitch consistency, roller and pin geometry, plate alignment, articulation, surface condition and the model dimensions that interface with the conveyor. If material certificates, inspection reports or order-specific compliance documents are required, list them in the enquiry before order acceptance.
| MOQ | Set according to product type, production batch and order value; high-value or large items may be evaluated by order value. |
|---|---|
| Samples | Suitable new-customer samples of 1-5 pieces may be discussed at sample pricing. |
| Mixed models | Multiple models can be combined toward approximately USD 1,500. |
| Very small needs | Qualified engineering/sample needs for 1-2 pieces may be evaluated at higher unit cost; routine consumer-style 1-2-piece retail orders are not accepted. |
| Lead-time planning | Standard parts 10-25 working days; customized components 20-45; project equipment 45-120, subject to final production review. |
| Trade terms | EXW, FOB, CIF and DAP are commonly supported; FCA, CFR, CPT, CIP and DDP can be discussed per shipment. |
Compare this model with its product family to check neighboring sizes and configurations. Then use the pallet conveyor engineering workflow to confirm the carrier, rail, sprocket, duty and replacement interfaces before order release.
Reference C216AL-PSR and attach the conveyor drawing or marked photograph showing chain path, sprocket, rail contact and carrier interface. Include quantity, replacement/new-design status, environment, documentation requirements and delivery window. If the code is uncertain, add measured pitch over multiple joints and a side-view photograph.
C210A-PSR Double Pitch Polyacetal Side Roller Chain with 31.75 mm pitch for pallet and workpiece-carrier conveyor layouts. Confirm roller or…

























