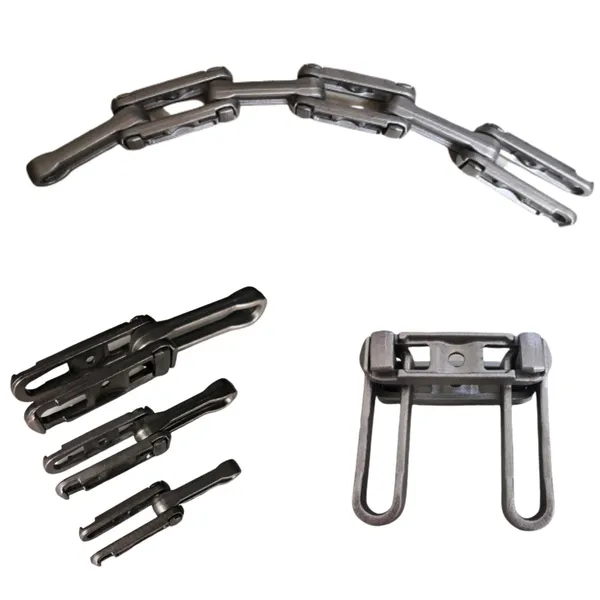
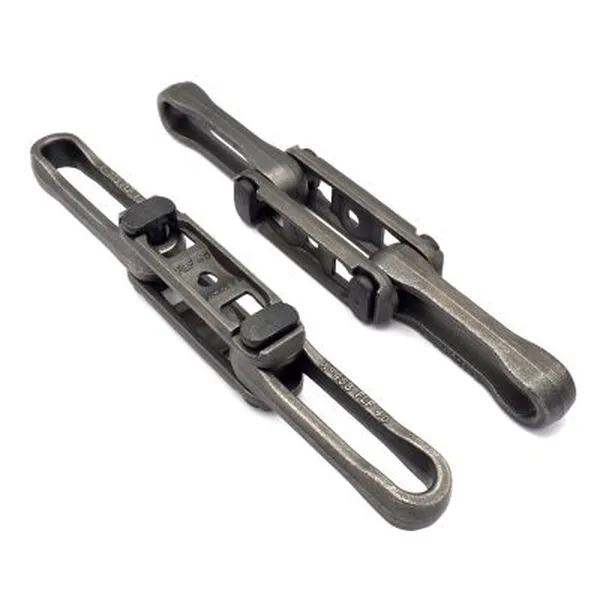
Description du produit

Company Profile

-HangZhou CHOHO Industrial Co., Ltd. was founded in 1999. Has become the leader of chain system technology, the first batch of natioal recognized enterprise technology center,national technology innovation demonstration enterprise,and the first A-share listed company in China’s chain drive industry.The securities code is 003033.
-CHOHO has 4 subsidiaries, including testing technology and international trading companies. has 4 factories in HangZhou, Thailand factory, ZheJiang R&D Center and Tokyo R&D Center. In addition, CHOHO ZHangZhoug Industrial zone is expected to be completed & put into operation next year.
-We specialized in producing all kinds of standard chains and special chains, such as Agricultural Chain, Sprocket, Chain Harrow, Tillage Parts,Rice Harvester Chain, GS38 Chain, Roller Chain, Automobile Chain, Motorcycle Chain Industrial Chain and so on.Our  partners among world top enterprises, such as LOVOL,JOHN DEERE,NEW HOLLAND, CLASS,AGCO,DEUTZFAHR,HONDA, KUBOTA etc.

Production Capacity Equipment

By 2571,CHOHO has more than 2,700 sets of main production equipment and more than 600 sets of high-precision equipment,With the domestic advanced product laboratory and chain production assembly line, CHOHO has strong research and development and testing capabilities for high-end chain products.

Our Advantages

1. Any inquiry you make will be answered professionally within 6~8 hours.
2. Attaches great importance to product quality and approved by many global quality system certification,such as France, Norway, Germany.
3. Focused on Chain since 1999, have rich experience in Production.
4. High-quality workers,First-class advanced equipment,good quality control,advanced technology.
5. Be Good at Custom-Made Products, provide customized services for customers.
6. Participated in the drafting of 24 national and industrial standards such as chains.As of 2571-Mar, CHOHO has 180 authorized patents.
7. With the responsibility of “Providing high quality chain system with the same service life for the global locomotive industry”, have established a strong R&D team.

CHOHO has a natural brand awareness.  As of January 2571, CHOHO has registered the “CHOHO” trademark in more than 60 countries, including the United States, Japan, the United Kingdom, France, Germany, Russia, Spain, Austria, Belgium, Bulgaria, Croatia, Czech Republic, Denmark, Finland, Greece , Hungary, Ireland, Italy, Netherlands, Poland, Portugal, Romania, Ukraine, Sweden, Australia, Algeria, Egypt, Kenya, Morocco, South Korea, Kazakhstan, Mongolia, Syria, Thailand, Pakistan, India, Brazil, Mexico, Colombia, etc. 

Product Advantages

Certifications

CHOHO attaches great importance to product quality and approved by many global quality system certification, such as France, Norway, and Germany. Through the establishment of a sophisticated production management process and quality control system, the entire product process control is achieved. With the introduction of advanced production, processing, and testing equipment, CHOHO has internationally leading full-process quality control capabilities to provide customers with high-quality products.

Choho Provide Chain System Solutions for The Global Top 500 and The Enterprises in Various Fields Top 10!

Broad Customer Channels  Market Continues to Develop!

CHOHO has been invited to participate in domestic & international agricultural machinery exhibitions, such as Hannover Messe, Bologna Fair, Canton Fair ,VIV ASIA and so on!

Packaging & Shipping

Packaging Details: Chain+Plastic Bag+Neutral Box+Wooden case+Big Carton+Steel Pallets or Customization

FAQ

1. Are you manufacturer or trade Company?
    We are a factory focused on producing and exporting Chain over 23 years,have a professional international trade team.
2. What terms of payment you usually use?
    T/T 30% deposit and 70% against document, L/C at sight
3. What is your lead time for your goods?
    Normally 30~45 days.Stock can be shipped immediately.
4. Do you attend any Show?
    We attend Hannover show in Germany, EIMA in Italy, CZPT in France, CIAME in China and many other Agricultural machinery shows.
5.Do you offer free samples?
   Yes,we can.or you just bear the shipping cost.
6.Is OEM available?
    Yes, OEM is available. We have professional designers to help you design.

Shipping Cost:

Estimated freight per unit.


To be negotiated|


Freight Cost Calculator

Usage: Transmission Chain, Conveyor Chain, Dedicated Special Chain, Roller Chain
Matériel: Stainless steel
Traitement de surface : Polishing
Exemples :
US$ 0/Meter
1 mètre (commande minimale)

|

Order Sample

Customization:
Available

|

Customized Request

convoyeur

Can a conveyor chain be used in pharmaceutical manufacturing?

Yes, conveyor chains can be used in pharmaceutical manufacturing for various applications. Conveyor systems play a crucial role in the efficient and safe transportation of pharmaceutical products throughout the manufacturing process. Here are some key considerations when using conveyor chains in pharmaceutical manufacturing:

1. Material Selection:

– Choose conveyor chains made from materials that are suitable for pharmaceutical applications, such as stainless steel or FDA-approved plastic. These materials offer corrosion resistance, cleanliness, and compliance with industry regulations.

2. Cleanliness and Sanitation:

– Ensure that the conveyor chain design allows for easy cleaning and sanitation. Smooth surfaces, minimal crevices, and access for cleaning equipment are important to maintain a hygienic environment.

3. Contamination Control:

– Implement measures to prevent contamination of pharmaceutical products. This includes using chain lubricants that are safe for pharmaceutical applications and implementing proper handling and storage procedures.

4. Product Protection:

– Choose conveyor chain systems that minimize product damage or degradation. This can include utilizing gentle product handling features such as low-friction surfaces, adjustable speed controls, and proper product spacing.

5. Regulatory Compliance:

– Ensure that the conveyor chain system complies with pharmaceutical industry regulations and guidelines, such as Good Manufacturing Practices (GMP) and the requirements of regulatory bodies like the FDA.

6. Integration with Equipment:

– Consider the integration of conveyor chains with other equipment in the pharmaceutical manufacturing process, such as labeling machines, filling machines, and packaging equipment. The conveyor system should provide seamless operation and synchronization with these machines.

By carefully selecting and designing conveyor chains specifically for pharmaceutical manufacturing, it is possible to meet the stringent requirements of the industry in terms of cleanliness, product integrity, and regulatory compliance.

convoyeur

How does lubrication affect the performance of a conveyor chain?

Lubrication plays a crucial role in the performance and longevity of a conveyor chain. Proper lubrication helps to reduce friction, wear, and heat generation, ensuring smooth operation and minimizing the risk of premature failure. Here’s how lubrication affects the performance of a conveyor chain:

1. Friction Reduction: Lubrication forms a thin film between the chain components, reducing friction between metal surfaces. This reduces the energy required for operation, minimizes heat generation, and prevents excessive wear and tear.

2. Wear Prevention: Lubrication forms a protective layer on the chain components, preventing direct metal-to-metal contact. This helps to reduce wear and extend the service life of the chain.

3. Corrosion Protection: Lubricants often contain anti-corrosion additives that protect the chain from rust and oxidation. This is particularly important in environments with high humidity or exposure to corrosive substances.

4. Noise Reduction: Proper lubrication reduces the noise generated during chain operation by minimizing friction and metal-to-metal contact. This can contribute to a quieter and more comfortable working environment.

5. Temperature Control: Lubrication helps to dissipate heat generated during chain operation, preventing excessive temperature rise. This is crucial in high-speed or heavy-duty applications where heat can lead to accelerated wear and reduced chain performance.

6. Maintenance and Service Life: Regular lubrication and proper lubricant selection are essential for maintaining the chain’s performance and extending its service life. Adequate lubrication reduces the need for frequent maintenance, minimizes downtime, and lowers overall operating costs.

It’s important to follow the manufacturer’s recommendations for lubrication frequency and use the appropriate lubricant for the conveyor chain. Regular inspections and maintenance checks should also be conducted to ensure proper lubrication levels and address any issues promptly. Proper lubrication practices will enhance the performance, reliability, and durability of the conveyor chain system.

convoyeur

How can you prevent conveyor chain failures?

Preventing conveyor chain failures is crucial for maintaining the efficiency and reliability of a conveyor system. Here are some key preventive measures:

By implementing these preventive measures, you can significantly reduce the risk of conveyor chain failures and extend the lifespan of the chain. Regular monitoring and maintenance are essential to ensure the system operates smoothly and safely.

China factory Straight Side Plate Conveyor Stainless Steel Precision Short Link Industrial Roller Chain  China factory Straight Side Plate Conveyor Stainless Steel Precision Short Link Industrial Roller Chain
editor by CX 2023-07-21