
توضیحات محصول
توضیحات محصول
| Brand | Chang Xing |
| Material | Metal |
| Size | 60cm/100cm/120cm/Customized Size |
| Features | Durable,customized,Nickel-Free, Lead free |
| Payment method | L/C,T/T,VISA |
| Color | Multiple Color/Customized |
| Process | Die-casting,polishing,plating,packing |
| FOB | HangZhou |
| کاربرد | Handbag,luggage,Garment,Dog tie,Purse,Bag etc. |
| Packing | Bag |
| Delivery period | Around 7-10 days or mostly depend on the specific situation |
| MOQ | 50Pcs |
| Declaration | We provide products with good quality, reasonable price, good after sales service |
High Quality Metal Brass Handbag Chains for Bags Accessories Purse Shoulder Handbag Chain Strap Curb Black Metal Lady Chains Bag
Product information
| Item Name | bag chain |
| Material | Metal |
| Size | 60cm/100cm/120cm/customize |
| MOQ | 50 pcs |
| Color | Silver/Gold/Black |
| کاربرد | Handbag;Luggage;Purse;Wallet;Dog tie etc |
| Package | Packed In Plastic Bag and Carton and Pallet |
| Payment | Trade Assurance, T/T, Paypal |
| OEM | Available |
1. Welcome to contact us, we have a professional team and superior responsibility sincerely for your service.
2. All of our products material is environmental protection material.
3. The most competitive prices.
4. We have the own production capacity power to design intra-industry product.
5. In accordance with your request we could special customized, not only limited colors on display photo
6. All product could laser etched your own logo.
7. Offer good after-sales service.
Product parameters
Product show
Application Scenarios
Packaging & Shipping
سوالات متداول
Q: Do you have in stock?
A: Yes, we have a large number of spot products, all kinds of styles, can greatly save your time, the price is more favorable.
Q: Can I ask for some of your item samples?
A: Yes, we provide free samples.
Q: Can you make customized products?
A: Yes, the size, color, logo can be customized.
Q: Terms of Packing
A: We can customize the packaging according to your needs.
Q: Delivery time
A: Generally, In stock can be shipped within 7-10 days. The specific delivery time depends on the items and the quantity of your order.
Q: Quality under Control
A: We will ensure that each piece meets the quality requirements before delivery,Keep good quality and competitive price always to ensure our customers’ benefits,Aim to do long-time business.
Q: Why do you choose us?
A: 1)More than 10 years of manufacturing experience.
2) provide OEM/ODM services direct factory price.
3)More competitive high quality zero complaint.
4)Use ERP to manage the company.
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Usage: | Transmission Chain, Drag Chain, Conveyor Chain, Dedicated Special Chain |
|---|---|
| Material: | Iron |
| Surface Treatment: | Polishing |
| Feature: | Heat Resistant |
| Chain Size: | 1/2"*3/32" |
| Structure: | Roller Chain |
| Samples: |
US$ 0.01/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
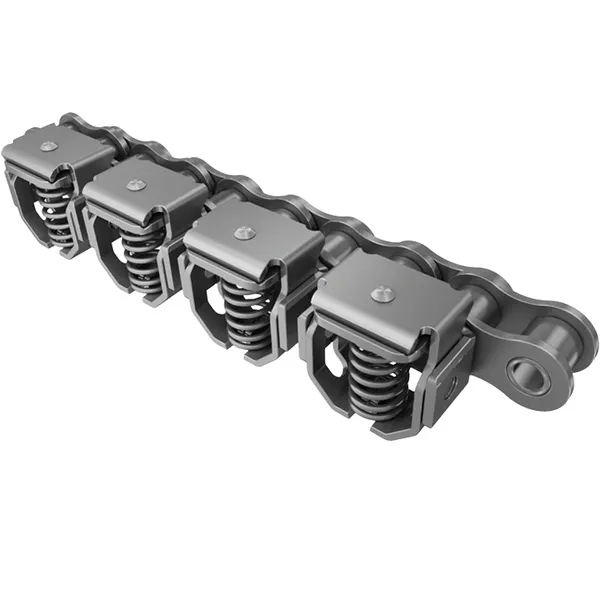
What are the benefits of using an overhead conveyor chain system?
Using an overhead conveyor chain system offers several benefits in various industrial applications. Here are some key advantages:
1. Space Optimization:
– Overhead conveyor chain systems utilize the vertical space, allowing efficient utilization of floor space. This is especially beneficial in facilities with limited floor area, as it enables efficient material handling and production flow without obstructing the work area.
2. Flexibility and Versatility:
– Overhead conveyor chains offer flexibility in routing and can be customized to fit the specific layout requirements of the facility. They can traverse different areas, including assembly lines, paint booths, storage areas, and more. The versatility of overhead systems allows for efficient and adaptable material movement.
3. Improved Safety:
– Overhead conveyor chains minimize ground-level obstructions, reducing the risk of tripping hazards and accidents. Operators and workers can safely navigate the work area without interference from the conveyor system.
4. Product Protection:
– Overhead conveyor chains provide better protection for the products being transported. By keeping the products elevated and away from potential hazards on the floor, such as dust, debris, or spills, the risk of product damage or contamination is reduced.
5. Increased Efficiency:
– Overhead conveyor systems can enhance production efficiency by facilitating continuous material flow and reducing manual handling. They enable automated loading and unloading of materials, leading to faster processing times and improved overall productivity.
6. Easy Maintenance:
– Overhead conveyor chains are typically designed for easy maintenance. Components such as chains, trolleys, and drives can be accessed and serviced conveniently, minimizing downtime and maintenance costs.
7. Customization and Integration:
– Overhead conveyor chains can be tailored to meet specific application requirements, including load capacity, speed, and control systems. They can also be integrated with other automated systems, such as robotic workstations or sorting mechanisms, to further optimize the material handling process.
Overall, using an overhead conveyor chain system provides efficient material handling, maximizes space utilization, enhances safety, and improves productivity in industrial environments.
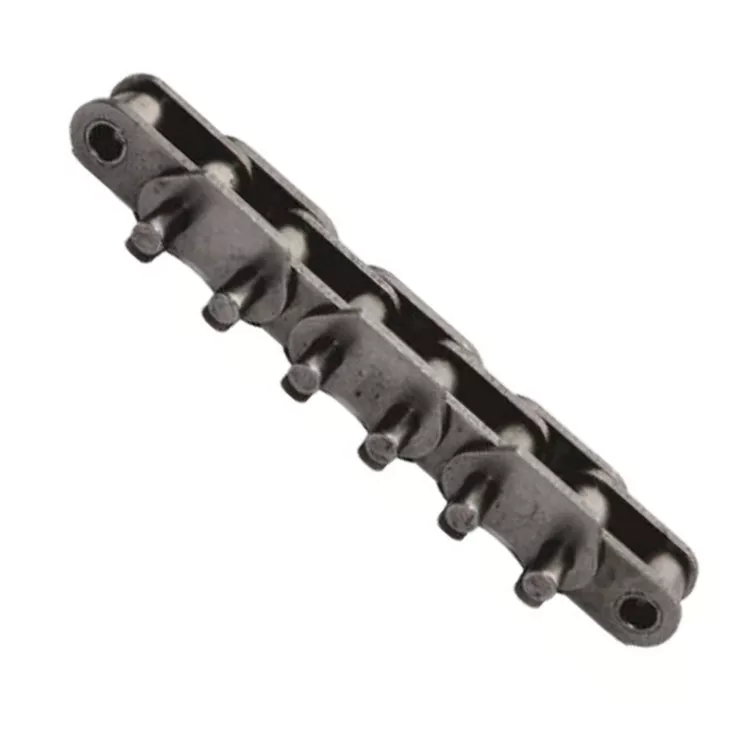
How do you prevent corrosion in conveyor chains?
Preventing corrosion in conveyor chains is essential for maintaining their performance and prolonging their lifespan. Here are some effective measures to prevent corrosion:
1. Material Selection: Choose conveyor chains made from corrosion-resistant materials such as stainless steel, plastic, or coatings specifically designed to resist corrosion. These materials offer better protection against rust and corrosion compared to standard steel chains.
2. Proper Lubrication: Apply a suitable lubricant to the conveyor chain regularly. Lubrication creates a protective barrier that helps prevent moisture and contaminants from reaching the metal surface, reducing the risk of corrosion. Select a lubricant that provides corrosion protection properties and is compatible with the chain material.
3. Environmental Controls: Control the operating environment to minimize exposure to corrosive elements. Implement measures such as humidity control, proper ventilation, and protection from direct contact with water or chemicals. Consider using covers or enclosures to shield the conveyor chain from environmental factors that can accelerate corrosion.
4. Surface Treatments: Apply corrosion-resistant coatings or treatments to the conveyor chain. These coatings can provide an additional protective layer that acts as a barrier against moisture and corrosive substances. Examples of surface treatments include zinc plating, galvanizing, or epoxy coatings.
5. Regular Inspections and Cleaning: Regularly inspect the conveyor chain for signs of corrosion or damage. Remove any accumulated dirt, debris, or corrosive substances promptly. Cleaning the chain helps prevent the buildup of contaminants that can accelerate corrosion.
6. Preventive Maintenance: Implement a preventive maintenance program that includes regular cleaning, lubrication, and inspection of the conveyor chain. This proactive approach helps identify and address any potential corrosion issues early on, preventing further damage.
7. Proper Storage: When not in use, store the conveyor chains in a dry and controlled environment. Protect them from exposure to moisture, humidity, and corrosive substances. Use appropriate storage methods, such as hanging the chains or storing them in sealed containers.
By following these preventive measures, you can significantly reduce the risk of corrosion in conveyor chains, ensuring their optimal performance and longevity.

What are the advantages of using a conveyor chain in material handling?
Conveyor chains offer numerous advantages in material handling applications, making them a preferred choice in various industries. Here are some of the key advantages:
- Efficient Transportation: Conveyor chains provide a continuous and reliable means of transporting materials, ensuring a smooth flow throughout the production or distribution process. They can handle both light and heavy loads, enabling efficient movement of items of different sizes and weights.
- Increased Productivity: By automating the material handling process, conveyor chains help increase productivity and operational efficiency. They eliminate the need for manual handling and reduce human effort, allowing employees to focus on other tasks, resulting in higher throughput and reduced labor costs.
- Flexibility and Customization: Conveyor chains can be designed and configured to meet specific material handling requirements. They are available in various lengths, widths, and configurations, allowing for customization based on the layout and space constraints of the facility. Additionally, different types of conveyor chains can be selected to handle specific materials or accommodate special handling needs.
- Improved Safety: Conveyor chains enhance workplace safety by reducing the risk of manual lifting and carrying heavy loads. They provide a controlled and controlled movement of materials, minimizing the chances of accidents and injuries. Additionally, safety features such as emergency stop buttons, guardrails, and sensors can be incorporated into the conveyor system to further enhance safety.
- Space Optimization: Conveyor chains utilize vertical and horizontal space efficiently, making them ideal for facilities with limited floor space. They can be designed to navigate corners, inclines, and declines, allowing for optimized layout and maximizing the use of available space.
- Versatility: Conveyor chains are versatile and can handle a wide range of materials, including bulk items, packaged goods, fragile items, and irregularly shaped objects. They can accommodate different types of conveyance methods such as flat, inclined, or spiral conveyors, providing flexibility in material handling processes.
- Improved Inventory Control: Conveyor chains enable better inventory control by facilitating the smooth movement and tracking of materials. They can be integrated with barcode scanners, RFID technology, or other tracking systems to monitor the flow of goods and provide real-time information on inventory levels.
- Reduced Material Damage: Conveyor chains help minimize material damage during handling and transportation. They provide a stable and controlled movement, reducing the risk of items falling or getting damaged due to manual handling or rough transportation methods.
The advantages of using a conveyor chain in material handling include improved efficiency, productivity, safety, space utilization, and inventory control, leading to cost savings and enhanced overall operational performance.


editor by CX 2024-03-27

























