توضیحات محصول
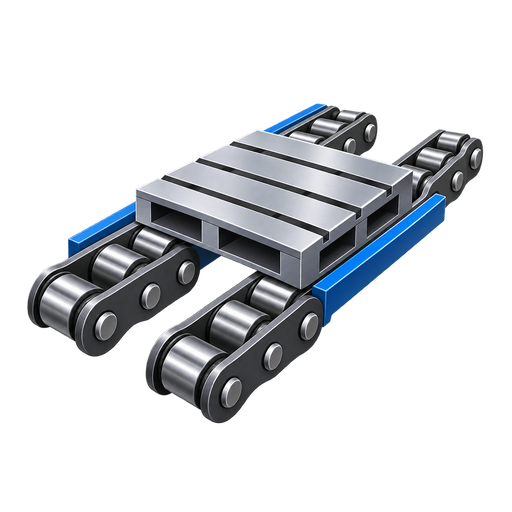
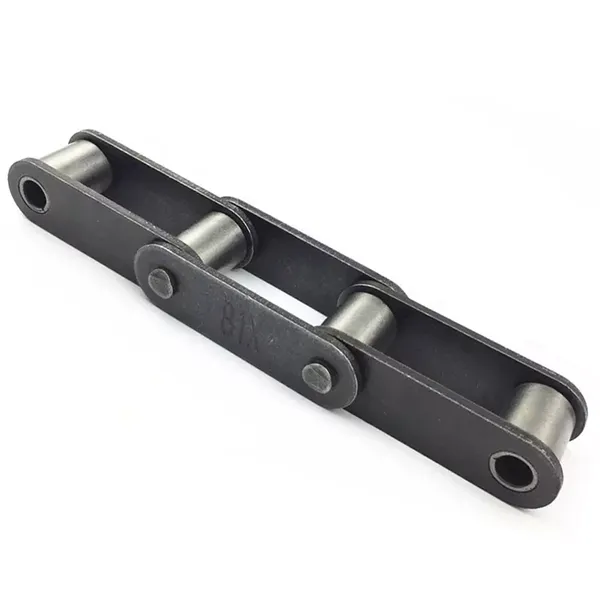
Conveyor Chains (M Series)
Chain No.: M20, M28, M40, M56, M80, M112, M160, M224, M315, M450
Pitch: 40.0mm to 200.0 mm
For Free Samples
Prompt Delivery
Green Product
International Approvals
Experienced Staff
Why choose us?
1. HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd established in 1991, we have 5 subsidiaries in China and also have 6 subsidiaries abroad;
2. We covering a production area of 200, 100 square meters, have more than 1, 800 sets of advanced equipment and over 3, 100 highly skilled employees, the annual production capacity has exceeded 20, 000, 000 meters;
3. We specialized in producing all kinds of standard chains and special chains, such as A or B series chains, driving chains, conveyor chains, dragging chains, agricultural chains and so on;
4. We have obtained ISO9001, ISO14001, ISO16969, AAA and API certificates.
The company is specialized in producing all kinds of standard chains and special chains, E. G. A or B series chains, automobile chains, stainless steel chains, combine harvester chains, heavy-duty cranked link transmission chains, stereo garage chains and maintenance-free chains etc.
In recent years, it invests the capital and depends on the improvement of technology to accelerate the step of new product development and the step of technology reform. It intends to produce high strength and precision chains in order to meet requirements of the domestic and overseas markets. We have enclosed our catalog, which introduces our company in detail and covers the main products we supply at present. You may also visit our online company introduction which includes our latest product line.
Should any of these items be of interest to you, please let us know. We will be happy to give you a quotation CZPT receipt of your detailed requirements.
We look CZPT to receiving your enquires soon.
| طریقه استفاده: | زنجیره انتقال |
|---|---|
| مواد: | Stainless steel |
| درمان سطحی: | پولیش کاری |
| ویژگی: | مقاوم در برابر حرارت |
| اندازه زنجیر: | 1/2"*11/128" |
| ساختار: | زنجیر غلتکی |
| سفارشی سازی: |
موجود است
| درخواست سفارشی |
|---|
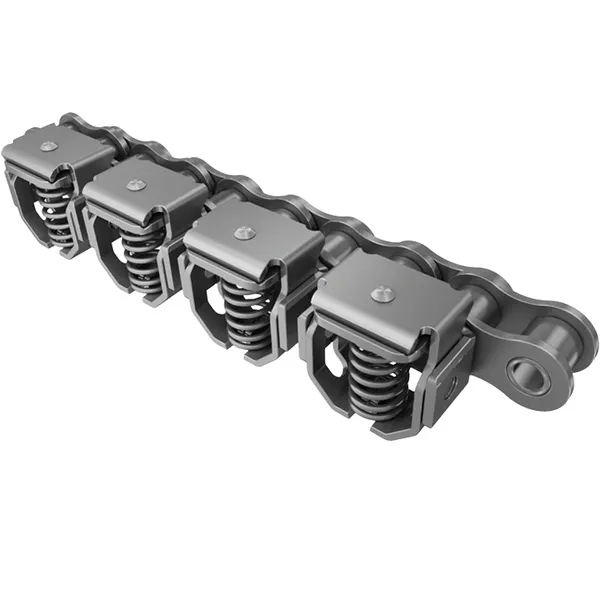
What are the benefits of using a self-lubricating conveyor chain?
Self-lubricating conveyor chains offer several advantages over traditional lubricated chains. Here are some key benefits:
1. Reduced Maintenance: Self-lubricating chains eliminate the need for regular lubrication, reducing the time and effort required for maintenance. This is particularly beneficial in applications where access to the chain is difficult or time-consuming.
2. Cost Savings: By eliminating the need for external lubrication, self-lubricating chains can help reduce lubrication costs over the lifetime of the chain. This includes the cost of lubricants, as well as the labor and equipment required for lubrication maintenance.
3. Clean and Environmentally Friendly: Self-lubricating chains do not require external lubricants, resulting in a cleaner working environment. There is no risk of lubricant spills or contamination of the surrounding area, making them ideal for applications that require strict cleanliness standards, such as food processing or pharmaceutical industries.
4. Extended Chain Life: Self-lubricating chains are designed with built-in lubrication systems that provide a continuous and controlled supply of lubricant to the chain components. This helps reduce friction, wear, and heat generation, resulting in longer chain life and improved performance.
5. Improved Reliability: With consistent and reliable lubrication, self-lubricating chains maintain optimal performance and minimize the risk of chain failure or breakdown. They are less susceptible to premature wear, elongation, and corrosion, ensuring a more reliable and efficient conveyor system.
It’s important to note that the specific benefits of self-lubricating chains may vary depending on the manufacturer and the design of the chain. It’s recommended to consult with the chain manufacturer or an industry expert to understand the suitability and advantages of self-lubricating chains for a particular application.

Can a conveyor chain be used for heavy-duty applications?
Yes, a conveyor chain can be used for heavy-duty applications. Conveyor chains are specifically designed to handle heavy loads and provide reliable transportation in industrial environments.
Here are some factors that make conveyor chains suitable for heavy-duty applications:
1. Robust construction: Conveyor chains are typically made from high-strength materials such as alloy steel, stainless steel, or hardened carbon steel. These materials offer excellent durability and can withstand the heavy loads and harsh operating conditions commonly found in heavy-duty applications.
2. High load-carrying capacity: Conveyor chains are designed to handle significant loads, including heavy products, bulk materials, or large components. The chains are engineered with appropriate pitch, link dimensions, and strength to ensure reliable transport of heavy items.
3. Fatigue resistance: Conveyor chains are built to withstand repetitive stress and fatigue caused by continuous operation under heavy loads. They undergo specific heat treatments and surface hardening processes to enhance their resistance to wear, fatigue, and deformation.
4. Customization options: Conveyor chains can be customized to meet the specific requirements of heavy-duty applications. This includes selecting the appropriate chain type, pitch, attachment design, and surface coating for improved performance and longevity.
5. Compatibility with heavy-duty equipment: Conveyor chains are designed to integrate seamlessly with heavy-duty conveyor systems, including large motors, drives, and supporting structures. This ensures proper power transmission and smooth operation even in demanding environments.
6. Safety features: Conveyor chains for heavy-duty applications often incorporate safety features such as overload protection, emergency stops, and monitoring systems to ensure the safety of operators and prevent damage to the equipment.
It’s important to consult with a qualified engineer or conveyor manufacturer to select the appropriate conveyor chain and system components for the specific heavy-duty application. They can provide guidance on chain selection, system design, and maintenance practices to ensure optimal performance and reliability.
What industries commonly use conveyor chains?
Conveyor chains are widely used in various industries for efficient material handling and transportation. Here are some of the industries commonly using conveyor chains:
- Manufacturing: Conveyor chains are extensively used in manufacturing industries such as automotive, electronics, appliances, and machinery. They facilitate the movement of components, parts, and finished products along assembly lines.
- Food and Beverage: The food and beverage industry relies heavily on conveyor chains for conveying and processing food products, including packaging, sorting, and distribution. Conveyor chains in this industry often have specific requirements such as sanitary design and resistance to contaminants.
- Logistics and Warehousing: Conveyor chains are integral to logistics and warehousing operations for efficient handling of goods, including sorting, loading, unloading, and distribution. They are commonly used in distribution centers, airports, and postal facilities.
- Mining and Quarrying: Conveyor chains play a crucial role in mining and quarrying operations by transporting bulk materials such as coal, ore, gravel, and aggregates. They are designed to withstand heavy loads and harsh environments.
- Agriculture: In the agricultural sector, conveyor chains are used for handling crops, grains, seeds, and livestock feed. They are employed in processing plants, grain elevators, and animal feed production facilities.
- Automotive: The automotive industry extensively uses conveyor chains in assembly plants for transporting vehicle components, body frames, engines, and other parts throughout the production process.
- Pharmaceutical and Healthcare: Conveyor chains are utilized in pharmaceutical and healthcare facilities for the automated movement of medical supplies, pharmaceutical products, and laboratory specimens.
- Chemical and Petrochemical: Conveyor chains are employed in chemical and petrochemical industries for the handling of hazardous materials, bulk chemicals, and raw materials during production and storage.
- Construction and Building Materials: Conveyor chains are used in construction sites and building material production facilities for conveying materials such as cement, bricks, aggregates, and roofing materials.
These are just a few examples, and conveyor chains are also utilized in many other industries where efficient material handling and transportation are essential for the production and distribution processes.
editor by CX 2023-09-06