Chain Tension and Take-Up on Pallet Conveyors
Practical engineering guide: Chain Tension and Take-Up on Pallet Conveyors. Selection, interfaces, application checks, maintenance and RFQ inputs.
This guide focuses on how take-up travel manages installation, wear and chain engagement without using excessive tension. It is written for machine builders, maintenance teams and buyers who need a chain selection that can be checked against drawings and the real conveyor rather than a generic product label.
Chain Tension and Take-Up on Pallet Conveyors
Many conveyor problems begin when a correct catalogue component is installed into an interface that was never checked in detail. In a typical project such as a long conveyor with drive and take-up stations at opposite ends, chain pitch, roller contact, rail alignment, sprocket engagement, carrier stiffness, stops and maintenance access all influence the result. A useful engineering review therefore combines model-level data with the operating sequence of the machine.
Warum dieses Thema wichtig ist
How take-up travel manages installation, wear and chain engagement without using excessive tension affects more than catalogue selection. It changes how the workpiece carrier enters a station, how loads pass into guide rails, how the chain approaches the drive and how the system behaves during stopping or accumulation. If one interface is ignored, the symptom may appear somewhere else: a roller can wear because a rail joint is high, a chain can pull sideways because a pallet stop is offset, or a new chain can run badly because the old sprocket is worn.
The practical objective is not to eliminate every variation in the machine. It is to identify the variables that must be controlled, define which dimensions are fixed by the chain source, and leave unsupported items for explicit RFQ confirmation. This is also why tightening the chain until it has no designed slack is a risky shortcut. It replaces measurable machine data with an assumption and can make a correct-looking part fail at installation.
Vier Prüfungen zur Definition von ersten
Take-Up Range
Record tooth count or drive geometry, shaft alignment, take-up position and the way the chain enters and leaves the drive.
Sprocket Wrap
Record tooth count or drive geometry, shaft alignment, take-up position and the way the chain enters and leaves the drive.
Return Support
State the measurable condition, installed interface and acceptance check that apply to this part of the conveyor.
Thermal/Length Changes
State the measurable condition, installed interface and acceptance check that apply to this part of the conveyor.
Beginnen Sie mit der exakten Kettengeometrie.
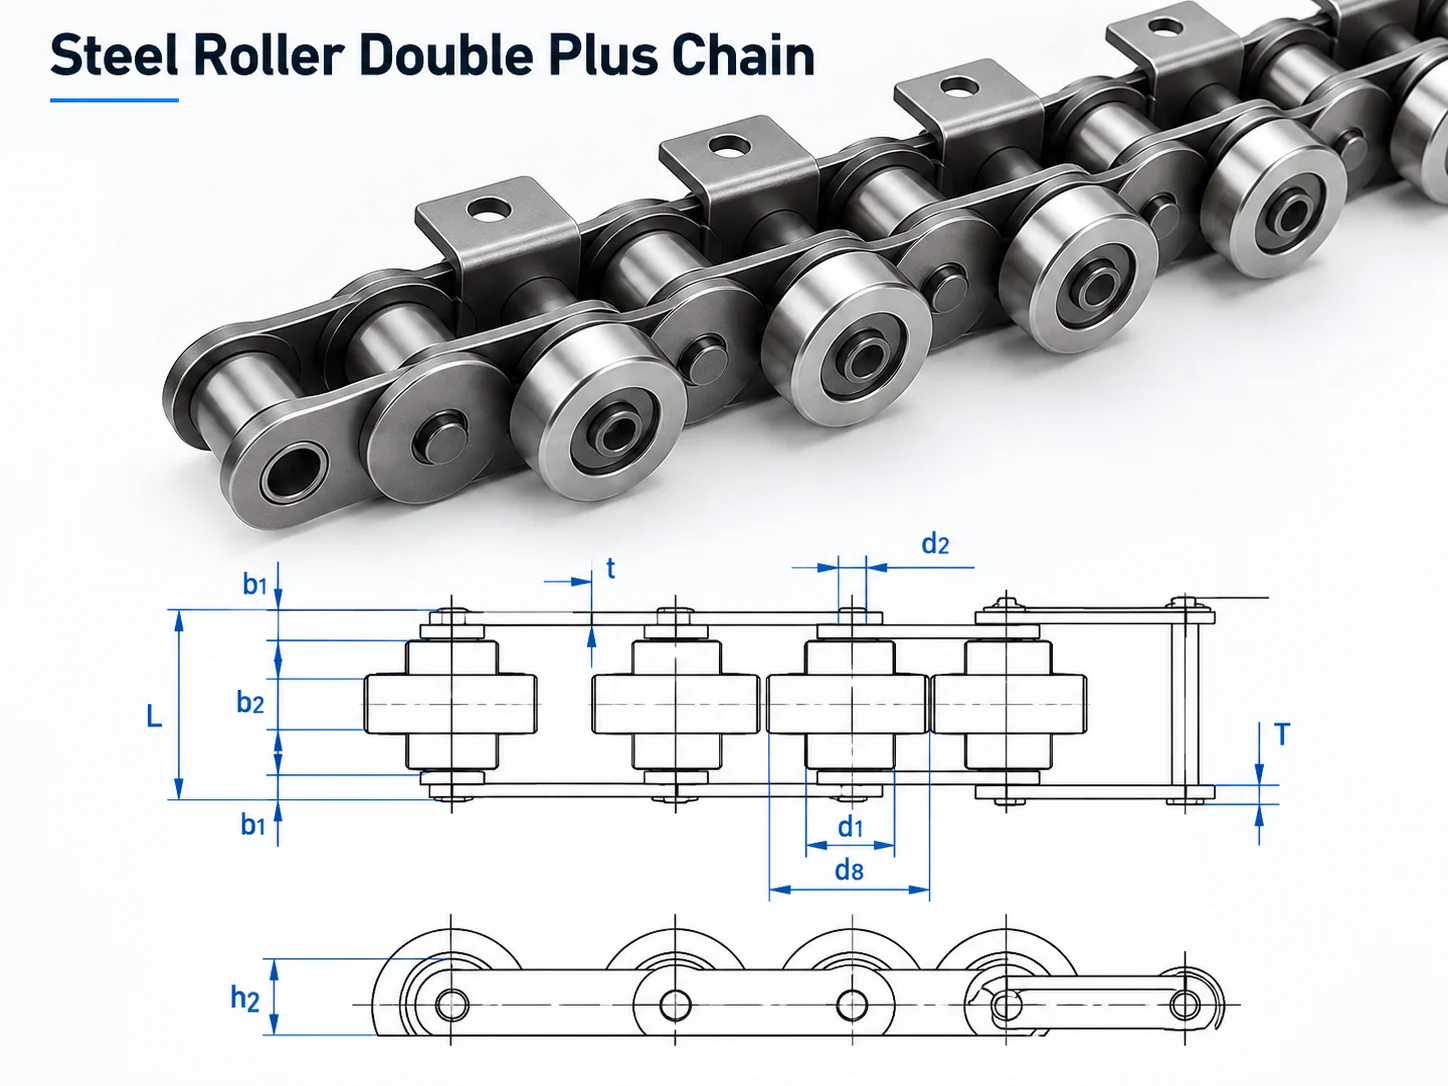
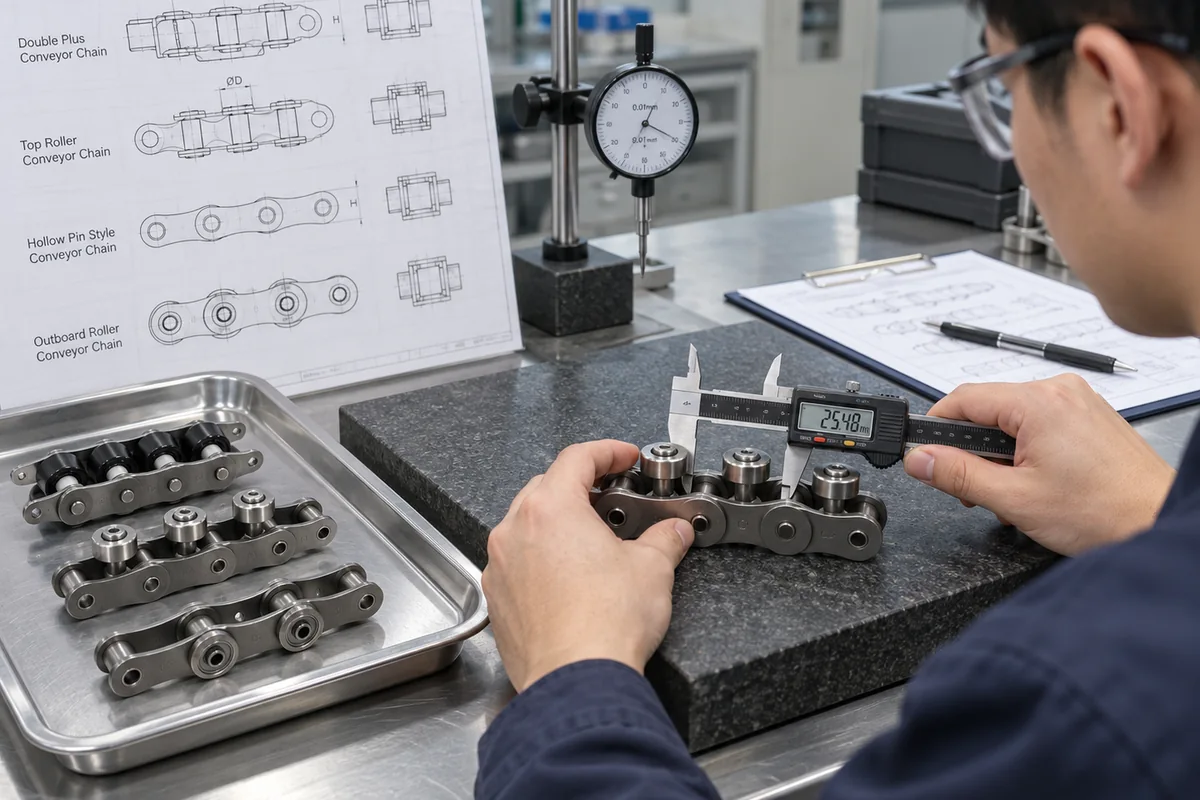
Wenn eine Modellnummer verfügbar ist, verwenden Sie die exakte Modellspezifikation und die zugehörige Zeichnung. Vergleichen Sie Teilung, Rollendurchmesser, Innenbreite, Bolzendurchmesser und -länge, Plattenhöhe und -dicke sowie alle Abmessungen von Seitenrollen, Großrollen oder Hohlbolzen, die mit dem Förderer in Kontakt stehen. Ist der Code unbekannt, messen Sie die installierte Kette systematisch. Die Messung der Teilung über mehrere Bolzen ist zuverlässiger als die Messung eines einzelnen verschlissenen Spalts. Fotos sollten das Seitenprofil, die Rollenanordnung sowie den Kontakt von Kettenrad und Schiene zeigen.
Do not use tensile strength as the pallet payload. Catalogue tensile figures are material/component test properties. Conveyor working conditions also involve line length, the number of chain strands, carrier count, acceleration, shock, friction, lubrication, sprocket size, wear state and the required safety factor. The chain can only be verified for a system after those conditions are understood.
Auswahl-Workflow
- Take-Up Range: Vergleichen Sie die geforderten Bedingungen mit der genauen Kettenzeichnung oder dem Systemlayout und notieren Sie alle offenen Fragen zur Bestätigung der Angebotsanfrage.
- Sprocket Wrap: Vergleichen Sie die geforderten Bedingungen mit der genauen Kettenzeichnung oder dem Systemlayout und notieren Sie alle offenen Fragen zur Bestätigung der Angebotsanfrage.
- Return Support: Vergleichen Sie die geforderten Bedingungen mit der genauen Kettenzeichnung oder dem Systemlayout und notieren Sie alle offenen Fragen zur Bestätigung der Angebotsanfrage.
- Thermal/Length Changes: Vergleichen Sie die geforderten Bedingungen mit der genauen Kettenzeichnung oder dem Systemlayout und notieren Sie alle offenen Fragen zur Bestätigung der Angebotsanfrage.
- Spediteur und Dienst: Erfasst werden die Masse des beladenen Förderers, die Anzahl der Förderer, die Liniengeschwindigkeit, die Starts pro Stunde, das Staumuster sowie etwaige Steigungen oder vertikale Übergänge.
- Hin- und Rückfahrt: Überprüfen Sie die Daten des Kettenrads, die Wellenausrichtung, den Spannbereich, die Rücklaufunterstützung und den Schmierzugang.
- Freigabebedingungen: Alle Felder, die in den technischen Daten nicht angegeben sind – wie z. B. eine spezielle Materialgüte, Beschichtung, zulässige Systemlast oder Umweltklasse – sollten als RFQ-Bestätigungspunkt aufgeführt werden, anstatt sie zu schätzen.
Systemintegration
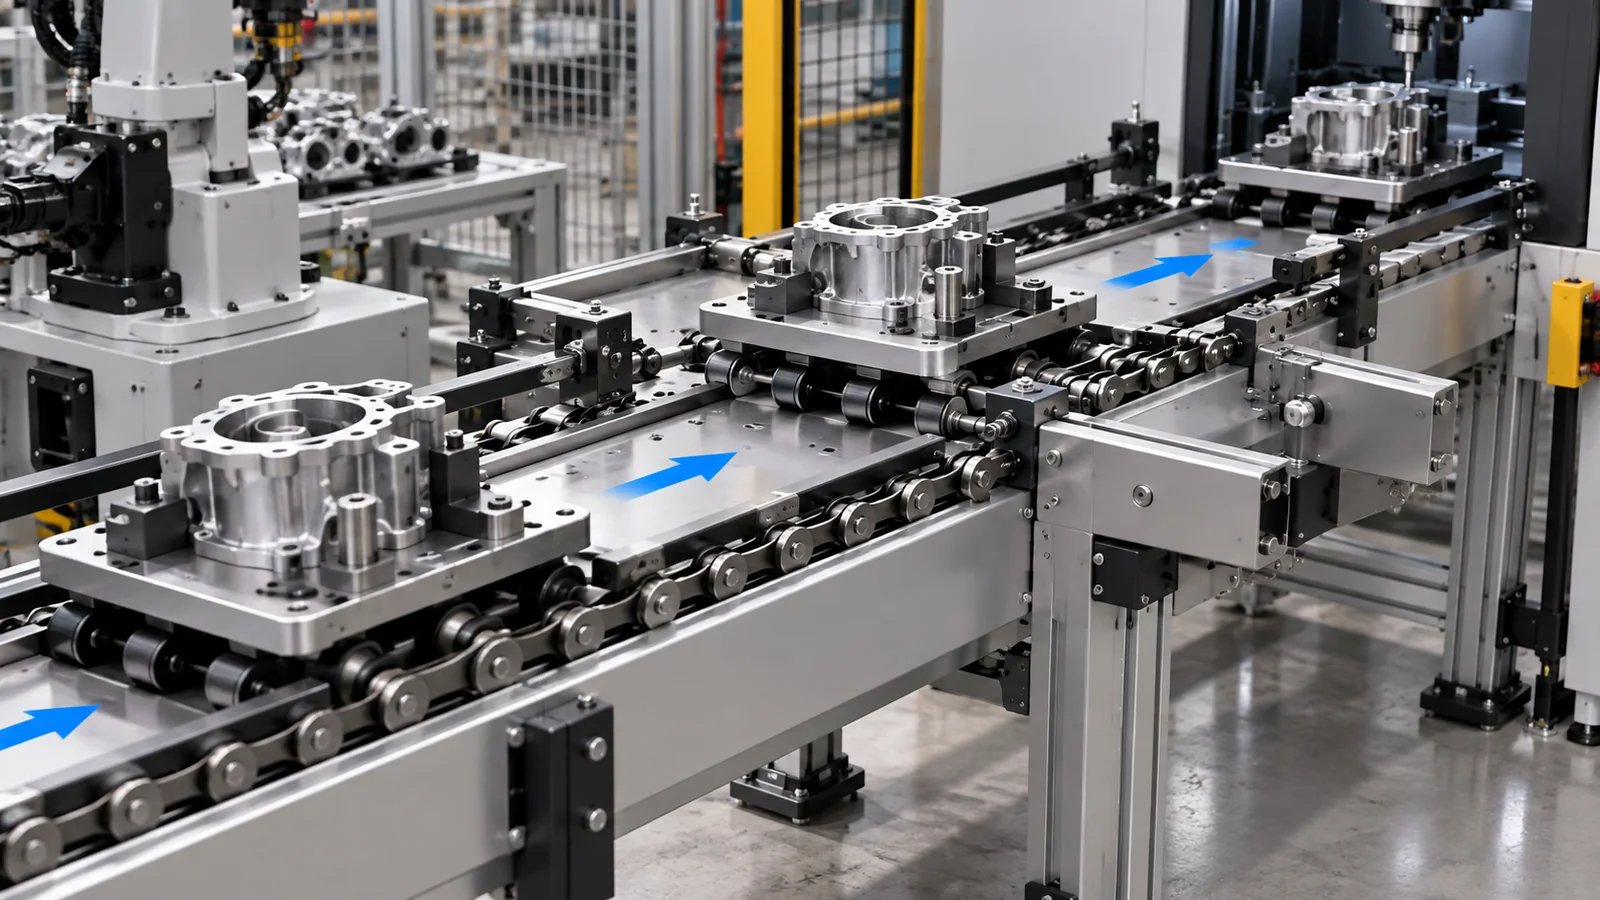
Sobald die Förderkette identifiziert ist, prüfen Sie, wie die Last vom Förderband in die restliche Maschine übertragen wird. Die Führungsschiene bzw. Verschleißschiene muss die vorgesehene Rollenoberfläche stützen und an den Verbindungsstellen durchgehend sein. Parallele Kettenstränge müssen den vorgegebenen Achsabstand und die synchronisierte Antriebstaktung aufweisen. Anschläge müssen an der vorgesehenen Palettenfläche und nicht an der Kettenseitenplatte anliegen. Querübergaben und Hubvorgänge benötigen ausreichende Unterstützung, damit der Träger nicht in eine Lücke gerät oder auf einer Bolzen-/Plattenkante aufsetzt.
Bei Systemen mit Materialstau müssen Transport und Stopp getrennt werden. Die Kette kann sich weiterbewegen, während der Träger angehalten wird; Stoppkraft, Warteschlangenlänge, Wiederanlaufsequenz und lokale Reibung müssen jedoch weiterhin überprüft werden. Bei Systemen, die ein Werkstück für die Bearbeitung positionieren, sollten spezielle Positionierelemente verwendet werden, wenn die erforderliche Wiederholgenauigkeit über den Rahmen des normalen Förderbandtransports hinausgeht.
Inbetriebnahme und Instandhaltung
Nehmen Sie ein neues oder repariertes Förderband zunächst mit niedriger Geschwindigkeit in Betrieb. Führen Sie mehrere vollständige Kettenumläufe durch und beobachten Sie dabei Antrieb, Rücklauf, Schienenübergänge, Stopps und Materialübergaben. Achten Sie auf Geräusche, die sich einmal pro Kettenumdrehung oder Kettenradumdrehung wiederholen, da diese Muster Hinweise auf schwergängige Verbindungen, beschädigte Rollen, lokale Schienenstufen oder Probleme mit den Kettenrädern geben. Bei starren Werkstückpaletten ist auf Schräglagen zwischen parallelen Strängen zu achten; selbst geringe Timing-Unterschiede können zu einseitiger Belastung des Förderers führen.
Die Instandhaltung sollte Trends verfolgen, anstatt auf einen Ausfall zu warten. Längen- und Dehnungsmessungen sind gemäß der zugelassenen Methode zu dokumentieren. Die Rollen sind auf freie Drehung und ungewöhnliche Abflachungen zu prüfen. Polierte Seitenkontaktspuren, die auf eine Fehlausrichtung hindeuten, sind zu erkennen. Die Kettenradzähne sind zu prüfen und die Spannposition zu verifizieren. Die Schmierintervalle sollten sich nach den Betriebsbedingungen und den Empfehlungen des Kettenherstellers richten; mehr Schmierstoff ist nicht automatisch besser, wenn er abrasive Verunreinigungen anzieht oder in einen Prozessbereich gelangt.
Checkliste für Angebotsanfragen
Für eine Ersatzteilanfrage senden Sie bitte, falls lesbar, die Modellbezeichnung, die gemessene Teilung, die Rollenanordnung, die Kettenbreite, die Plattenhöhe, die Bolzenabmessungen, ein Foto des Seitenprofils und ein Foto, das den Kontakt zwischen Kettenrad und Schiene zeigt. Für eine neue Anlage benötigen wir zusätzlich die Förderbandlänge, die Trägergröße und die Ladungsmasse, die Anzahl der Litzen, den Litzenabstand, die Geschwindigkeit, die Start-/Stopp-Zeiten, die Pufferlänge, die Umgebungsbedingungen und das Zielland. Diese Angaben ermöglichen es, die Kettenanpassung von der Berechnung der Gesamtförderleistung zu trennen.
Use take-up to control slack, not to force alignment
Take-up should provide the travel needed for installation, wear and thermal or length changes without turning the chain into a tightly stretched belt. Excess tension can increase bearing and rail loads while doing little to correct misalignment.
Check the drive/return arrangement, available take-up travel, strand balance and return support. On paired chains, compare take-up position on both sides and investigate unequal movement before compensating with extra tension.
Measure the interface
Use several-pitch dimensions, end-view geometry and sprocket/rail details when a replacement must fit an existing machine.
Describe the duty
Include loaded carrier mass, speed, starts, accumulation or indexing behavior and the operating environment.
Test the worst case
Commission with representative carriers and the most demanding queue, stop, transfer or restart condition rather than only no-load travel.
Keep open items explicit
If a material, coating, special tolerance, documentation need or allowable system load is not stated, confirm it in the enquiry.
Häufig gestellte Fragen
Kann ich einen Ersatz nur anhand der Tonhöhe auswählen?
For chain tension and take-up on pallet conveyors, pitch is only the first filter. Confirm roller geometry, inner width, pins, plates and any side-roller or hollow-pin features against the installed conveyor before treating two chains as interchangeable.
Bedeutet ein höherer Zugfestigkeitswert, dass ich diese Last auf der Palette tragen kann?
For chain tension and take-up on pallet conveyors, do not convert tensile strength directly into pallet payload. Service load depends on strand count, friction, acceleration, stop impact, sprockets, rails and the safety margin used for the machine.
Kann ein repräsentatives Familienfoto das genaue Modell beweisen?
Nein. Ein repräsentatives Familienbild kann zwar zur Erläuterung der Konstruktion beitragen, die Modellidentität und die Abmessungen müssen jedoch aus der modellspezifischen technischen Spezifikation, der Zeichnung oder den bestätigten Fertigungsdaten stammen.
Welche Informationen beschleunigen die Angebotserstellung?
For an RFQ related to chain tension and take-up on pallet conveyors, send the model code or dimensional sketch, clear photographs, conveyor layout, loaded carrier information, quantity and delivery country so the review starts from reproducible machine data.
Key engineering variables for Chain Tension and Take-Up on Pallet Conveyors
Die Entscheidung sollte auf messbaren Maschinenparametern und der genauen Kettenzeichnung basieren, nicht auf einer allgemeinen Produktbezeichnung. Beschreiben Sie den Betriebsvorgang in einer Zeile: Was transportiert das Förderband? Wie schnell läuft es? Wo hält es an? Welche Bedingung hat die Überprüfung ausgelöst? Erfassen Sie Maße und Beobachtungen, die ein anderer Techniker nachvollziehen kann.
| Eingang | Was aufgezeichnet werden soll | Warum es wichtig ist |
|---|---|---|
| Träger/Ladung | Beladene Masse, Schwerpunkt, Unterseitenkontakt und Trägeranzahl | Unterstützung, Reibung und Stoppverhalten |
| Bewegung | Geschwindigkeit, Starts, Stopps, Akkumulation und Indexierung | Dynamische Nachfrage und Prozesszeitplanung |
| Kettenpfad | Teilung, Rollen, Litzenabstand und Schienen | Mechanische Passform und Nachführung |
| Fahren | Kettenradzähne, Ausrichtung, Spann- und Antriebsposition | Engagement und Spannungsverteilung |
| Umfeld | Grenzwerte für Temperatur, Staub, Feuchtigkeit, Reinigung und Schmierung | Material- und Wartungsoptionen |
Related product and selection resources
Verwenden Sie die Katalog für Palettenförderketten um Familien und die Auswahlprozess für Ingenieure when machine data is incomplete. For adjacent component context, see chain tensioner placement guidance.
What to include with an enquiry about Chain Tension and Take-Up on Pallet Conveyors
Geben Sie die installierte oder geplante Kettenfamilie, die Anzahl, die Anwendung, das Träger-/Lastsystem, die wichtigsten Abmessungen und die Betriebsbedingungen an, die das neue Bauteil erfüllen muss. Fügen Sie Fotos oder Zeichnungen bei, wenn die geltenden Normen unklar sind, und halten Sie offene Material-, Dokumentations- oder Lieferanforderungen offen.
Turn symptoms into measured maintenance data
Maintenance decisions become more reliable when the same points are measured at each inspection. Mark a repeatable chain section, measure elongation over several pitches, record take-up position and inspect the corresponding sprocket teeth and rail contact. Note whether wear is even on both strands, whether rollers rotate freely and whether the carrier tracks centrally through transfers. For noise or vibration complaints, record the operating state when the symptom occurs: empty running, loaded transfer, accumulation, restart or a specific station. That separates chain wear from alignment, transfer impact, loose guarding or a damaged carrier. Lubrication changes should be tied to the chain construction and environment rather than used as a universal response to noise.
Measure
Several-pitch elongation, roller rotation, take-up position and strand-to-strand difference.
Inspect
Sprocket tooth profile, rail wear, transfer impact points, fasteners and carrier underside contact.
Record
Operating state, load, queue condition, temperature/contamination and the exact location of the symptom.
Decide
Correct alignment or interface faults before replacing chain solely because a symptom is present.
Set take-up travel from the complete conveyor layout
Take-up should control slack without forcing the chain to run as if it were a belt. Review the full chain path, drive location, return support, transfer points and expected wear adjustment range before setting the take-up. A setting that looks acceptable while the conveyor is empty can become unsuitable after carriers accumulate or after the chain reaches operating temperature.
Commission in stages: run empty at low speed, add representative carriers, exercise normal stop and accumulation sequences, and observe the slack side near the drive and take-up. Record the final reference position so later maintenance teams can distinguish normal adjustment from a rapid change that may indicate wear, alignment problems or a damaged component.
Measure the interfaces that control fit and tracking
For Chain Tension and Take-Up on Pallet Conveyors, start with a dimensioned record of the installed conveyor. Measure several pitches rather than one joint, then add roller or pin geometry, plate dimensions, strand centers and the rail/contact section. At the drive, record sprocket tooth count, bore or shaft arrangement and visible tooth wear. At stations, identify stop faces, locators, transfer gaps and the carrier surfaces that actually touch the conveyor.
Repeat the review with a representative loaded pallet at safe low speed. Watch whether the carrier stays square, whether both strands share the load and whether any symptom begins at the same fixed location. A change tied to one rail joint, stop or sprocket should be corrected at that interface before chain tension or a new chain is used as the remedy. Keep photographs of the measurement reference points with the RFQ so an engineer can reproduce the comparison against the proposed drawing.
Chain geometry
Several-pitch length plus roller, pin, plate and attachment dimensions.
Carrier geometry
Loaded mass, underside supports, datums, center of gravity and stop faces.
Drive geometry
Sprocket, shaft, center distance and available take-up travel.
Fixed locations
Rail joints, transfers, stops and points with recurring wear or impact.
Use take-up position as a diagnostic measurement
Record the take-up position on both sides of a paired conveyor and note the available remaining travel. Compare the reading over time rather than tightening until the chain “feels” taut. Conveyor chain needs controlled slack for articulation and sprocket entry; treating it like a stretched belt can increase bearing and rail loads.
Observe the return strand and chain entry at the drive. Excessive sag, whipping or tooth climbing indicates a problem, but the cause may be wear, misalignment or insufficient support rather than simply low tension. Unequal take-up positions between strands are especially useful clues to rail or drive timing issues.
After adjustment, run representative carriers through acceleration, stops and the longest queue. Confirm that sprocket engagement remains smooth and that carriers do not skew. Include take-up travel and drive/return layout in a new-system RFQ so adjustment range is considered before installation.