
Product Description
ForgedScraper conveyor chain
P152F51/45/45A/45C/47/45D/45E/45F, P2000F29/29A, P101.6F20, RO6205MF3, MR56, MR80, MR224, MR315, FVR40/63/90/112
Forged chain , trolleys,carriers used on overhead conveyor production line.
Main products are Forge chain and trolley, welded link chain, Standard and non-standard stainless steel and carbon steel roller chain, Leaf chain, standard and non-standard conveyor chain, Scraper conveyor chain, Cranked link chain, double plus chain, double pitch transmission chain, plastic chain, sprockets and Other accessories.
Main products are Forge chain and trolley, welded link chain, Standard and non-standard stainless steel and carbon steel roller chain, Leaf chain, standard and non-standard conveyor chain, Scraper conveyor chain, Cranked link chain, double plus chain, double pitch transmission chain, plastic chain, sprockets and Other accessories.
The products can be combined to find the best possible solution for even the most demanding applications. Special solutions can also be developed for customers’ individual requirements.
Drop Forged Rivetless Chain, Drop Forged Chains, drop forged link,forged scraper chains.
1.Scraper chains P142,P142V,P142H,P200,P102,P250,P260
2.Detachable chain 51,52,55,57,62,74,78
3.Relevant overhead trolley&carriages&spare parts
4.as per your drawings or samples
| Drop forged detachable chains | X348,X458,X678,X698,F100,F160,P80,P100,P200 |
| CatterPilar Chains for | X348,X458,X678,X698 |
| Material: | Alloy |
|---|---|
| Structure: | Combined Chain |
| Surface Treatment: | Polishing |
| Chain Size: | 1/2"*3/32" |
| Feature: | Heat Resistant |
| Process: | Forging |
| Samples: |
US$ 1/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
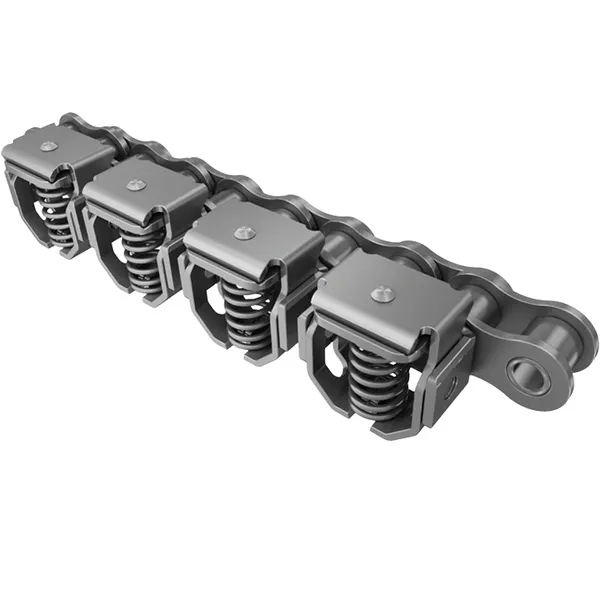
What are the benefits of using a self-lubricating conveyor chain?
Self-lubricating conveyor chains offer several advantages over traditional lubricated chains. Here are some key benefits:
1. Reduced Maintenance: Self-lubricating chains eliminate the need for regular lubrication, reducing the time and effort required for maintenance. This is particularly beneficial in applications where access to the chain is difficult or time-consuming.
2. Cost Savings: By eliminating the need for external lubrication, self-lubricating chains can help reduce lubrication costs over the lifetime of the chain. This includes the cost of lubricants, as well as the labor and equipment required for lubrication maintenance.
3. Clean and Environmentally Friendly: Self-lubricating chains do not require external lubricants, resulting in a cleaner working environment. There is no risk of lubricant spills or contamination of the surrounding area, making them ideal for applications that require strict cleanliness standards, such as food processing or pharmaceutical industries.
4. Extended Chain Life: Self-lubricating chains are designed with built-in lubrication systems that provide a continuous and controlled supply of lubricant to the chain components. This helps reduce friction, wear, and heat generation, resulting in longer chain life and improved performance.
5. Improved Reliability: With consistent and reliable lubrication, self-lubricating chains maintain optimal performance and minimize the risk of chain failure or breakdown. They are less susceptible to premature wear, elongation, and corrosion, ensuring a more reliable and efficient conveyor system.
It’s important to note that the specific benefits of self-lubricating chains may vary depending on the manufacturer and the design of the chain. It’s recommended to consult with the chain manufacturer or an industry expert to understand the suitability and advantages of self-lubricating chains for a particular application.
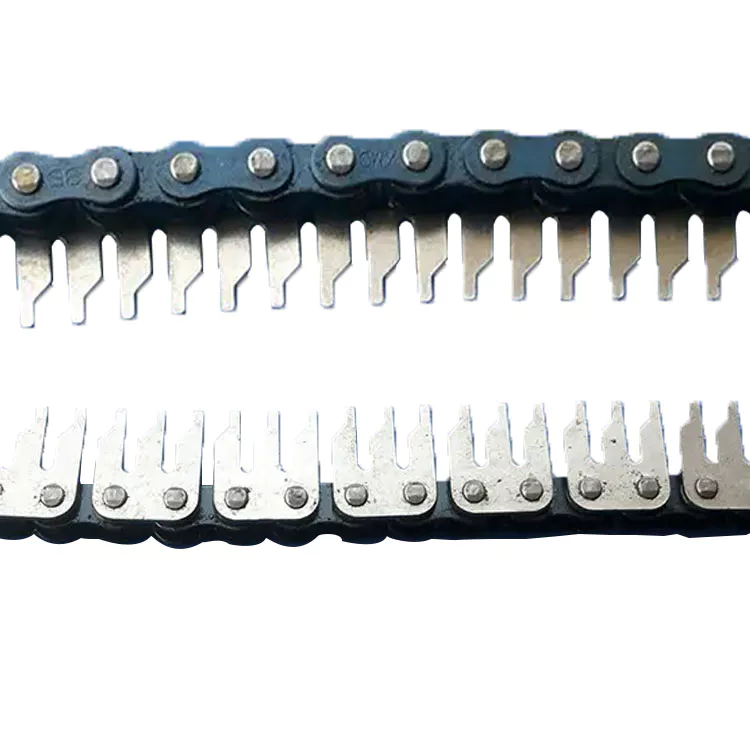
What are the advantages of using a plastic conveyor chain?
Plastic conveyor chains offer several advantages over traditional metal chains. Here are some of the key advantages:
1. Corrosion Resistance: Plastic chains are highly resistant to corrosion, making them ideal for applications in humid or corrosive environments. They do not rust or deteriorate when exposed to moisture or chemicals.
2. Lightweight: Plastic chains are significantly lighter than metal chains, making them easier to handle and install. Their lightweight nature reduces the overall weight of the conveyor system and can result in energy savings during operation.
3. Low Noise Operation: Plastic chains generate less noise compared to metal chains, leading to a quieter working environment. This can be particularly beneficial in industries where noise reduction is important, such as food processing or packaging.
4. Reduced Friction and Wear: Plastic chains have self-lubricating properties, which reduce friction and wear. This results in lower maintenance requirements and longer chain life. The smooth surface of plastic chains also minimizes the risk of product damage during transportation.
5. Flexibility and Modularity: Plastic chains can be easily customized and designed to fit specific conveyor system requirements. They offer flexibility in terms of length, width, and configuration. Additionally, plastic chains are often modular, allowing for easy replacement of damaged or worn-out sections without replacing the entire chain.
6. Cost-Effective: Plastic conveyor chains are generally more cost-effective compared to metal chains. They are often less expensive to manufacture and offer a longer lifespan with minimal maintenance requirements, resulting in lower overall costs.
7. Chemical Resistance: Plastic chains are resistant to a wide range of chemicals, making them suitable for applications where exposure to aggressive substances is a concern. They can withstand contact with oils, acids, alkalis, and various cleaning agents.
Overall, the advantages of using a plastic conveyor chain include corrosion resistance, lightweight design, low noise operation, reduced friction and wear, flexibility, cost-effectiveness, and chemical resistance. These benefits make plastic chains a popular choice in various industries, including food processing, packaging, pharmaceuticals, and logistics.

Can a conveyor chain be used for vertical lifting applications?
Yes, conveyor chains can be used for vertical lifting applications in certain circumstances. However, several factors need to be considered to ensure safe and efficient vertical lifting with a conveyor chain.
1. Chain Type: Not all conveyor chains are suitable for vertical lifting. Specialized chain types, such as bucket elevator chains or vertical reciprocating conveyor chains, are designed specifically for vertical lifting applications.
2. Load Capacity: The conveyor chain selected for vertical lifting must have the appropriate load capacity to handle the weight of the load being lifted. It is crucial to consider both the static and dynamic loads during the lifting operation.
3. Speed and Acceleration: The speed and acceleration of the vertical lifting operation should be within the recommended limits of the conveyor chain to prevent excessive stress and potential failure.
4. Safety Mechanisms: Adequate safety mechanisms, such as overload protection devices or emergency stop systems, should be implemented to ensure the safety of the lifting operation.
5. Maintenance and Inspection: Regular maintenance and inspection of the conveyor chain are essential to identify any wear, fatigue, or damage that could compromise the lifting operation’s safety and reliability.
It is important to consult the manufacturer’s guidelines and recommendations when considering the use of a conveyor chain for vertical lifting applications. They can provide specific information regarding chain selection, installation, maintenance, and safety considerations for vertical lifting operations.


editor by CX 2023-09-15

























