
ISO 606とコンベヤチェーン仕様の背景
実践的なエンジニアリングガイド:ISO 606とコンベヤチェーン仕様の概要。選定、インターフェース、アプリケーションチェック、メンテナンス、およびRFQ入力。
This guide focuses on how ISO 606 applies to short-pitch precision roller and bush chains and associated sprockets, while special conveyor chain families may require additional catalogue-specific geometry. It is written for machine builders, maintenance teams and buyers who need a chain selection that can be checked against drawings and the real conveyor rather than a generic product label.
ISO 606 and Conveyor Chain Specification Context
A pallet conveyor looks simple from a distance, but its reliability depends on several interfaces working at the same time. In a typical project such as a buyer comparing standard chain references with a special free-flow conveyor chain, chain pitch, roller contact, rail alignment, sprocket engagement, carrier stiffness, stops and maintenance access all influence the result. A useful engineering review therefore combines model-level data with the operating sequence of the machine.
Why this issue matters
How iso 606 applies to short-pitch precision roller and bush chains and associated sprockets, while special conveyor chain families may require additional catalogue-specific geometry affects more than catalogue selection. It changes how the workpiece carrier enters a station, how loads pass into guide rails, how the chain approaches the drive and how the system behaves during stopping or accumulation. If one interface is ignored, the symptom may appear somewhere else: a roller can wear because a rail joint is high, a chain can pull sideways because a pallet stop is offset, or a new chain can run badly because the old sprocket is worn.
The practical objective is not to eliminate every variation in the machine. It is to identify the variables that must be controlled, define which dimensions are fixed by the chain source, and leave unsupported items for explicit RFQ confirmation. This is also why claiming every special pallet conveyor chain is fully defined by ISO 606 is a risky shortcut. It replaces measurable machine data with an assumption and can make a correct-looking part fail at installation.
ISO 606:2015 is still the published current edition as of September 2026, while a new edition is under development. ISO 606 covers short-pitch precision roller and bush chains, attachments and associated sprockets. Special free-flow or pallet conveyor chains can include additional geometry that must still be taken from the manufacturer catalogue or exact project drawing.
Four checks to define first
Standard Designation
Include this information in the enquiry so model identification and commercial planning start from reproducible project data.
A/B Series Context
State the measurable condition, installed interface and acceptance check that apply to this part of the conveyor.
Sprocket Interface
Record tooth count or drive geometry, shaft alignment, take-up position and the way the chain enters and leaves the drive.
Catalogue-Specific Special-Chain Data
State the measurable condition, installed interface and acceptance check that apply to this part of the conveyor.
Start with the exact chain geometry
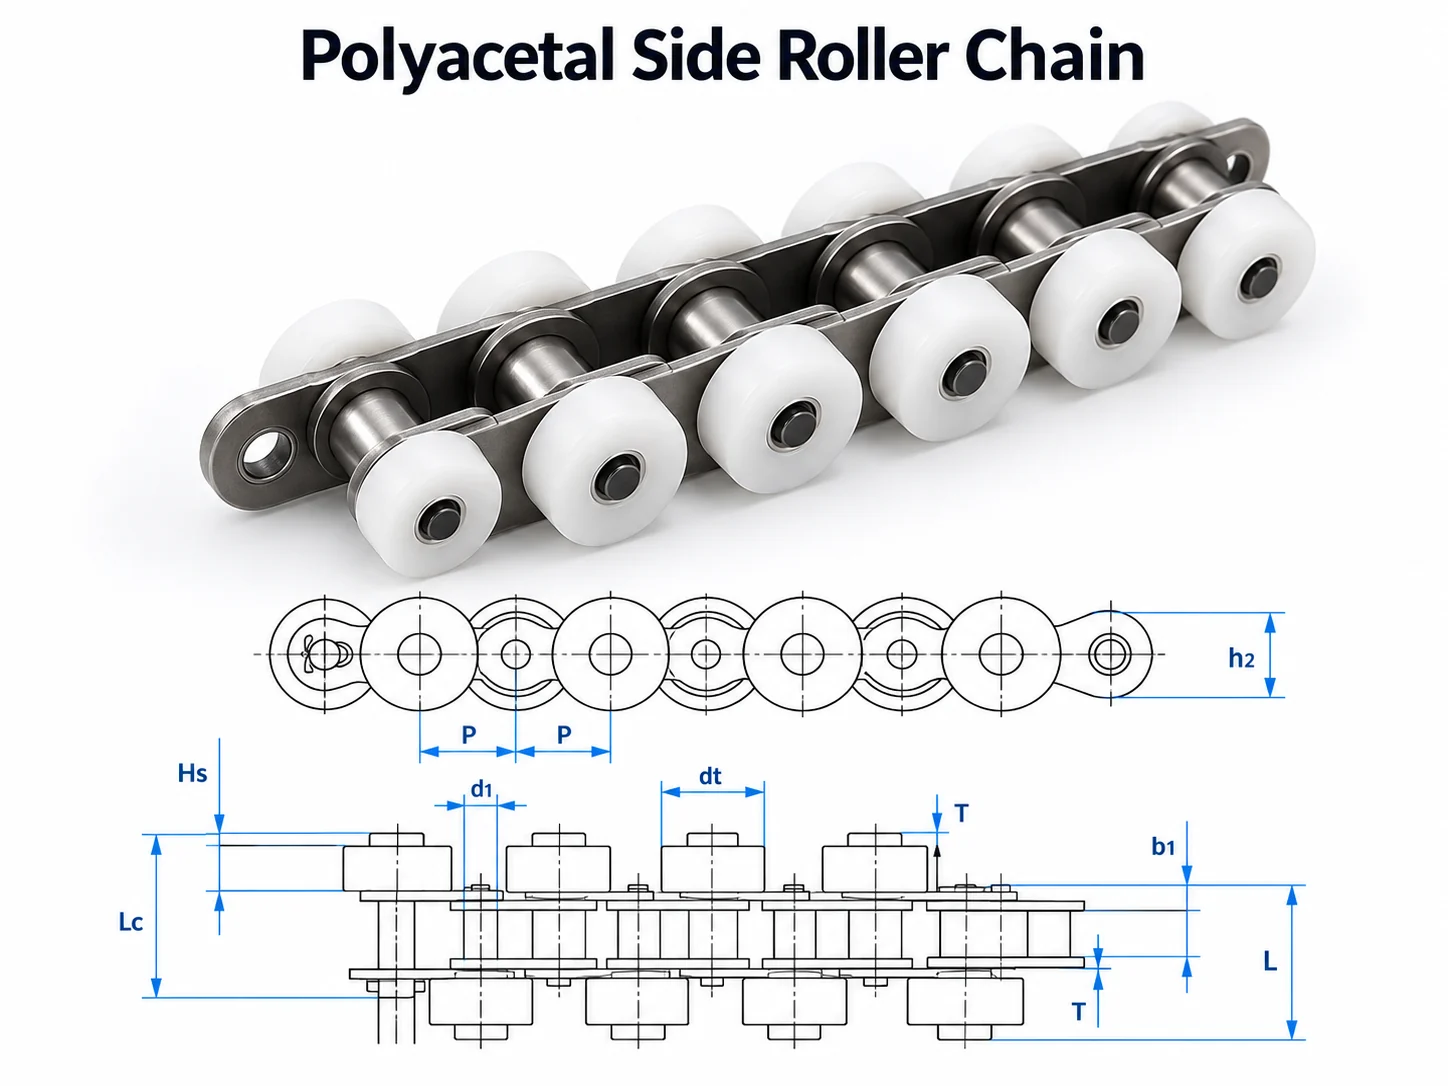
When a model number is available, use the exact model specification and the matching drawing. Compare pitch, roller diameters, inner width, pin diameter and length, plate height and thickness, and any side-roller, large-roller or hollow-pin dimensions that interface with the conveyor. When the code is unknown, measure the installed chain systematically. Measuring pitch across several pins is more reliable than reading a single worn gap, and photographs should show the side profile, roller arrangement, sprocket and rail contact.
Do not use tensile strength as the pallet payload. Catalogue tensile figures are material/component test properties. Conveyor working conditions also involve line length, the number of chain strands, carrier count, acceleration, shock, friction, lubrication, sprocket size, wear state and the required safety factor. The chain can only be verified for a system after those conditions are understood.
Selection workflow
- Standard Designation: compare the required condition with the exact chain drawing or system layout and record any open question for RFQ confirmation.
- A/B Series Context: compare the required condition with the exact chain drawing or system layout and record any open question for RFQ confirmation.
- Sprocket Interface: compare the required condition with the exact chain drawing or system layout and record any open question for RFQ confirmation.
- Catalogue-Specific Special-Chain Data: compare the required condition with the exact chain drawing or system layout and record any open question for RFQ confirmation.
- Carrier and duty: record loaded carrier mass, number of carriers, line speed, starts per hour, accumulation pattern and any incline or vertical transition.
- Drive and return: confirm sprocket data, shaft alignment, take-up range, return support and lubrication access.
- Release condition: list any field that the technical data does not state—such as a special material grade, coating, allowable system load or environmental rating—as an RFQ confirmation item instead of estimating it.
System integration
Once the chain is identified, check how the conveyor transfers load into the rest of the machine. The guide or wear rail should support the intended roller surface and remain continuous through joints. Parallel strands should have the specified center distance and synchronized drive timing. Stops should contact a designed pallet face, not the chain side plate. Cross transfers and lifts need enough support so the carrier does not drop into a gap or land on a pin/plate edge.
For systems that accumulate, separate transport from stopping. The chain may continue moving while the carrier is held, but the stop force, queue length, restart sequence and local friction still need to be checked. For systems that position a workpiece for processing, use dedicated locating features when the required repeatability is tighter than normal conveyor transport can provide.
Commissioning and maintenance
Commission a new or repaired conveyor at low speed first. Jog several complete chain circuits and observe the drive, return, rail transitions, stops and transfers. Listen for sounds that repeat once per chain revolution or once per sprocket rotation because those patterns help isolate a tight joint, roller damage, local rail step or sprocket issue. With rigid workpiece pallets, watch for skewing across parallel strands; even small timing differences can load one side of the carrier.
Maintenance should track trends instead of waiting for a failure. Record elongation or length checks using the approved method, inspect rollers for free rotation and abnormal flats, look for polished side-contact marks that suggest misalignment, inspect sprocket teeth and verify take-up position. Lubrication intervals should reflect the operating environment and the chain manufacturer’s guidance; more lubricant is not automatically better if it attracts abrasive contamination or enters a process area.
RFQ checklist
For a replacement request, send the model code if legible, measured pitch, roller arrangement, chain width, plate height, pin dimensions, a photograph of the side profile and a photograph showing sprocket/rail contact. For a new system, add conveyor length, carrier size and loaded mass, number of strands, strand spacing, speed, starts/stops, buffer length, environmental conditions and destination country. These details make it possible to separate a chain match from a full conveyor-duty calculation.
Use the standard as a dimensional reference, not a complete conveyor design
A chain standard can organize pitch series, terminology and dimensional relationships, but the installed conveyor still has its own rail, sprocket, carrier, stop and environmental interfaces. Separate the standardized chain dimensions from machine-specific requirements when reviewing a replacement.
Record which designation or series applies, then compare the physical chain and sprocket. Special conveyor chains, attachments and application loads may require catalogue- or drawing-specific data beyond the base standard. If a requirement is not stated, confirm it for the project rather than treating the standard name as proof of interchangeability.
Measure the interface
Use several-pitch dimensions, end-view geometry and sprocket/rail details when a replacement must fit an existing machine.
Describe the duty
Include loaded carrier mass, speed, starts, accumulation or indexing behavior and the operating environment.
Test the worst case
Commission with representative carriers and the most demanding queue, stop, transfer or restart condition rather than only no-load travel.
Keep open items explicit
If a material, coating, special tolerance, documentation need or allowable system load is not stated, confirm it in the enquiry.
Frequently asked questions
Can I select a replacement from pitch alone?
For iso 606 and conveyor chain specification context, pitch is only the first filter. Confirm roller geometry, inner width, pins, plates and any side-roller or hollow-pin features against the installed conveyor before treating two chains as interchangeable.
Does a higher tensile value mean I can carry that load on the pallet?
For iso 606 and conveyor chain specification context, do not convert tensile strength directly into pallet payload. Service load depends on strand count, friction, acceleration, stop impact, sprockets, rails and the safety margin used for the machine.
Can a representative family photo prove the exact model?
No. A representative family image can help explain construction, but model identity and dimensions must come from the model-specific technical specification, drawing or confirmed manufacturing data.
What information speeds up a quotation?
For an RFQ related to iso 606 and conveyor chain specification context, send the model code or dimensional sketch, clear photographs, conveyor layout, loaded carrier information, quantity and delivery country so the review starts from reproducible machine data.
Key engineering variables for ISO 606 and Conveyor Chain Specification Context
The decision should be tied to measurable machine inputs and the exact chain drawing rather than a generic family label. Record the operating case in one line: what the conveyor carries, how fast it moves, where it stops and what condition triggered the review. Capture dimensions and observations another engineer can reproduce.
| Input | What to record | Why it matters |
|---|---|---|
| Carrier/load | Loaded mass, center of gravity, underside contact and carrier count | Support, friction and stop behavior |
| Motion | Speed, starts, stops, accumulation and indexing | Dynamic demand and process timing |
| Chain path | Pitch, rollers, strand spacing and rails | Mechanical fit and tracking |
| ドライブ | Sprocket teeth, alignment, take-up and drive position | Engagement and tension distribution |
| 環境 | Temperature, dust, moisture, cleaning and lubrication limits | Material and maintenance choices |
Related product and selection resources
Use the pallet conveyor chain catalogue to compare families and the engineering selection workflow when machine data is incomplete.
What to include with an enquiry about ISO 606 and Conveyor Chain Specification Context
Identify the installed or proposed chain family, quantity, application, carrier/load, key dimensions and the operating condition the new part must solve. Attach photographs or drawings when the existing code is uncertain and keep open material, documentation or delivery requirements visible.
Use standards as a dimensional reference, then verify the conveyor interface
A chain standard helps define terminology, pitch series and dimensional relationships, but it does not describe the complete pallet conveyor. Rail section, carrier underside, sprocket condition, strand spacing, stop layout and environment still belong to the machine design. When reviewing a replacement, separate what is controlled by the chain specification from what is unique to the installed conveyor. Record the chain designation, measured pitch, roller or bush dimensions and plate geometry, then compare the installed sprocket and rail. If the machine drawing contains tolerances or special attachments, those requirements take priority for the actual project. This approach avoids treating a standards reference as proof that two complete conveyor assemblies are interchangeable.
Reference
Identify the standard or dimensional series actually applicable to the chain being reviewed.
Measure
Confirm the installed chain and sprocket rather than assuming the standard defines the full conveyor.
Separate
Keep machine-specific rail, pallet, stop, attachment and environmental requirements in the project drawing.
Document
Record which dimensions were verified and which items still require supplier confirmation.
Turn the conveyor description into reproducible project data
Use ISO 606 and Conveyor Chain Specification Context as a prompt to record the machine rather than relying on family names. Start with the chain model if it is known; otherwise measure several pitches and the roller, pin, plate or attachment geometry. Add an end photograph on the rail, sprocket tooth count and bore, strand spacing and carrier underside. Then document loaded carrier mass, travel speed, starts, maximum accumulation, transfers and the environment.
For a replacement, include the old marking and the reason for replacement, especially if unusual wear or failure is involved. For new equipment, add the process sequence and drive/take-up layout. If a material, coating, allowable load, tolerance or documentation requirement is not shown in the exact technical data, state it as a requirement to confirm. That separates known geometry from application questions and makes the enquiry useful to both engineering and purchasing.
Identify
Model marking, photographs and several-pitch measurement.
Measure
Roller/pin/plate geometry, sprocket, rail and strand centers.
Describe duty
Carrier/load, speed, starts, queue, transfers and environment.
State open requirements
Material, documentation, special length, tolerance and delivery needs.
Use the standard designation as a reference point, then verify the installed interfaces
Record the chain designation or pitch series and compare the physical chain with the applicable dimensional data. Then measure the machine-specific features the standard cannot define for the installation: side-roller offset, custom attachments, rail section, strand spacing, carrier underside, sprocket bore/hub and stop/transfer geometry.
For replacement work, inspect the existing sprocket and rail as carefully as the chain. A standardized pitch does not make a worn sprocket or incompatible attachment disappear. Where a special conveyor family has catalogue-specific dimensions, use the exact family/model drawing in addition to general standard terminology.
In procurement, avoid using the standard name as proof of material grade, allowable system load, coating or full interchangeability unless those requirements are explicitly stated. Put any special documentation or compliance need into the enquiry so it can be confirmed for the proposed product and order.

























