
Descripción del Producto
| The 880 series has a wide range of applications for conveying lightweight items in curves e.g. plastic bottles, cans, cartons etc. This space-saving chain is often used with small diameter turn discs with ball bearings. Plate mat.:POM/PP; Pin mat.:stainless steel Max.speed: 80m/min lubrication; 50m/min dry;Max.length:15m; Working load:2680N Color:white/brown; Packing unit:10ft(80links) |
| APPLICATIONS: |
| China CZPT Machinery Co.,Ltd is a special supplier of conveyor system components,including plastic and stainless steel flat top chains, Modular belts, other spare parts, such as UHMWPE wearstrips, side guards, chains guide, bipods, tripods, brackets, clampls.ect. With our years of experence, quality products, excellent services we work with world wide clients from America, Europe, Africa, many counrties of Asia. We keep very good business relation with them, and get trusted from them. Our products application: Packaging and conveying industry |
| Material: | Plástico |
|---|---|
| Estructura: | Cadena superior |
| Tratamiento de superficie: | Low Friction |
| Tamaño de la cadena: | Pitch 38.1mm |
| Pin: | SS304 |
| Condition: | 100% Brand New |
| Muestras: |
US$ 30/Meter
1 metro (pedido mínimo) | |
|---|
| Customization: |
Available
| Customized Request |
|---|

Can a conveyor chain be used in pharmaceutical manufacturing?
Yes, conveyor chains can be used in pharmaceutical manufacturing for various applications. Conveyor systems play a crucial role in the efficient and safe transportation of pharmaceutical products throughout the manufacturing process. Here are some key considerations when using conveyor chains in pharmaceutical manufacturing:
1. Material Selection:
– Choose conveyor chains made from materials that are suitable for pharmaceutical applications, such as stainless steel or FDA-approved plastic. These materials offer corrosion resistance, cleanliness, and compliance with industry regulations.
2. Cleanliness and Sanitation:
– Ensure that the conveyor chain design allows for easy cleaning and sanitation. Smooth surfaces, minimal crevices, and access for cleaning equipment are important to maintain a hygienic environment.
3. Contamination Control:
– Implement measures to prevent contamination of pharmaceutical products. This includes using chain lubricants that are safe for pharmaceutical applications and implementing proper handling and storage procedures.
4. Product Protection:
– Choose conveyor chain systems that minimize product damage or degradation. This can include utilizing gentle product handling features such as low-friction surfaces, adjustable speed controls, and proper product spacing.
5. Regulatory Compliance:
– Ensure that the conveyor chain system complies with pharmaceutical industry regulations and guidelines, such as Good Manufacturing Practices (GMP) and the requirements of regulatory bodies like the FDA.
6. Integration with Equipment:
– Consider the integration of conveyor chains with other equipment in the pharmaceutical manufacturing process, such as labeling machines, filling machines, and packaging equipment. The conveyor system should provide seamless operation and synchronization with these machines.
By carefully selecting and designing conveyor chains specifically for pharmaceutical manufacturing, it is possible to meet the stringent requirements of the industry in terms of cleanliness, product integrity, and regulatory compliance.
How does a conveyor chain handle different types of materials?
A conveyor chain is designed to handle a wide variety of materials in diverse industrial applications. It is capable of efficiently transporting different types of materials, including:
1. Bulk Materials: Conveyor chains are commonly used to handle bulk materials such as grains, coal, ores, aggregates, and powders. The design of the chain, including the spacing and shape of the links, helps prevent material spillage and ensures smooth and consistent flow.
2. Packaged Goods: Conveyor chains are also used for conveying packaged goods such as boxes, cartons, crates, and pallets. They provide a stable and reliable method of transporting these items along the production line, reducing manual handling and increasing productivity.
3. Small Parts: Conveyor chains with specialized attachments or small-pitch configurations are suitable for handling small parts or components. These chains ensure precise positioning and gentle transport of delicate or intricate items.
4. Heavy-Duty Loads: Industrial conveyor chains are capable of handling heavy-duty loads, such as automotive parts, machinery components, and large equipment. They are engineered to withstand the weight and stress of these objects, providing reliable and efficient material handling in demanding environments.
5. Food and Beverage Products: Conveyor chains used in the food and beverage industry are designed to meet strict hygiene and safety standards. They are constructed from materials that are resistant to corrosion, easy to clean, and compliant with food-grade regulations. These chains ensure the safe and contamination-free handling of food products.
6. Hazardous Materials: Conveyor chains can be used to safely transport hazardous materials, such as chemicals or waste products. Specialized chains with additional safety features, such as sealed housings or containment systems, are utilized to minimize the risk of spills or leaks.
Conveyor chains can be customized with different chain configurations, attachments, and accessories to accommodate specific material characteristics and handling requirements. The selection of the appropriate chain type, material, and design parameters ensures optimal performance and efficient material handling for a wide range of materials.
What are the different types of conveyor chains?
There are several types of conveyor chains available, each designed to meet specific application requirements. Here are some common types of conveyor chains:
- Roller chains: Roller chains are the most commonly used type of conveyor chain. They consist of a series of cylindrical rollers connected by side plates. Roller chains provide smooth and efficient movement and are suitable for medium to heavy-duty applications.
- Double pitch chains: Double pitch chains have larger pitch (distance between the centers of adjacent pins) compared to standard roller chains. They are often used in applications that require slower speeds and lighter loads.
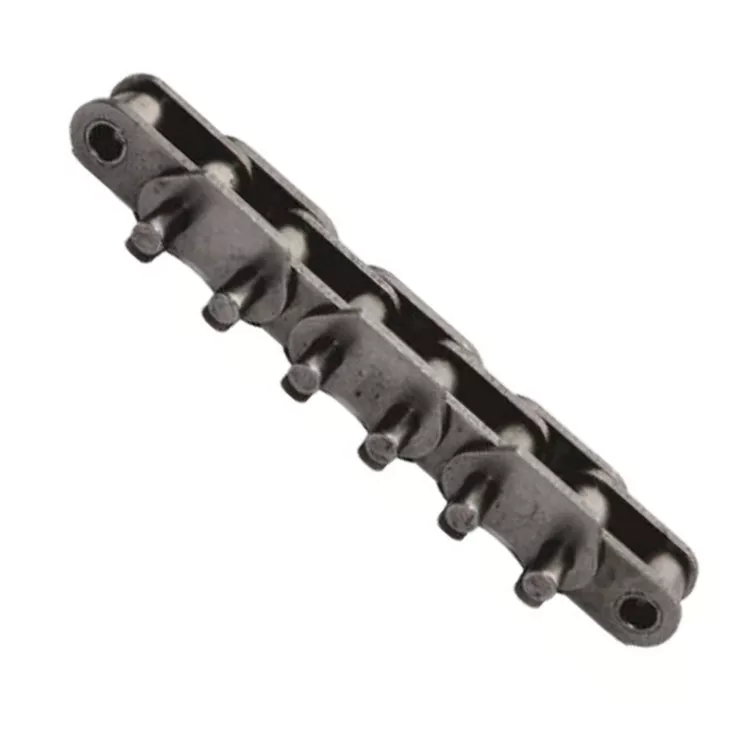
- Hollow pin chains: Hollow pin chains have hollow pins that allow for easy attachment of various accessories or attachments. They are commonly used in conveying applications that require customization or where attachments need to be mounted.
- Apron or slat chains: Apron or slat chains consist of plates or slats that are connected by hinges. They are used in heavy-duty applications where the chain needs to support and carry large loads or withstand harsh environments.
- Plastic chains: Plastic chains are made of durable and lightweight materials such as acetal or polyethylene. They offer benefits such as corrosion resistance, low noise levels, and the ability to work in wet or washdown environments. Plastic chains are commonly used in food processing, packaging, and pharmaceutical industries.
These are just a few examples of conveyor chain types, and there are many other variations available depending on specific application requirements. The selection of the appropriate conveyor chain type depends on factors such as load capacity, speed, environment, and desired functionality.


editor by CX 2023-08-15

























